Author: Brian Ribeiro

  • How SiC and Advanced IGBT Technologies Improve UPS Efficiency

    How SiC and Advanced IGBT Technologies Improve UPS Efficiency

    An uninterruptible power supply must do two things exceptionally well: protect the load and minimize the energy consumed while providing that protection.

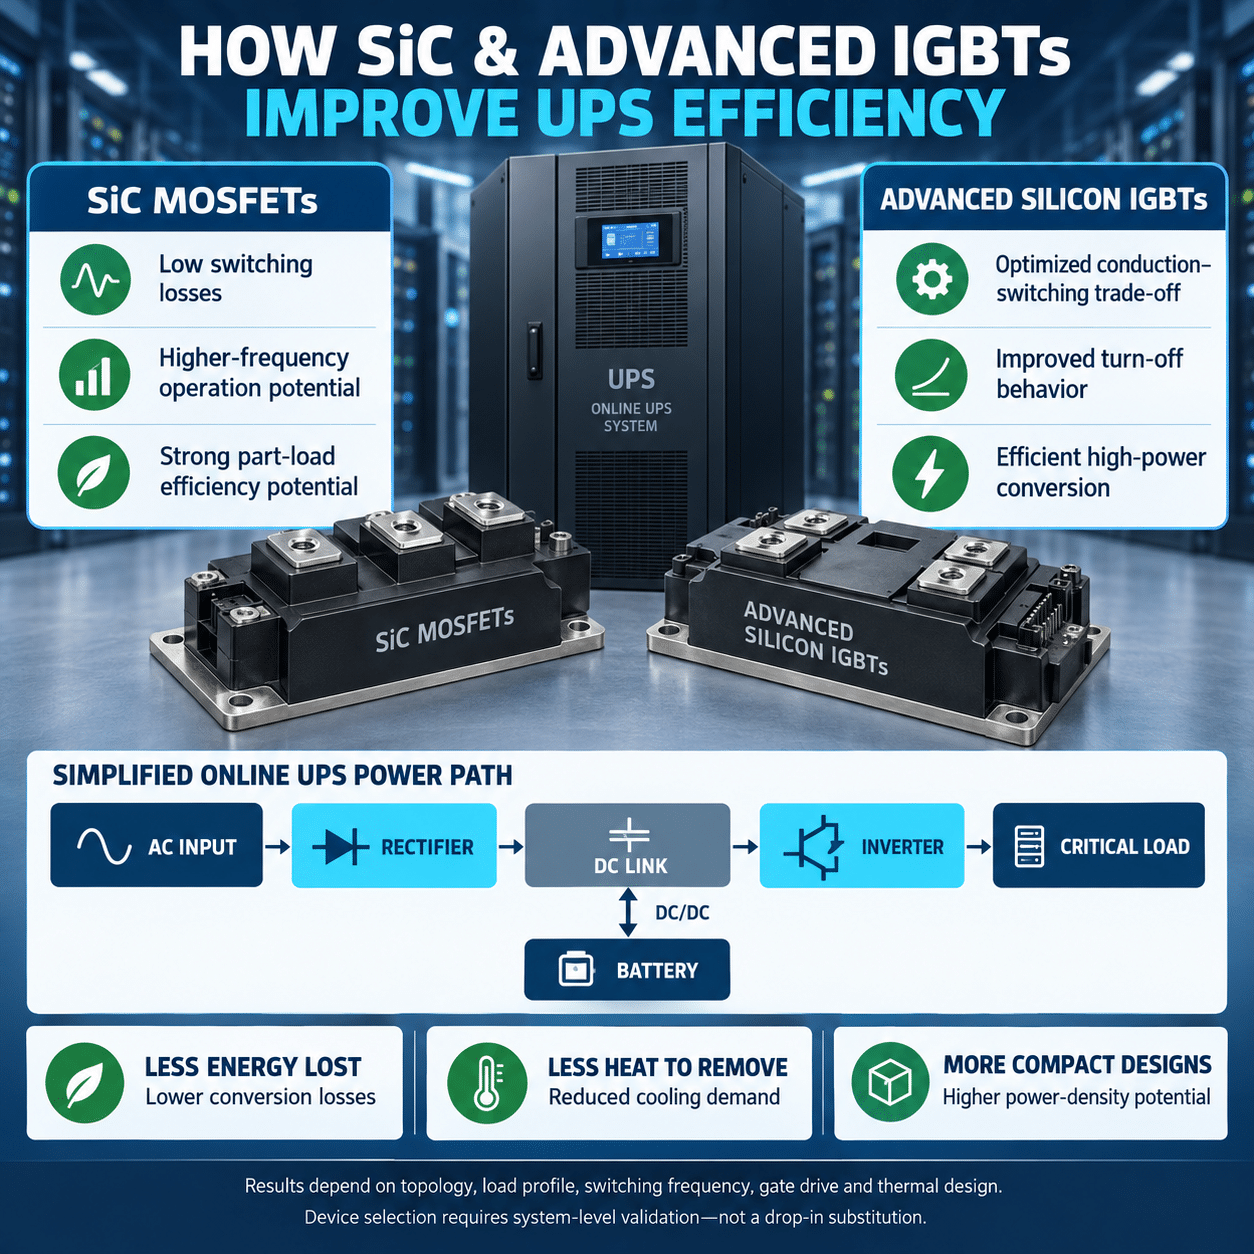
    In a double-conversion UPS, incoming AC power is converted to DC and then reconstructed as regulated AC. This architecture isolates critical equipment from many utility disturbances, but every conversion stage produces some loss. In a large data center or industrial facility, even a small improvement in UPS efficiency can reduce electricity use, cooling demand and operating cost.

    Silicon carbide devices and advanced insulated-gate bipolar transistors are helping UPS manufacturers reduce those losses without giving up the power quality and availability required by critical loads.

    Where does UPS power loss come from?

    A conventional online UPS contains several power-handling components:

    • Input rectifier or converter
    • DC link
    • Battery interface
    • Output inverter
    • Static bypass
    • Magnetic components
    • Filters
    • Cooling fans
    • Control and auxiliary power supplies

    Power is lost in semiconductor conduction, switching transitions, inductors, transformers, capacitors, conductors and cooling systems.

    The semiconductor devices in the rectifier and inverter are particularly important because they must carry the UPS load continuously while switching thousands of times per second.

    Total semiconductor loss can be divided into two broad categories.

    Conduction loss

    Conduction loss occurs while a semiconductor is carrying current. It depends on the device’s on-state voltage or resistance, load current, duty cycle and junction temperature.

    A device with lower on-state voltage reduces the power converted to heat during each conduction interval.

    Switching loss

    Switching loss occurs while a device changes between its off and on states. Voltage and current overlap briefly during each transition, producing an energy loss.

    Total switching loss increases with:

    • Switching frequency
    • Bus voltage
    • Load current
    • Turn-on and turn-off energy
    • Diode reverse recovery
    • Parasitic inductance
    • Gate-drive behavior

    Reducing either form of loss can improve UPS efficiency, but semiconductor design involves tradeoffs. A device optimized for very low conduction loss may not provide the lowest switching loss, and vice versa. The best device depends on the UPS topology, voltage, switching frequency and load profile.

    Why UPS efficiency matters

    UPS losses become heat inside the electrical room. That creates two operating costs:

    1. The electricity lost in the UPS
    2. The additional electricity needed to remove the heat

    Consider a UPS delivering a constant 1 MW load. At 96% efficiency, its approximate input is 1.042 MW and its internal loss is about 41.7 kW. At 97.5% efficiency, the input is approximately 1.026 MW and the loss falls to about 25.6 kW.

    That 1.5-percentage-point improvement reduces UPS loss by roughly 16 kW at this operating point—before accounting for the associated reduction in cooling energy.

    Actual savings depend on the load profile, operating mode, redundancy configuration, electricity rate and cooling-system efficiency. This is why an efficiency curve is more useful than a single peak-efficiency number.

    The role of IGBTs in modern UPS systems

    The insulated-gate bipolar transistor, or IGBT, combines a voltage-controlled gate with strong high-voltage and high-current capability. IGBTs have been widely adopted in medium- and high-capacity UPS converters and inverters.

    Fuji Electric’s UPS history illustrates the effect of this transition. Compared with earlier thyristor-based systems, its adoption of IGBTs for both the converter and inverter increased conversion efficiency and substantially reduced equipment size.

    IGBT technology has continued to advance. Improvements include:

    • Thinner semiconductor structures
    • Optimized trench-gate designs
    • Improved field-stop layers
    • Lower on-state voltage
    • Reduced switching energy
    • Improved diode performance
    • Higher allowable junction temperature
    • Lower-inductance packaging
    • Reverse-conducting and reverse-blocking functions

    These developments allow UPS designers to reduce losses without simply increasing semiconductor die area.

    How advanced IGBTs improve efficiency

    Better conduction and switching tradeoffs

    IGBT designers generally seek to reduce on-state voltage without creating an unacceptable increase in switching loss. Newer chip structures provide greater control over the carrier distribution inside the device, improving this tradeoff.

    Fuji Electric’s 7th-generation X-Series IGBT technology uses thinner and optimized chip structures to reduce inverter loss. In one published comparison involving 1,200 V, 75 A devices operating at 8 kHz, the X-Series reduced inverter loss by 10% relative to the preceding V-Series under the stated test conditions.

    This is a device and test-condition comparison, not a guarantee that every complete UPS will gain 10% efficiency. System performance also depends on topology, controls, magnetics, cooling and the operating point.

    Improved freewheeling diode performance

    The switching device does not operate alone. In many converter topologies, current commutates between the IGBT and a freewheeling diode.

    Diode forward-voltage and reverse-recovery behavior affect:

    • Conduction loss
    • Turn-on loss
    • Voltage overshoot
    • Electromagnetic interference
    • Device stress

    An improved diode can therefore increase the benefit obtained from an advanced IGBT.

    Reverse-conducting IGBTs

    A reverse-conducting IGBT integrates IGBT and freewheeling-diode functions into one chip. This can increase power density and simplify chip placement inside the module.

    Fuji Electric has developed X-Series RC-IGBT modules that combine 7th-generation IGBT and diode functionality, supporting higher power density and improved performance in applicable industrial power converters.

    Reverse-blocking IGBTs

    Most conventional IGBTs are designed primarily to block voltage in one direction. A reverse-blocking IGBT, or RB-IGBT, is designed to block voltage in both directions.

    In suitable three-level converter circuits, an RB-IGBT can reduce the number of series-connected semiconductor elements in a current path. Fewer conducting junctions can mean lower conduction loss.

    Fuji Electric has applied proprietary RB-IGBT technology in advanced T-type neutral-point-clamped conversion circuits used in high-efficiency UPS systems.

    What makes silicon carbide different?

    Conventional power semiconductors are made from silicon. Silicon carbide, or SiC, is a wide-bandgap semiconductor material with physical properties that support:

    • Higher electric-field strength
    • Higher-voltage operation with thinner active regions
    • Faster switching
    • Lower switching energy
    • Lower reverse-recovery loss
    • Higher-temperature capability
    • Higher switching frequency

    The two SiC devices most relevant to UPS designs are SiC Schottky barrier diodes and SiC MOSFETs.

    SiC Schottky barrier diodes

    A SiC Schottky barrier diode, or SiC-SBD, has very little reverse-recovery charge compared with a conventional silicon bipolar diode.

    When a silicon diode changes from conducting to blocking, stored charge must be removed. The resulting reverse-recovery current increases loss in both the diode and the switching transistor. It can also contribute to current spikes, voltage overshoot and electromagnetic noise.

    Replacing the diode with a suitable SiC-SBD can:

    • Reduce diode recovery loss
    • Reduce IGBT turn-on loss
    • Lower current overshoot
    • Reduce thermal stress
    • Support higher switching frequency
    • Simplify management of switching transients

    A combination of silicon IGBTs and SiC diodes is often described as a hybrid SiC solution. It captures an important portion of SiC’s efficiency benefit while retaining the established high-current capability and cost structure of IGBTs.

    Fuji Electric has developed 1,200 V SiC-SBD products for systems including data-center and telecommunications power supplies, targeting lower forward loss and improved surge-current capability.

    SiC MOSFETs

    A SiC MOSFET replaces the silicon IGBT as the actively controlled switching device. It can switch more rapidly and with lower switching loss, particularly at light and medium loads where an IGBT’s characteristic voltage drop can represent a significant penalty.

    Potential UPS benefits include:

    • Lower turn-on and turn-off loss
    • Reduced part-load loss
    • Higher switching frequency
    • Smaller magnetic components
    • Smaller filters
    • Reduced heat-sink requirements
    • Higher power density

    SiC MOSFETs also conduct reverse current through their channel when controlled appropriately. Their behavior differs from both silicon MOSFETs and IGBTs, so the gate drive, dead time and protection system must be designed specifically for the device.

    Fuji Electric notes that faster switching can reduce power loss and that higher switching frequencies can contribute to smaller power-conversion equipment.

    Why faster switching can make a UPS smaller

    Higher switching frequency moves the converter’s switching ripple to a higher frequency. This can reduce the inductance and capacitance needed to filter it, allowing smaller reactors and filter components.

    A smaller magnetic component can provide several system-level benefits:

    • Reduced copper loss
    • Reduced core material
    • Lower weight
    • Smaller enclosure
    • Shorter power paths
    • Greater power density

    However, frequency cannot be increased without limit. Higher frequency increases the number of switching events per second and may increase losses in semiconductors, magnetic cores, capacitors and conductors.

    SiC expands the useful design range by reducing the energy lost in each switching transition. The optimum switching frequency remains a system-level decision.

    Three-level topologies reduce semiconductor stress

    A traditional two-level inverter switches each phase output between the positive and negative DC rails. A three-level topology adds an intermediate voltage state.

    Depending on the circuit, this can:

    • Reduce the voltage switched by an individual device
    • Lower switching loss
    • Reduce output-voltage steps
    • Reduce filter requirements
    • Improve waveform quality
    • Support a higher DC bus with available device ratings

    The semiconductor benefit depends on the specific topology and current path. A poorly optimized three-level circuit can add conduction devices and control complexity. Advanced devices such as RB-IGBTs can help reduce that penalty.

    Fuji Electric’s advanced T-type neutral-point-clamped architecture combines RB-IGBT and SiC technology to reduce conversion loss in applicable UPS systems. Its 7400WX-T3U achieved a published efficiency of 97.4% and at least 96% efficiency at a 25% load factor under the product’s stated conditions.

    Part-load efficiency is essential

    UPS systems rarely operate at their nameplate rating continuously.

    Common reasons include:

    • N+1 or 2N redundancy
    • Future capacity reserved for growth
    • Variable IT or production loads
    • Conservative initial sizing
    • Modular systems operating with spare capacity

    A system designed for redundancy may place each UPS module at 25%, 40% or 50% load during normal operation. Peak efficiency at 100% load may therefore say little about annual energy consumption.

    SiC and advanced IGBT technologies can improve part-load efficiency by reducing switching, conduction and auxiliary losses. System controls can add another layer of improvement by operating the appropriate number of modules near a more efficient load point.

    Fuji Electric’s 7400WX-T3U includes an optimum-load operating mode that adjusts the number or loading of operating UPS units to improve overall system efficiency.

    When evaluating a UPS, request efficiency at:

    • 10% load, if available
    • 25% load
    • 50% load
    • 75% load
    • 100% load

    Apply those values to the facility’s expected annual load distribution.

    Reduced loss lowers cooling requirements

    Every kilowatt not lost in the UPS is a kilowatt that does not have to be removed as heat.

    Lower semiconductor loss can reduce:

    • Heat-sink size
    • Cooling airflow
    • Fan power
    • Electrical-room cooling demand
    • Local hot spots
    • Component temperature
    • Acoustic noise

    Lower temperature can also support reliability because many power-electronic component aging mechanisms accelerate as temperature increases.

    This benefit is not automatic. Higher-temperature-capable SiC devices should not be used as a reason to expose capacitors, fans, control boards and batteries to excessive heat. The entire UPS contains components with different thermal limits.

    The better design objective is often to use the semiconductor’s lower loss and temperature capability to create thermal margin—not simply to operate every component hotter.

    Higher power density can reduce facility footprint

    When lower semiconductor loss is combined with smaller magnetics and reduced cooling requirements, a UPS can deliver more power from a smaller footprint.

    This is valuable in:

    • Data centers
    • Semiconductor plants
    • Hospitals
    • Financial facilities
    • Telecommunications sites
    • Industrial control rooms

    Floor space carries a significant opportunity cost in these facilities. A more compact UPS can leave additional space for production equipment, IT racks, batteries or future capacity.

    Fuji Electric has demonstrated a SiC-based research power unit with 81 kW/L power density and 99.5% efficiency at a 37 kW rated output under the prototype’s test conditions. [6] Although this is not a complete UPS specification, it illustrates how low-loss SiC devices can support compact power-conversion hardware.

    Efficiency mode and semiconductor efficiency are different

    Many UPS products offer an economy, high-efficiency or bypass-based operating mode. Under acceptable utility conditions, such a mode supplies the load through a bypass path rather than continuously processing all power through the rectifier and inverter.

    This can produce efficiency higher than normal double-conversion operation. For example, Fuji Electric’s UPS7500WX lists 98.5% efficiency in its HE mode.

    It is important to distinguish:

    • Efficiency gained from lower-loss semiconductors in the active conversion path
    • Efficiency gained by bypassing some or all of that conversion path

    The operating modes provide different levels of power conditioning and may have different transfer behavior. The appropriate mode depends on:

    • Load sensitivity
    • Utility power quality
    • Transfer-time tolerance
    • Harmonic and power-factor requirements
    • Facility risk policy
    • Applicable standards

    Semiconductor improvements increase the efficiency of online operation, helping reduce the energy penalty when the application requires continuous power conversion.

    Efficiency improvements can support reliability

    Lower internal loss may reduce thermal stress on:

    • Power semiconductor junctions
    • DC-link capacitors
    • Magnetic components
    • Busbars
    • Cooling fans
    • Nearby control electronics

    Reduced fan demand may also extend fan life or allow redundant cooling arrangements to operate with greater margin.

    However, efficiency and reliability must be validated together. Faster switching can create:

    • Higher (dv/dt)
    • Higher (di/dt)
    • Voltage overshoot
    • Common-mode current
    • Electromagnetic interference
    • Insulation stress
    • More demanding gate-drive requirements

    Successful SiC application depends on low-inductance packaging, compact busbars, suitable gate drivers, effective protection and careful EMC design. A fast semiconductor installed in a layout developed for slower devices may not deliver the expected reliability or efficiency.

    Packaging is part of the efficiency equation

    A semiconductor chip cannot perform independently of its package.

    Package features affect:

    • Electrical resistance
    • Parasitic inductance
    • Switching overshoot
    • Heat transfer
    • Current sharing
    • Maximum junction temperature
    • Power-cycling capability

    Lower-inductance packages allow faster switching with less voltage overshoot. Improved insulating substrates and thermal interfaces move heat away from the semiconductor more effectively.

    Fuji Electric’s 7th-generation X-Series power modules combine optimized chips with lower-inductance packaging and improved heat dissipation.

    This coordinated chip-and-package approach is essential because reducing device switching loss is of limited value if parasitic inductance forces the designer to slow the device substantially.

    Choosing between SiC and advanced IGBT solutions

    SiC is not automatically the most economical option for every UPS.

    Advanced IGBTs may remain attractive when:

    • Power levels are high
    • Switching frequency is moderate
    • Conduction loss dominates
    • Cost sensitivity is significant
    • Proven silicon platforms meet the efficiency target
    • Existing manufacturing and service infrastructure is important

    Hybrid SiC solutions may be effective when:

    • Diode reverse recovery is a major loss mechanism
    • Improved switching performance is needed
    • A full SiC design is not required
    • The designer wants to balance performance and cost

    All-SiC solutions may be attractive when:

    • Very low switching loss is important
    • Part-load efficiency is a priority
    • High switching frequency enables smaller magnetics
    • Power density is valuable
    • Cooling capacity or footprint is constrained

    The comparison should be made at the system level. Semiconductor cost should be weighed against savings in magnetics, heat sinks, fans, enclosure volume, cooling infrastructure and lifetime electricity use.

    How to compare high-efficiency UPS systems

    When evaluating a UPS that uses SiC or advanced IGBT technology, ask for:

    1. Efficiency in normal online mode
    2. Efficiency at 25%, 50%, 75% and 100% load
    3. Efficiency in optional economy or high-efficiency modes
    4. Whether auxiliary and fan power are included
    5. Test voltage, power factor and environmental conditions
    6. Heat rejection at representative loads
    7. Input power factor and harmonic performance
    8. Output waveform performance
    9. Overload and short-circuit capability
    10. Semiconductor topology
    11. Redundancy and module-loading strategy
    12. Transfer behavior between operating modes
    13. Cooling-system redundancy
    14. Expected capacitor and fan service life
    15. Applicable efficiency-test standards

    Avoid comparing values measured under different modes or test conditions. A bypass-mode efficiency from one product should not be compared directly with the online double-conversion efficiency of another.

    Calculate annual loss—not just nominal efficiency

    The most useful metric is the annual energy lost under the expected operating profile.

    For each load interval:

    [
    P_{\text{loss}} = P_{\text{out}}\left(\frac{1}{\eta}-1\right)
    ]

    Annual loss energy can then be estimated by multiplying the loss at each operating point by the number of hours spent there.

    Include:

    • Normal load variation
    • Redundancy configuration
    • Planned future growth
    • Battery charging
    • Economy-mode operating hours
    • Cooling energy
    • Module staging
    • Maintenance bypass periods

    This lifecycle analysis may show that a product with a small peak-efficiency advantage offers less annual benefit than one with a flatter part-load curve.

    Power semiconductors and UPS design are evolving together

    The efficiency of a UPS is not determined by one device alone. It results from the interaction of semiconductor technology, circuit topology, gate control, packaging, magnetics, cooling and system operation.

    Advanced IGBTs continue to improve the balance between conduction loss, switching loss, power density and cost. SiC-SBDs reduce reverse-recovery loss, while SiC MOSFETs enable faster switching and smaller passive components. Three-level circuits and intelligent module controls turn those device improvements into system-level savings.

    Fuji Electric develops both UPS systems and the power semiconductors used in power-conversion equipment. Its portfolio includes advanced IGBT, hybrid SiC and SiC technologies intended for high-efficiency converters and uninterruptible power supplies. 

    By evaluating performance across the actual load profile—and separating online conversion efficiency from bypass-mode efficiency—facility designers can choose a UPS that protects critical loads while reducing energy use, cooling demand and total operating cost.

  • How to Troubleshoot and Prevent Nuisance Tripping in Earth Leakage Devices

    How to Troubleshoot and Prevent Nuisance Tripping in Earth Leakage Devices

    An earth leakage device that trips repeatedly is easy to dismiss as overly sensitive. In reality, the trip may be warning of deteriorated insulation, moisture, incorrect wiring or a developing equipment fault. It may also be responding correctly to the combined leakage current produced by filters, long cables, variable frequency drives and other electronic loads.

    The challenge is to distinguish a genuine safety problem from an installation or coordination problem, without defeating the protection the device was installed to provide.

    This article presents a systematic approach to troubleshooting and preventing unwanted trips in earth leakage circuit breakers and protective relays.

    Safety note: Earth leakage troubleshooting should be performed only by qualified electrical personnel using appropriate procedures and test equipment. Do not bypass a protective device, disconnect protective grounding or increase its trip threshold simply to keep equipment running.

    What does an earth leakage device detect?

    Under normal conditions, the current flowing out through the energized conductors should return through the circuit’s designated return conductors. An earth leakage device measures the vector sum of those currents.

    If some current returns through protective earth, equipment frames, building steel, piping or another unintended path, an imbalance appears. When that residual current exceeds the device’s operating threshold for the required time, the device trips or issues an alarm.

    Depending on the region and application, similar equipment may be described as:

    • An earth leakage circuit breaker, or ELCB
    • A residual-current device, or RCD
    • A residual-current circuit breaker
    • A ground-fault circuit interrupter
    • An earth leakage protective relay
    • A ground-fault protective device

    These terms are not always interchangeable. Product functions, trip levels and applicable standards vary. Always identify the exact device and the protection it is intended to provide.

    Fuji Electric offers molded-case earth leakage circuit breakers as well as earth leakage protective relays. A protective relay detects leakage through a zero-phase current transformer and provides a contact output for an alarm or external tripping circuit.

    “Nuisance” tripping may be a real warning

    A trip is unwanted from an operational perspective, but that does not mean it is false. Common causes include:

    • Damaged cable insulation
    • Moisture in motors, junction boxes or heating equipment
    • Contamination on terminals or circuit boards
    • Insulation deterioration caused by age or heat
    • A neutral-to-earth connection downstream of the protective device
    • Incorrectly shared neutrals
    • Wiring errors through a zero-phase current transformer
    • Accumulated leakage from several electronic loads
    • Electromagnetic compatibility filters
    • Long shielded motor cables
    • Variable frequency drive switching
    • Transient overvoltages
    • Simultaneous energization of multiple devices
    • An unsuitable earth leakage device
    • A damaged or incorrectly installed protective device

    Treat every unexplained trip as a condition requiring investigation. Repeatedly resetting the device without finding the cause can expose personnel and equipment to risk.

    Step 1: Determine which protection operated

    Many circuit breakers provide more than one protective function. A molded-case earth leakage circuit breaker may respond to:

    • Overload
    • Short circuit
    • Earth leakage

    Before investigating residual current, confirm which function caused the trip. Check the breaker’s trip indication, relay flag, event log or associated monitoring system.

    Record:

    • Date and time
    • Equipment operating at the time
    • Weather and humidity
    • Recent maintenance or wiring changes
    • Whether the event occurred during startup or steady operation
    • Drive speed and motor load
    • The number of circuits energized
    • Any related alarms
    • Whether the device reset normally

    If the event was caused by overload or short circuit, changing earth leakage settings will not solve it. Likewise, a genuine earth fault should not be treated as an overcurrent-coordination problem.

    Step 2: Review the device and application

    Obtain the exact catalog number and verify:

    • Rated current
    • Rated residual operating current
    • Operating-time characteristic
    • Number of poles
    • System voltage and frequency
    • Applicable waveform or load compatibility
    • Interrupting rating
    • Environmental limits
    • Upstream and downstream protective devices
    • Manufacturer’s wiring requirements

    A device intended for personnel protection may have a much lower trip threshold than one intended primarily for equipment or fire protection. The setting must match the circuit’s required protective purpose and applicable electrical codes.

    Adjustable thresholds and time delays should be changed only after an engineering review confirms that protection, fault-clearing time and regulatory requirements will remain satisfied.

    Fuji Electric’s earth leakage protective relay portfolio includes configurations with different sensitive-current and time-delay settings, allowing protection to be coordinated for the intended application. 

    Step 3: Inspect the installation

    A careful visual inspection often reveals the problem before advanced testing is needed.

    Look for:

    • Water or condensation
    • Corrosion
    • Carbon tracking
    • Damaged insulation
    • Crushed or overheated cables
    • Loose terminals
    • Contaminated connectors
    • Incorrect cable glands
    • Damaged motor leads
    • Improperly terminated shields
    • Neutral and earth conductors connected downstream
    • Recent field modifications
    • Signs of overheating in the protective device

    Pay particular attention to outdoor equipment, washdown areas, pumps, cooling towers, wastewater equipment and circuits that have been idle. Moisture can reduce insulation resistance enough to cause a trip, especially when a motor or heater is first energized.

    Do not assume that drying the equipment permanently solves the problem. Determine how moisture entered and correct the enclosure, sealing, drainage or heating issue.

    Step 4: Verify residual-current transformer wiring

    Earth leakage relays commonly use a zero-phase current transformer, or ZCT. All conductors that normally carry load current must pass through the sensing window in the correct arrangement.

    For a three-phase, four-wire circuit, this generally means all three phase conductors and the neutral pass through the ZCT. The protective-earth conductor does not.

    Check for:

    • A phase conductor routed outside the transformer
    • A neutral omitted from the transformer
    • A protective-earth conductor passing through it
    • Conductors passing through in different directions
    • Downstream neutral current returning through another circuit
    • A neutral-to-earth bond on the load side
    • Incorrect ZCT polarity or relay wiring
    • ZCT secondary wiring routed near high-noise conductors
    • An incorrectly sized sensing window

    A shared neutral can cause the outgoing and returning current measured by one device to differ even when no insulation fault is present. Each protected circuit must have a defined and correctly routed return path.

    Follow the manufacturer’s requirements for cable placement, secondary wiring, shielding and maximum distance between the ZCT and relay.

    Step 5: Measure the standing leakage current

    Use a leakage-current clamp meter capable of resolving the expected residual current.

    To measure total leakage, place the clamp around all current-carrying conductors for the protected circuit, not around the protective-earth conductor alone. The magnetic fields from the normal load currents cancel, leaving the residual component.

    Measure leakage under several conditions:

    • All loads off
    • Loads energized individually
    • Normal operation
    • Maximum production or HVAC demand
    • Startup
    • Different VFD speeds
    • Dry and humid conditions
    • Before and after filters or branches, where accessible

    Compare the measured value with the device’s operating threshold and non-tripping region. If normal standing leakage is already close to the trip threshold, a relatively small transient or additional load may cause operation.

    Do not rely on one reading. Some leakage varies with drive speed, carrier frequency, contactor operation, temperature and moisture. A meter with logging or peak-capture capability can help identify intermittent events.

    Step 6: Divide the circuit to locate the source

    If several loads are protected by one device, isolate them systematically.

    A practical method is to:

    1. De-energize the system safely.
    2. Disconnect or isolate downstream branches according to an approved procedure.
    3. Re-energize the minimum circuit.
    4. Add one branch at a time.
    5. Measure leakage after each addition.
    6. Record the incremental contribution from every load.

    This process reveals whether one piece of equipment has excessive leakage or several acceptable loads are adding up to an unacceptable total.

    Avoid random disconnection and repeated resetting. A controlled test plan produces better evidence and reduces risk.

    If disconnecting a particular load eliminates the problem, continue investigating that branch. The fault may be in the equipment, its cable, an EMC filter or its connection, not necessarily in the primary protective device.

    Step 7: Test insulation appropriately

    Insulation-resistance testing can identify degraded motors, heaters, cables and other equipment. However, a high-voltage insulation test can damage variable frequency drives, surge protectors, electronic power supplies, filters, sensors and control electronics.

    Before testing:

    • Follow the equipment manufacturer’s procedure.
    • Isolate sensitive electronic devices.
    • Disconnect surge-protective components where required.
    • Use the correct test voltage.
    • Discharge the circuit safely after testing.
    • Record results by phase and compare them over time.

    A single pass/fail result may not tell the whole story. Trending insulation resistance can reveal gradual deterioration before it causes repeated trips.

    Low readings should be investigated for moisture, contamination, cable damage, motor-winding deterioration or an actual connection to earth.

    Why variable frequency drives can increase leakage current

    Variable frequency drives switch their output voltage rapidly. The resulting high-frequency components can couple through the capacitance between:

    • Motor windings and the motor frame
    • Motor conductors and protective earth
    • Shielded cable conductors and the shield
    • Output filters and ground
    • The drive’s internal EMC filter and ground

    Long motor cables increase capacitance and can therefore increase high-frequency leakage current. Higher carrier frequencies may also increase the leakage component.

    Fuji Electric’s FRENIC-Ace guidance recommends several possible measures when an upstream earth leakage breaker trips:

    • Reduce the drive’s carrier frequency where permitted.
    • Shorten the cable between the drive and motor.
    • Review the breaker’s sensitivity.
    • Use an earth leakage device designed to address high-frequency current components.

    These measures must be applied carefully. Reducing carrier frequency can increase motor noise and may not be permitted for every motor type. Changing protection sensitivity requires a code and safety review. Always follow the manuals for the specific drive, motor and protective device.

    Check EMC filters and other electronic loads

    Many electronic devices intentionally connect capacitors between their power circuits and protective earth to control electromagnetic interference. This creates a small normal leakage current.

    Potential contributors include:

    • AC drives
    • Servo drives
    • UPS equipment
    • Switching power supplies
    • Computer equipment
    • LED drivers
    • Line filters
    • Inverters
    • Soft starters
    • Heating controls
    • Surge-protection devices

    One device may not create enough leakage to cause a trip. A panel containing dozens of such devices may.

    Obtain the manufacturer’s maximum protective-conductor current or leakage-current data for each load. Add an appropriate margin for variation, transients and future equipment. Measurements should then be used to validate the estimate.

    Never remove an EMC filter or its earth connection without the equipment manufacturer’s approval. Doing so can create electric-shock, emissions and equipment-performance problems.

    Look for switching and transient events

    If the device trips only when equipment is energized, consider transient leakage rather than continuous leakage.

    Possible sources include:

    • Charging of filter capacitors
    • Simultaneous startup of multiple drives
    • Contactor switching
    • Transformer energization
    • Utility disturbances
    • Lightning-related surges
    • Surge-protection-device operation
    • Transfer between utility and generator power
    • Power restoration after an outage

    Correlate trip timestamps with equipment logs and power-quality data. Staggering equipment startup may reduce the combined transient while also lowering inrush demand.

    If surge protective devices are involved, inspect their condition indicators and verify correct coordination. A degraded device can develop excessive leakage.

    Confirm earth leakage device compatibility

    Modern electronic loads can produce residual currents containing frequencies and waveforms that differ from a simple sinusoidal AC fault.

    The protective device must be suitable for:

    • The power-system arrangement
    • The connected load technology
    • Expected residual-current waveform
    • Frequency content
    • DC components, where applicable
    • Required personnel or equipment protection
    • Applicable national and local standards

    Do not assume an older earth leakage device is appropriate after conventional motors or resistive loads have been replaced by drives and electronic equipment.

    Fuji Electric’s G-TWIN line includes molded-case circuit breakers and earth leakage circuit breakers for distribution and motor applications, with product families designed for applicable international requirements. The exact model and characteristic should be selected with reference to the current catalog and the application’s governing standards.

    Coordinate upstream and downstream protection

    Multiple earth leakage devices in series can cause the upstream main device to trip before, or at the same time as, the device closest to the fault. This can shut down a much larger area than necessary.

    Selective coordination may use:

    • Different residual-current thresholds
    • Time-delayed upstream protection
    • Separate branch protection
    • Appropriate device characteristics
    • Monitoring relays at selected levels

    The objective is for the device closest to the fault to operate first while upstream protection remains available for backup.

    Time delay must never be introduced where it would violate required personnel-protection or disconnection times. Coordination should be documented through an engineering study rather than established through trial and error.

    Preventing unwanted trips

    Once the immediate cause is identified, the following design and maintenance practices can reduce recurrence.

    Divide electronic loads among circuits

    Avoid placing too many leakage-producing devices behind one highly sensitive protective device. Segmenting loads reduces accumulated leakage and makes future troubleshooting easier.

    Segmentation should preserve required protection and avoid creating unacceptable operational dependencies.

    Keep drive-to-motor cables within specified limits

    Use the shortest practical motor cable and follow the drive manufacturer’s recommendations for:

    • Cable type
    • Shielding
    • Grounding
    • Carrier frequency
    • Output reactors or filters
    • Motor insulation
    • Permitted cable length

    Long cable runs should be identified during design rather than discovered during commissioning.

    Select filters as part of the system

    Choose line and output filters based on the drive, cable, motor and electromagnetic-compatibility requirements. Verify their expected earth leakage under normal operation.

    Separate neutral and protective earth correctly

    Maintain the required neutral-to-earth bonding arrangement for the power system. Do not create additional downstream bonds that provide parallel return paths.

    Protect equipment from moisture

    Use suitable enclosures, glands, drains, heaters and ventilation. Inspect outdoor and washdown equipment before seasonal startup.

    Stagger equipment energization

    Sequential startup can reduce combined transient leakage and power-system inrush after a power interruption.

    Provide leakage-current margin

    The expected normal leakage should remain comfortably below the protective device’s operating threshold. The appropriate margin depends on the device, application, standards and load variability.

    Trend instead of waiting for a trip

    Periodic or continuous residual-current monitoring can show deterioration before the circuit reaches the trip point. Alarm-only earth leakage relays may be useful where early warning is needed in addition to correctly designed fault protection.

    Test protective devices regularly

    Operate the built-in test function at the interval required by the manufacturer and facility procedures. The test button checks important internal functions but does not replace a complete inspection or calibrated trip test.

    Fuji Electric recommends regular functional testing, visual inspection and verification of connections for earth leakage circuit breakers. A device that fails to trip, cannot reset reliably or shows damage should be removed from service and evaluated by qualified personnel.

    Troubleshooting checklist

    When an earth leakage device trips unexpectedly, ask:

    1. Which protective function operated?
    2. What equipment was running or starting?
    3. Has wiring or equipment recently changed?
    4. Is there evidence of moisture, contamination or insulation damage?
    5. Are all current-carrying conductors routed correctly through the ZCT?
    6. Is the neutral shared or connected to earth downstream?
    7. What is the standing leakage current?
    8. Which branch adds the largest leakage component?
    9. Does leakage change with VFD speed or carrier frequency?
    10. Are motor cables unusually long?
    11. Do EMC filters contribute significant normal leakage?
    12. Did the trip coincide with switching, a surge or power restoration?
    13. Is the protective device appropriate for the load’s waveform?
    14. Are upstream and downstream devices selectively coordinated?
    15. Does the device pass its required functional and calibrated tests?

    Fix the cause, not the symptom

    Preventing nuisance trips is not a matter of making the earth leakage device less protective. It requires determining whether the trip is caused by a genuine fault, accumulated normal leakage, high-frequency current, a transient or an installation error.

    Fuji Electric provides earth leakage circuit breakers, earth leakage protective relays and related distribution and control equipment for industrial and commercial electrical systems. 

    By combining correct device selection with careful wiring, leakage-current measurement, circuit segmentation and preventive maintenance, facilities can improve continuity without compromising electrical safety.

  • How to Select Pressure Transmitters and Flow Meters for Midstream Oil and Gas Applications

    How to Select Pressure Transmitters and Flow Meters for Midstream Oil and Gas Applications

    Midstream oil and gas operations depend on accurate measurements to transport, process and store crude oil, natural gas, natural gas liquids and related products safely and efficiently. Flow and differential pressure measurements support applications ranging from pipeline monitoring and terminal operations to filtration, compression, storage and utility steam systems.

    Selecting the right instrument requires more than choosing a measurement range. The fluid’s properties, operating envelope, required accuracy, installation conditions and purpose of the measurement all affect which technology will perform reliably.

    This guide explains how to evaluate differential pressure transmitters and flow meters for liquid, gas and steam applications across midstream facilities.

    Begin with the measurement objective

    Before comparing instruments, define what the measurement needs to accomplish. A meter used for operational monitoring may have different accuracy, diagnostics and documentation requirements from one used for inventory control, allocation or custody transfer.

    Typical midstream measurement objectives include:

    • Process control
    • Pipeline balancing
    • Pump or compressor performance monitoring
    • Filter and strainer condition monitoring
    • Leak detection
    • Storage-tank level measurement
    • Terminal loading and unloading
    • Fuel-gas monitoring
    • Steam and utility energy management
    • Allocation or custody transfer

    For custody-transfer or regulated measurement, the complete metering system must meet the applicable contractual, regulatory and industry requirements. A standard process flow meter should not automatically be assumed suitable for fiscal measurement.

    Once the objective is clear, establish the allowable uncertainty, required turndown, response time, output signals and maintenance expectations.

    Define the complete process envelope

    A flow meter or pressure transmitter should be selected for every credible operating condition, not only the normal flow rate.

    Document the following:

    • Minimum, normal and maximum flow
    • Minimum, normal and maximum pressure
    • Design pressure and potential pressure surges
    • Minimum, normal and maximum temperature
    • Fluid composition and density
    • Viscosity and conductivity, where relevant
    • Vapor pressure and potential for flashing
    • Gas compressibility
    • Solids, wax, scale or entrained liquid
    • Corrosive or sour-service components
    • Single-phase or multiphase conditions
    • Required pressure-drop limit

    Composition matters because crude oil, refined products, natural gas and NGLs can behave very differently. Changes in temperature, pressure or composition can alter density and other properties used to calculate mass or standard volumetric flow.

    For steam, determine whether the service is saturated or superheated. Also establish the expected pressure, temperature, steam quality and likelihood of condensate. A meter designed for dry saturated steam may not provide reliable results in wet-steam conditions.

    When to use differential pressure measurement

    Differential pressure, or DP, measurement is one of the most established methods for measuring flow in pipelines and process facilities. A primary element, such as an orifice plate, flow nozzle or Venturi, creates a restriction. The transmitter measures the resulting pressure difference, which is related to the square of the flow rate.

    DP technology can be applied to liquids, gases and steam. Its strengths include:

    • Broad industry familiarity
    • Availability across many pipe sizes and pressure classes
    • Suitability for high-temperature and high-pressure service
    • No moving parts in the transmitter
    • Established calculation and installation standards
    • Flexibility in primary-element design and materials

    DP measurement is especially attractive where operators already have standardized primary elements, manifolds, impulse piping and maintenance procedures.

    Its limitations should also be considered. A restriction creates permanent pressure loss, and the square-root relationship between differential pressure and flow can limit usable turndown. Accuracy depends on the primary element, piping geometry, process data, transmitter performance and installation quality, not on the transmitter alone.

    Select the DP range around actual flow conditions

    The transmitter must resolve the differential pressure generated at low flow while safely handling the maximum differential and line pressure.

    Because flow is proportional to the square root of differential pressure, a system operating at 50% of its maximum flow produces only about 25% of the maximum DP. At 10% flow, the signal falls to approximately 1% of maximum DP. An unnecessarily broad DP range can therefore reduce useful low-flow resolution.

    Work with the primary-element supplier to determine:

    • DP at minimum, normal and maximum flow
    • Required beta ratio or restriction geometry
    • Permanent pressure loss
    • Reynolds-number range
    • Gas expansion factor, where applicable
    • Discharge coefficient
    • Temperature effects on the pipe and primary element
    • Required upstream and downstream straight runs
    • Overall calculated uncertainty

    ASME PTC 19.5 addresses differential-pressure-class flow measurement for liquids, gases and vapors, including discharge coefficients, expansion factors and thermal effects.

    The final selection should be based on the transmitter’s calibrated-span performance rather than its maximum available range.

    Do not overlook static pressure

    A DP transmitter may be measuring a relatively small differential while both sides of its sensor are exposed to very high line pressure. This is common in natural-gas pipelines, compressor stations and other high-pressure services.

    Confirm:

    • Maximum allowable working pressure
    • Static-pressure rating
    • Overpressure limit on either side
    • Zero shift caused by static pressure
    • Pressure cycling and surge conditions
    • Required process-connection rating

    Fuji Electric offers high-static-pressure differential transmitters for oil and gas applications. Specialized FCX designs can measure small differential pressures while operating at static pressures up to 20,000 psi, depending on the configuration.

    A high line-pressure rating alone is not enough. The transmitter must maintain the required accuracy and stability under the expected combination of static pressure, differential pressure and temperature.

    Match wetted materials to the process

    Every component exposed to the process must be chemically and mechanically compatible with the fluid. This includes diaphragms, flanges, gaskets, impulse tubing, manifolds, seals and the primary flow element.

    Potential concerns include:

    • Hydrogen sulfide and sour gas
    • Carbon dioxide
    • Chlorides and produced water
    • Corrosion inhibitors and treatment chemicals
    • Aromatic hydrocarbons
    • Hydrogen permeation
    • Erosion from entrained solids
    • Low-temperature NGL service

    Possible wetted materials include stainless steel, Hastelloy, Monel, tantalum and other specialty materials. The appropriate choice depends on the process composition and operating conditions. Compliance with project-specific sour-service requirements should be verified separately.

    Fuji Electric’s FCX pressure-transmitter portfolio provides a range of wetted-material options for corrosive and demanding process services. 

    A diaphragm seal may be appropriate when the process is corrosive, viscous, prone to plugging, sanitary or extremely hot or cold. However, seals and capillaries can affect response time and temperature performance. Seal size, fill fluid, capillary length and ambient-temperature exposure must be evaluated as a complete system.

    Design the impulse-piping arrangement correctly

    Many apparent transmitter problems originate in the impulse lines rather than the sensor. Poor routing can trap gas in liquid service, collect liquid in gas service or create unequal hydrostatic heads.

    As a general practice:

    • For clean liquid service, mount the transmitter below the pressure taps so trapped gas can return to the process.
    • For clean gas service, mount it above the taps so condensate can drain back to the pipe.
    • For steam service, use condensate pots or equivalent arrangements and maintain equal liquid heads.
    • Keep high- and low-pressure impulse lines as short, direct and symmetrical as practical.
    • Protect impulse lines from freezing, excessive heat, vibration and mechanical damage.
    • Provide an appropriate manifold for isolation, equalization and calibration.

    ASME MFC-8M describes practices for transmitting pressure signals from a primary flow device to the secondary instrument without introducing unnecessary uncertainty.

    For remote seals, matched capillary lengths and similar ambient exposure help reduce differential temperature effects.

    Choosing a flow-meter technology for liquids

    No single flow-meter technology is best for every midstream liquid application. Selection depends on fluid properties, accuracy requirements, pressure-drop limits and whether the pipe can be modified.

    Clamp-on ultrasonic meters

    Clamp-on ultrasonic flow meters attach to the outside of an existing pipe. They require no process penetration and typically produce no additional pressure loss.

    They can be a strong choice for:

    • Flow surveys
    • Temporary verification
    • Energy assessments
    • Leak investigations
    • Applications where shutting down or cutting the pipe is undesirable
    • Retrofitting existing systems

    Successful application depends on pipe material, wall thickness, liner condition, pipe condition, acoustic properties and the availability of a fully developed flow profile. The pipe must normally remain full of liquid, and heavy deposits or aeration can weaken the ultrasonic signal.

    Spool-piece ultrasonic meters

    Inline ultrasonic meters can provide higher performance and repeatability through a controlled meter body and defined acoustic paths. Fuji Electric’s three-path FST spool-piece ultrasonic meter, for example, is specified for accuracy of up to ±0.2% of rate in supported configurations, with hazardous-area versions and digital communications available.

    These meters may suit refined products, compatible hydrocarbons and other clean-liquid services when their materials, pressure rating and fluid-property requirements are satisfied.

    Electromagnetic meters

    Electromagnetic flow meters provide no obstruction and minimal pressure loss, but they require an electrically conductive liquid. They are therefore suitable for produced water, utility water and many water-based chemical streams, not most refined hydrocarbons, crude oils or other nonconductive petroleum products.

    Differential-pressure meters

    DP meters remain useful for a wide range of liquid duties, particularly at high pressure or temperature. Their principal tradeoffs are permanent pressure loss and more limited turndown than some ultrasonic technologies.

    The decision should be based on lifecycle performance rather than purchase price alone. Installation labor, shutdown requirements, pumping energy, calibration and long-term maintenance can outweigh the initial cost of the instrument.

    Choosing a meter for natural gas and process gas

    Gas measurement requires accurate pressure, temperature, composition and compressibility information. A volumetric flow value at actual line conditions cannot be compared directly with a value referenced to standard conditions unless the appropriate compensation is applied.

    Evaluate:

    • Actual and standard volumetric flow
    • Gas composition and molecular weight
    • Operating pressure and temperature
    • Compressibility factor
    • Required turndown
    • Gas cleanliness
    • Entrained liquid or mist
    • Pulsation from compressors or regulators
    • Required flow conditioning
    • Allocation or custody-transfer requirements

    DP measurement is widely used for gas flow and can be effective across demanding pressure classes. A multivariable calculation may use DP, static pressure and temperature to determine compensated flow.

    Wet gas, slugging or multiphase flow requires specialized analysis. A meter designed for clean, single-phase natural gas should not be expected to retain its stated performance when liquid loading is significant.

    Choosing a steam flow meter

    Steam measurement presents several challenges: high temperature, changing density, condensation and the need to minimize energy loss.

    Common choices include DP, vortex and ultrasonic technologies.

    Differential-pressure steam measurement

    DP systems are established and suitable for high-pressure and high-temperature applications. Correct impulse-piping design is essential. Both transmitter legs should contain stable, equal condensate columns to prevent false differential pressure.

    Pressure and temperature compensation may be required to calculate mass flow when steam density changes.

    Vortex flow meters

    Vortex meters are often used for general saturated and superheated steam service. They have no moving parts and can provide a practical balance of performance and maintenance requirements. They do, however, require adequate straight piping and can be affected by low flow, vibration and wet steam.

    Clamp-on ultrasonic steam meters

    Clamp-on ultrasonic technology enables saturated-steam measurement without cutting the pipe or introducing an obstruction. It can eliminate meter-induced pressure loss and simplify retrofit installation.

    Fuji Electric’s FSJ ultrasonic steam flow meter is designed for clamp-on saturated-steam measurement. It requires no process penetration, has no moving parts and can support steam-energy monitoring without adding pressure loss.

    Confirm that the steam pressure, temperature, pipe size, pipe material, wall thickness and steam condition fall within the selected meter’s published limits. Superheated or wet steam should not be assumed compatible with an instrument specified only for saturated steam.

    Evaluate installation effects

    Even a highly accurate meter can produce poor results if installed in a disturbed flow profile.

    Review:

    • Required upstream and downstream straight-pipe lengths
    • Proximity to elbows, tees, valves and reducers
    • Multiple out-of-plane elbows
    • Control-valve location
    • Pump or compressor discharge pulsation
    • Swirl and asymmetric velocity profiles
    • Pipe vibration
    • Whether the pipe remains full
    • Sensor orientation
    • Accessibility for calibration and maintenance

    Where adequate straight pipe is unavailable, a flow conditioner or a technology less sensitive to profile distortion may be needed. Avoid treating catalog accuracy as installed-system accuracy. Total uncertainty includes the meter, transmitter, process-property inputs, installation and any compensation calculations.

    Specify hazardous-area and functional requirements

    Midstream instruments commonly operate in classified locations. The selected model and complete installation must carry the required approvals for the gas group, temperature class, protection method and area classification.

    Also define:

    • 4–20 mA and HART requirements
    • Digital communication protocols
    • Local display and configuration
    • High- or low-failure alarm behavior
    • Environmental enclosure rating
    • Electromagnetic compatibility
    • Surge and lightning protection
    • Functional-safety requirements
    • Cybersecurity requirements for connected instruments
    • Calibration certificates and material traceability

    Fuji Electric’s FCX-AIV pressure and DP transmitters combine 4–20 mA/HART communication with a fast measurement cycle, long-term stability and IEC 61508 SIL 2/SIL 3 certification in applicable configurations.

    Functional-safety certification does not, by itself, make an instrument suitable for a safety instrumented function. The complete loop must be designed and verified against the project’s safety requirements.

    Look at lifecycle cost, not just instrument cost

    The lowest-priced meter is not necessarily the lowest-cost solution. A lifecycle comparison should include:

    • Installation and piping modifications
    • Required shutdown time
    • Permanent pressure loss
    • Pumping or compression energy
    • Calibration frequency
    • Impulse-line maintenance
    • Exposure to erosion or fouling
    • Spare-parts strategy
    • Diagnostic capability
    • Local technical support
    • Expected service life

    A clamp-on meter may reduce installation cost and avoid a shutdown. A DP system may offer familiarity and robust high-pressure performance. A spool-piece ultrasonic meter may provide higher accuracy with little pressure loss. The right answer depends on the application’s priorities.

    A practical selection checklist

    Before finalizing a differential pressure transmitter or flow meter, confirm that the specification answers these questions:

    1. What fluid or steam condition will be measured?
    2. Is the process consistently single phase?
    3. What are the minimum, normal, maximum and design conditions?
    4. Is the measurement for control, monitoring, allocation or custody transfer?
    5. What installed-system uncertainty and turndown are required?
    6. How much permanent pressure loss is acceptable?
    7. Are all wetted materials compatible with the process?
    8. Can the instrument withstand the maximum static pressure and overpressure?
    9. Are adequate straight pipe and mounting access available?
    10. What compensation for pressure, temperature, density or composition is needed?
    11. What hazardous-area approvals and communications are required?
    12. How will the device be isolated, verified and maintained?
    13. What is the expected lifecycle cost?

    Select the measurement system, not only the instrument

    Reliable midstream measurement depends on the interaction of the sensor, process connections, primary element, piping, compensation data and control system. Selecting each part independently can produce a system that appears correct on paper but fails to deliver the required performance in operation.

    Fuji Electric provides differential pressure transmitters and flow-meter technologies for liquid, gas and steam applications across upstream and midstream operations. Its portfolio includes FCX pressure and DP transmitters, clamp-on and spool-piece ultrasonic liquid meters, and clamp-on ultrasonic steam measurement solutions.Engaging a measurement specialist early can help validate the operating envelope, materials, installation geometry and uncertainty requirements, before they become costly field problems.

  • How to Select a Ring Compressor for Wastewater Systems

    How to Select a Ring Compressor for Wastewater Systems

    Aeration is one of the most important, and often one of the most energy-intensive, processes in wastewater treatment. It supplies the oxygen required by aerobic microorganisms, keeps solids suspended and can support mixing, filter backwashing and other plant operations.

    For smaller tanks, decentralized treatment systems and applications requiring clean, oil-free air at relatively low pressure, a ring compressor can offer a compact and reliable solution. Also known as a regenerative, side-channel or ring blower, this equipment has no oil in the compression chamber and relatively few wear components.

    Successful selection requires more than matching a catalog’s maximum airflow to the process requirement. Engineers must determine the airflow and pressure required at the same operating point, correct for actual site conditions and consider how demand will change over time.

    What is a ring compressor?

    A ring compressor uses an impeller mounted directly on a motor shaft. As the impeller rotates, its blades draw air into the housing and repeatedly accelerate it through a side channel. Each pass adds energy to the air before it reaches the discharge.

    Unlike a positive-displacement blower, a ring compressor does not trap and move a fixed volume of air with each revolution. Its delivered airflow changes significantly as system pressure changes. This makes the manufacturer’s performance curve essential to proper selection.

    Ring compressors are typically well suited to applications requiring:

    • Clean, oil-free air
    • Moderate airflow and pressure
    • Continuous operation
    • Low maintenance
    • Compact equipment
    • Relatively quiet operation
    • Pressure or vacuum capability

    Fuji Electric ring compressors use direct-drive motors and are designed to supply oil-free air without internal lubrication.

    Where are ring compressors used in wastewater treatment?

    Common wastewater applications include:

    • Aeration of small activated-sludge tanks
    • Package treatment plants
    • Equalization-tank mixing
    • Aerobic digesters
    • Lagoon aeration
    • Membrane or media aeration
    • Airlift pumping
    • Grit or grease separation
    • Filter backwashing
    • Odor-control processes
    • Instrument or sampling systems

    In biological treatment, the blower supplies oxygen that supports the microorganisms responsible for breaking down organic material. It may also provide mixing that prevents solids from settling.

    Ring compressors are not the best fit for every plant. Very large basins, deep tanks or systems with high airflow demand may be better served by positive-displacement or turbo blowers. The correct technology should be chosen by comparing the complete operating range, efficiency, turndown and lifecycle cost.

    Step 1: Determine the required airflow

    Airflow should be based on the process requirement, not an estimate based only on tank volume.

    For biological aeration, the required oxygen transfer depends on factors such as:

    • Influent biochemical oxygen demand
    • Ammonia loading and nitrification requirements
    • Biomass concentration
    • Required dissolved oxygen
    • Wastewater temperature
    • Tank geometry
    • Mixing requirements
    • Diffuser type and condition
    • Site elevation
    • Required operating margin

    The process designer typically begins with the actual oxygen requirement and converts it to a standard oxygen requirement using appropriate correction factors. Diffuser performance is then used to estimate the standard airflow needed to deliver that oxygen.

    For mixing-limited applications, the minimum airflow needed to keep solids suspended may be higher than the airflow calculated from oxygen demand. Both conditions should be checked.

    Airflow should be specified in clearly defined units. SCFM represents airflow referenced to standard conditions, while ACFM represents the volume at the actual inlet temperature and pressure. These values are not interchangeable. Confirm the reference temperature, pressure and humidity used by the equipment manufacturer and process designer.

    Avoid applying an arbitrary oversizing percentage without analysis. Excess air wastes energy, may cause excessive turbulence and can make dissolved-oxygen control difficult. A reasonable design margin should reflect real uncertainty, anticipated growth and standby requirements.

    Step 2: Calculate total system pressure

    A ring compressor must overcome the resistance of the entire aeration system. Total required discharge pressure normally includes:

    1. Static water depth above the diffuser
    2. Diffuser or sparger pressure loss
    3. Friction loss in headers and branch piping
    4. Losses through valves, fittings and check valves
    5. Fouling allowance
    6. Any additional required pressure at the point of use

    Static head is often the largest component. For water near standard conditions, every foot of submergence requires approximately 0.433 psi, or about 12 inches of water column. Wastewater density and actual operating conditions may require an adjustment.

    The pressure calculation should use the maximum operating water level, not simply the nominal diffuser depth.

    Diffuser pressure loss must come from the diffuser supplier at the expected airflow. Include the pressure increase caused by aging, fouling or scaling. Fine-bubble diffusers may become progressively more restrictive if they are not cleaned or maintained.

    Piping loss should be calculated at the maximum design airflow. Undersized piping can add significant pressure loss and move the compressor away from its efficient operating range.

    Step 3: Select from the performance curve

    Never select a ring compressor from its maximum airflow and maximum pressure values independently. Those values occur at different points on the performance curve.

    As discharge pressure increases, the available airflow generally decreases. The correct model is the one that delivers the required airflow at the calculated total system pressure.

    For every candidate model, plot or identify:

    • Normal operating point
    • Maximum-flow operating point
    • Maximum-pressure operating point
    • Minimum expected system resistance
    • Future or fouled-system condition

    The selected point should remain inside the manufacturer’s permitted continuous operating region. It should not be located at the extreme edge of the curve, where small changes in pressure can cause a large loss of airflow or motor overload.

    Fuji Electric offers single-stage ring compressors with capacities up to approximately 790 SCFM and maximum pressures up to 139 inches of water in current listed configurations. Actual capacity depends on the model and operating pressure.

    Step 4: Choose between single-stage and two-stage designs

    Single-stage and two-stage ring compressors address different pressure requirements.

    Single-stage ring compressors

    A single-stage unit passes air through one regenerative compression stage. It is generally appropriate when the system requires moderate pressure and airflow.

    Potential benefits include:

    • Simpler construction
    • Compact footprint
    • Lower initial cost
    • Broad model availability
    • Good performance for shallow or moderately deep aeration systems

    Fuji Electric’s wastewater portfolio includes VFZ and VFB single-stage ring compressors for aeration and related applications.

    Two-stage ring compressors

    A two-stage unit sends air through two regenerative stages to produce a higher pressure differential. This can make it a better fit for deeper tanks, more restrictive diffusers or systems with higher combined losses.

    The additional pressure capability should not be treated as a reason to oversize. A two-stage blower operating unnecessarily far below its intended pressure range may use more energy than a correctly selected single-stage unit.

    Fuji Electric’s 2VFB Series provides two-stage options with direct-drive, totally enclosed fan-cooled motors for higher-pressure applications.

    Step 5: Correct performance for altitude and temperature

    Published curves are typically based on defined inlet conditions. Air density decreases as altitude and inlet temperature increase. Consequently, a compressor installed at a high-elevation plant or in a hot equipment enclosure may move less mass of air, and therefore deliver less oxygen, than the same unit under standard conditions.

    Evaluate:

    • Site elevation
    • Minimum and maximum ambient temperature
    • Expected inlet-air temperature
    • Barometric pressure
    • Humidity
    • Enclosure ventilation
    • Heat recirculation around the compressor

    Corrections may affect oxygen delivery, discharge temperature and motor loading. Ask the manufacturer to confirm the corrected operating point when the installation differs materially from the stated curve conditions.

    A blower room or acoustic enclosure also needs adequate ventilation. Ring compressors add heat to the air as pressure rises, and recirculating hot discharge air into the inlet can further reduce performance.

    Step 6: Confirm motor and electrical requirements

    Once the aerodynamic operating point is established, verify the motor and power supply.

    The specification should identify:

    • Required horsepower
    • Voltage and phase
    • Supply frequency
    • Motor full-load current
    • Service factor, if applicable
    • Motor enclosure
    • Insulation class
    • Thermal protection
    • Starts per hour
    • Continuous or intermittent duty
    • Required electrical certifications

    Three-phase motors are generally preferred for larger continuous-duty systems. Single-phase options may be useful for smaller packaged plants where three-phase power is unavailable.

    Ring compressors can overload under operating conditions that may not be intuitive. The motor must be checked across the entire anticipated pressure and airflow range, not just at the design point.

    Fuji Electric offers direct-drive ring compressors across a range of motor sizes, voltages and single- or three-phase configurations. Current model data should be used to confirm electrical compatibility.

    Step 7: Plan for variable demand

    Wastewater oxygen demand changes with influent loading, temperature and time of day. A blower sized only for the peak condition may spend much of its life supplying more air than the process needs.

    Common control approaches include:

    • On/off operation
    • Staging multiple compressors
    • Modulating an inlet or discharge valve
    • Variable-frequency control
    • Dissolved-oxygen-based control
    • Timed aeration cycles

    A variable frequency drive can reduce output when demand falls, but the compressor must remain within its approved speed, motor-current and temperature limits. Regenerative-blower performance does not necessarily follow the same relationships used for conventional centrifugal fans. Obtain manufacturer-approved speed ranges and corrected performance data before applying a VFD.

    For systems with a broad demand range, multiple smaller compressors may provide better control and redundancy than one large machine. Staging units also allows maintenance while part of the aeration capacity remains available.

    Step 8: Include the necessary accessories

    A complete ring-compressor installation typically requires more than the compressor itself.

    Depending on the system, specify:

    • Inlet filter or filter-silencer
    • Pressure-relief valve
    • Check valve
    • Pressure or vacuum gauge
    • Flexible connector
    • Isolation valve
    • Discharge silencer
    • Vibration-isolation mounts
    • Temperature switch or sensor
    • Airflow or pressure transmitter
    • Suitable starter or AC drive

    The inlet filter protects the close internal clearances from dust and debris. A clogged filter increases inlet restriction, reduces airflow and can raise operating temperature, so it must be accessible for inspection and replacement.

    A relief valve protects the compressor if a discharge valve closes, a diffuser header plugs or another restriction raises pressure beyond the safe operating limit. It should be sized and set according to the manufacturer’s requirements.

    Fuji Electric’s typical pressure-system arrangement includes an inlet filter, pressure-relief valve, pressure gauge and check valve. It also calls for an initial length of metal discharge pipe to handle elevated outlet-air temperature.

    Step 9: Design the piping around the compressor

    Poor piping design can reduce performance, create excessive noise and shorten equipment life.

    Good practices include:

    • Use pipe at least as large as the compressor connection unless calculations support another size.
    • Keep the inlet and discharge piping as short and direct as practical.
    • Avoid unnecessary elbows and restrictions near the ports.
    • Support the piping independently instead of placing its weight on the compressor.
    • Use a flexible connector to limit transmitted vibration and accommodate thermal movement.
    • Prevent condensate or wash water from draining into the compressor.
    • Use temperature-rated materials near the discharge.
    • Provide access to filters, valves and instruments.
    • Do not install a throttling valve where it could create an unsafe operating condition.

    Discharge air can become hot, particularly at higher pressure. Plastic or temperature-sensitive components should not be installed immediately at the outlet unless they are specifically rated for the expected temperature.

    The compressor should also be protected from water ingestion. A check valve and correctly routed piping can reduce the risk of tank water flowing backward during shutdown.

    Step 10: Consider redundancy and maintainability

    Loss of aeration can quickly affect biological treatment performance. Determine how long the process can tolerate reduced or interrupted airflow and select the redundancy strategy accordingly.

    Possible arrangements include:

    • One duty and one standby compressor
    • Multiple duty compressors with one common standby
    • N+1 capacity
    • Several staged units capable of meeting average demand after one failure
    • A spare compressor kept on site

    Automatic lead-lag rotation can equalize running hours. The control system should generate alarms for high pressure, high temperature, motor overload, low airflow and compressor failure.

    Maintenance planning should cover:

    • Inlet-filter inspection and replacement
    • Relief-valve testing
    • Check-valve inspection
    • Removal of dust from cooling surfaces
    • Motor-current trending
    • Noise and vibration checks
    • Verification of airflow and pressure
    • Inspection for loose piping or connections

    Ring compressors require no oil in the compression chamber, but “oil-free” does not mean maintenance-free. Clean inlet air, adequate cooling and operation within the approved envelope are essential to long service life.

    Step 11: Compare lifecycle energy use

    Aeration often represents a significant portion of a wastewater facility’s electricity consumption. The U.S. Environmental Protection Agency identifies proper blower sizing and aeration-system optimization as important energy-conservation measures for treatment plants.

    Compare candidate systems at representative annual operating points, not only at peak design conditions. Include:

    • Compressor input power
    • Operating hours at each load
    • Pressure loss through piping and diffusers
    • Control method
    • Standby-unit energy use
    • Filter and diffuser fouling
    • Maintenance cost
    • Expected equipment life

    Reducing avoidable system pressure can be just as valuable as selecting a more efficient compressor. Larger piping, clean diffusers and well-designed headers allow the blower to perform its job with less power.

    Ring-compressor selection checklist

    Before placing an order, confirm the following:

    1. What is the required airflow at minimum, normal and peak load?
    2. Are the stated flow units standard or actual?
    3. What oxygen-transfer and mixing assumptions were used?
    4. What is the maximum water depth above the diffusers?
    5. What are the diffuser and piping losses at design flow?
    6. What fouling allowance is required?
    7. Does the performance curve show the necessary airflow at total pressure?
    8. Is a single-stage or two-stage design more appropriate?
    9. Have altitude and inlet temperature been considered?
    10. Is the motor compatible with the available electrical supply?
    11. Will variable-speed operation or compressor staging be used?
    12. Are inlet filtration, pressure relief and backflow protection included?
    13. Is there sufficient standby capacity?
    14. Can filters and other service items be reached easily?
    15. What will the system consume over a typical year?

    Select for the operating point, not the catalog maximum

    The most important rule in ring-compressor selection is simple: airflow and pressure must be evaluated together. A unit advertised with enough maximum airflow may not deliver that airflow against the pressure created by the tank, diffusers and piping.

    Fuji Electric provides single-stage and two-stage ring compressors for wastewater aeration and related pressure or vacuum applications. The available portfolio spans compact units through higher-capacity systems, with clean, oil-free air delivery and direct-drive construction.

    By supplying the manufacturer with accurate airflow, pressure, elevation, temperature and electrical data, wastewater professionals can select a compressor that supports treatment performance without unnecessary energy use or premature equipment stress.

  • Understanding Parasitic Inductance in Power Modules, and How to Minimize It

    Understanding Parasitic Inductance in Power Modules, and How to Minimize It

    Modern IGBT and SiC power modules can switch hundreds of amperes in a fraction of a microsecond. That speed enables compact, efficient power converters, but it also makes every millimeter of the current path important.

    Conductors that appear to be simple connections on a schematic have inductance in the physical circuit. During fast switching, this parasitic, or stray, inductance can generate voltage overshoot, ringing, electromagnetic interference and additional switching loss. If it is not controlled, it can also overstress semiconductor devices and complicate parallel operation.

    Parasitic inductance cannot be eliminated completely. It can, however, be understood, estimated and minimized through coordinated module selection, mechanical design, PCB layout, busbar design and gate-drive engineering.

    What is parasitic inductance?

    Any conductor carrying current produces a magnetic field. When that current changes, energy is stored in or released from the magnetic field. This behavior gives the conductor inductance even when no discrete inductor appears in the schematic.

    Parasitic inductance is present in:

    • Power-module terminals
    • Internal module connections
    • DC busbars
    • PCB traces and planes
    • Capacitor leads and terminals
    • Cable connections
    • Fuse and contactor paths
    • Gate-drive connections
    • Current sensors
    • Snubber circuits

    The most important value is usually the total inductance of a current loop, not the inductance of one conductor considered in isolation. Both the outgoing and return paths determine the loop area and magnetic flux.

    Fuji Electric’s IGBT application guidance identifies representative stray inductances throughout practical inverter systems and explains how those inductances interact with circuit capacitances to create resonant behavior and electromagnetic emissions.

    Why a few nanohenries matter

    The voltage generated across an inductance is described by:

    VL = L * di / dt

    where:

    • (VL) is the inductive voltage
    • (L) is the parasitic inductance
    • (di/dt) is the rate of current change

    Consider a switching loop with 40 nH of total parasitic inductance. If current changes at 5,000 A/µs, the inductive voltage is:

    40 * 5000 / 200

    That voltage appears in addition to, or subtracts from, the circuit voltage according to its polarity and location. In a high-voltage converter, an extra 200 V can consume a significant part of the semiconductor’s voltage margin.

    The problem becomes more pronounced with faster devices. SiC MOSFETs can switch at substantially higher (di/dt) and (dv/dt) than conventional silicon devices. A layout that performed acceptably with an older IGBT may produce excessive overshoot or ringing after a faster device is substituted.

    The main effects of parasitic inductance

    Turn-off voltage overshoot

    When a semiconductor interrupts current, the energy stored in the commutation-loop inductance must go somewhere. It produces a voltage rise across the switching device.

    The peak device voltage can be approximated as:

    VPeak = VDC + L * di / dt

    This simplified relationship does not capture every dynamic effect, but it clearly shows why DC-link voltage, loop inductance and switching speed must be evaluated together.

    Fuji Electric’s SiC module application guidance illustrates that turn-off surge voltage rises as stray inductance increases under otherwise comparable conditions.

    Excessive overshoot can approach or exceed the module’s rated blocking voltage, reducing reliability or causing immediate failure.

    Ringing

    Parasitic inductance combines with device output capacitance, junction capacitance, bus capacitance and other stray capacitances to form resonant circuits.

    Fast switching can excite these resonances, producing high-frequency oscillation in voltage and current. Ringing can:

    • Increase peak voltage
    • Produce false gate transitions
    • Increase switching loss
    • Create conducted and radiated emissions
    • Interfere with sensing and control circuits
    • Complicate waveform measurement

    Fuji Electric provides an example in which 200 nH of stray inductance and 500 pF of capacitance create a resonance near 16 MHz.

    Gate-voltage disturbance

    Inductance in the common emitter or common source path is particularly important. Power current flowing through this inductance creates a voltage that appears in the gate-drive loop.

    The resulting feedback can:

    • Reduce effective gate voltage during turn-on
    • Slow or distort switching
    • Produce gate-voltage spikes
    • Encourage parasitic turn-on
    • Create oscillation
    • Cause unequal switching in parallel devices

    This is why modules with Kelvin emitter or Kelvin source terminals can offer a major advantage. The gate driver references a low-current auxiliary terminal rather than the high-current power path, reducing the influence of common-path inductance.

    Increased switching loss

    Designers often slow a device with more gate resistance to control overshoot caused by excessive inductance. This can reduce (di/dt) and (dv/dt), but it also increases switching time and energy loss.

    Low-inductance construction allows the semiconductor to switch closer to its intended capability without violating voltage or electromagnetic-compatibility limits.

    Fuji Electric’s recent three-dimensional wiring development for SiC power modules reduced internal parasitic inductance by approximately 70% compared with the company’s conventional structure and produced an approximately 50% reduction in switching loss under the evaluated conditions.

    Unequal current sharing

    In parallel module arrangements, unequal inductance can cause different transient voltages and switching speeds in each branch. One module may temporarily carry more current or experience greater switching stress.

    A design with equal DC, AC and gate-path resistance but unequal inductance may still share current poorly during switching. Physical symmetry matters as much as schematic symmetry.

    Identify the critical current loops

    The first step in controlling inductance is to identify where current commutates during each switching transition.

    In a typical half-bridge, the high-frequency commutation loop includes:

    1. The local positive DC-link capacitor terminal
    2. The upper or lower switching device
    3. The complementary diode or MOSFET channel
    4. The negative DC-link capacitor terminal
    5. The conductors connecting these elements

    The bulk capacitor located elsewhere in the enclosure may stabilize the average DC bus, but it cannot supply the fastest current edges effectively if long busbars or cables separate it from the module. A low-inductance local capacitor path is therefore essential.

    Other critical loops include:

    • Gate turn-on loop
    • Gate turn-off loop
    • Active-clamp loop
    • Desaturation-detection loop
    • Snubber loop
    • Current-sensor path
    • Common-mode return path

    Each loop should be evaluated independently. Reducing the power-loop inductance does not automatically correct a long or poorly referenced gate-drive loop.

    Minimize the commutation-loop area

    Loop inductance is strongly related to enclosed area. The basic design principle is to keep the outgoing and return current paths close together.

    Effective techniques include:

    • Use overlapping positive and negative conductors.
    • Place laminated busbar layers close together.
    • Use broad copper planes rather than long, narrow traces.
    • Position the DC-link capacitor close to the module terminals.
    • Avoid unnecessary bends and detours.
    • Keep connections short and direct.
    • Use several parallel connection points where appropriate.
    • Avoid large gaps between forward and return paths.

    A wide conductor alone is not necessarily low inductance. If its return path is distant, the overall loop can still have substantial inductance. Closely coupled forward and return conductors produce opposing magnetic fields, reducing external flux and loop inductance.

    Place DC-link capacitors close to the module

    At the switching frequency and its harmonics, the effective DC-link capacitor is the one connected through the lowest-inductance path.

    A practical DC link may use:

    • Bulk electrolytic capacitors for energy storage
    • Film capacitors for high-frequency current
    • Small local capacitors for the fastest switching components

    The local film or ceramic capacitor should be mounted as close as practical to the module’s DC terminals. Its terminals and connection structure are part of the loop, so a low-inductance capacitor connected through long leads may not provide a low-inductance result.

    Evaluate:

    • Capacitor equivalent series inductance
    • Terminal geometry
    • Connection length
    • Busbar overlap
    • RMS ripple-current capability
    • Voltage rating
    • Temperature
    • Lifetime
    • Fault-current behavior

    Do not choose a capacitor by capacitance alone. Its impedance across the relevant frequency range is what determines its effectiveness during switching.

    Use laminated or closely coupled busbars

    A laminated busbar places positive and negative conductors in parallel layers separated by thin insulation. This arrangement reduces loop area and provides strong magnetic-field cancellation.

    Good busbar design should:

    • Keep the layers close
    • Maintain overlap up to the module terminals
    • Avoid narrow necks
    • Minimize terminal extensions
    • Use symmetrical paths to parallel modules
    • Position capacitor connections directly across the DC layers
    • Meet creepage, clearance and insulation requirements

    Electrical, thermal and mechanical requirements must be resolved together. A very compact busbar still needs adequate insulation, current capacity, cooling and fault withstand.

    Three-dimensional electromagnetic simulation can help compare geometries before tooling is committed.

    Choose a low-inductance module package

    Some inductance exists inside the module and cannot be corrected by external layout. Package architecture therefore matters.

    Review the manufacturer’s data for:

    • Internal stray inductance
    • Terminal arrangement
    • Kelvin emitter or source availability
    • Module topology
    • Recommended busbar arrangement
    • Recommended capacitor placement
    • Switching test conditions
    • Package scalability for parallel operation

    Fuji Electric’s 7th-generation X-Series IGBT modules combine lower-loss semiconductor technology with lower-inductance package designs.

    Selecting a module with terminals that naturally support a compact commutation loop may be more effective than trying to correct an unfavorable geometry with a complicated external busbar.

    Separate the power and gate-drive paths

    The gate driver should connect to the module through a small, dedicated loop.

    Recommended practices include:

    • Place the driver close to the module.
    • Use the Kelvin emitter or source terminal where provided.
    • Route gate and return conductors together.
    • Keep the gate loop away from high-(dv/dt) nodes.
    • Avoid sharing the power-emitter or power-source path.
    • Use compact, low-inductance gate resistors.
    • Separate turn-on and turn-off paths when useful.
    • Place clamping and protection components at the gate terminals.
    • Maintain suitable isolation and creepage distances.

    The loop between the driver’s decoupling capacitor, output stage, gate and return terminal also matters. A short connection to the gate terminal is not enough if the driver’s local supply loop is large.

    For high-side devices, account for the isolation barrier, common-mode transient immunity and the parasitic capacitance of the isolated power supply.

    Control common emitter or source inductance

    Common-path inductance is shared by the load-current loop and the gate-drive return. Its induced voltage acts as feedback on the gate signal.

    To reduce it:

    • Use a module with an auxiliary emitter or source terminal.
    • Connect the driver return directly to that terminal.
    • Do not route gate-return current through the power busbar.
    • Keep the auxiliary connection short.
    • Avoid coupling the gate-return trace to the switching node.
    • Follow the module manufacturer’s recommended terminal connections.

    An oscilloscope measurement referenced to the wrong emitter or source point can also hide the true gate voltage seen by the chip. Measure gate voltage at the designated auxiliary terminal whenever possible.

    Design parallel connections symmetrically

    For parallel modules, symmetry should be maintained from the capacitor bank through the modules and into the load connection.

    Match:

    • Positive-bus inductance
    • Negative-bus inductance
    • Output-path inductance
    • Gate-loop inductance
    • Gate resistance
    • Driver propagation delay
    • Module temperature
    • Contact resistance

    A star connection is not automatically symmetrical at high frequency. The physical length, width, layer spacing and mutual coupling of each branch must be comparable.

    Individual gate resistors are generally preferable to one common resistor. Depending on the module and application, separate drivers or carefully matched driver outputs may be required.

    Fuji Electric provides dedicated application guidance for parallel IGBT-module operation as part of its power-module design resources.

    Use snubbers as a refinement, not a substitute for layout

    An RC, RCD or capacitor snubber can absorb switching energy or damp an unwanted resonance. It can be valuable when properly designed, but it should not be used to compensate for avoidable busbar inductance.

    A snubber must have its own low-inductance connection. If it is mounted far from the switching loop, its leads may prevent it from controlling the fastest transient.

    When designing a snubber, consider:

    • Circuit topology
    • Target resonant frequency
    • Peak current
    • Pulse-energy rating
    • Capacitor inductance
    • Resistor pulse capability
    • Thermal dissipation
    • Physical placement

    First reduce the source of the inductance. Then use measured waveforms or simulation to size damping components.

    Tune the gate drive after optimizing the layout

    Gate resistance is an important tool for balancing switching loss, overshoot, diode recovery and electromagnetic emissions. It should be tuned on the final mechanical layout or a representative prototype.

    Increasing turn-off gate resistance can reduce (di/dt) and overshoot, but it generally increases turn-off loss. Increasing turn-on resistance can reduce diode-recovery stress and (dv/dt), but it increases turn-on loss.

    Other techniques may include:

    • Separate turn-on and turn-off resistors
    • Multilevel gate drive
    • Active gate control
    • Miller clamping
    • Negative turn-off bias
    • Active clamping

    These features do not eliminate the need for low inductance. They work best when the underlying layout is already controlled.

    Do not copy gate-resistor values from a different test fixture without validation. Module current, DC voltage, temperature, driver impedance and parasitic inductance all influence the result.

    Pay special attention to SiC modules

    SiC MOSFETs reward low-inductance design but expose layout weaknesses quickly.

    Important considerations include:

    • Very high (dv/dt) and (di/dt)
    • Lower gate-voltage tolerance than some IGBTs
    • Potential parasitic turn-on
    • High-frequency ringing
    • Sensitivity to common-source inductance
    • Driver common-mode transient immunity
    • Short-circuit protection speed
    • Measurement bandwidth and probe quality

    A converter should not be upgraded from IGBT to SiC by changing the module alone. The busbar, capacitors, gate driver, protection circuits, cooling and PCB layout should be reevaluated as a system.

    Fuji Electric has developed low-inductance SiC packaging structures using compact current paths and copper-pin or three-dimensional interconnection technologies to support higher power density and faster switching.

    Model inductance before building hardware

    Several levels of analysis are available.

    Hand calculations

    Basic loop geometry and the relationship (V=L(di/dt)) provide valuable early estimates. They can show whether a proposed inductance is compatible with the device’s voltage margin.

    Circuit simulation

    Add estimated parasitic inductances to the switching model. Separate the inductance into meaningful elements, such as:

    • DC-positive path
    • DC-negative path
    • Module internal path
    • Capacitor connection
    • Common emitter or source
    • Gate path
    • Load connection

    One lumped inductance may reproduce voltage overshoot but will not reveal how different locations affect gate behavior or common-mode noise.

    Electromagnetic extraction

    Finite-element or partial-element-equivalent-circuit tools can extract self and mutual inductance from the actual PCB or busbar geometry. This is particularly valuable for laminated busbars, parallel modules and high-current SiC converters.

    Simulation accuracy still depends on realistic device models, capacitor characteristics, terminal geometry and boundary conditions. Prototype testing remains necessary.

    Measure without creating misleading waveforms

    Fast power-module waveforms are easy to measure incorrectly. Probe inductance, ground leads and poor connection points can create ringing that is not present in the actual circuit, or hide ringing that is.

    Use:

    • A high-bandwidth differential probe with an adequate voltage rating
    • A current probe with suitable bandwidth and current capability
    • Short probe connections
    • Manufacturer-recommended probe points
    • A compact gate-voltage probe loop
    • Proper oscilloscope isolation and grounding practices
    • Deskew between voltage and current channels when calculating switching energy

    Never use a conventional grounded oscilloscope probe on a high-side switching node unless the measurement method is explicitly designed and rated for it.

    For gate voltage, measure directly between the gate and Kelvin emitter or source terminals. For device voltage, connect as close as practical to the relevant module terminals.

    The measurement setup should be documented so results can be reproduced.

    Validate with a double-pulse test

    A double-pulse test allows engineers to evaluate switching behavior at controlled current, voltage and temperature.

    It can reveal:

    • Turn-on and turn-off energy
    • Voltage overshoot
    • Current overshoot
    • Diode reverse recovery
    • Ringing frequency
    • Gate-voltage disturbance
    • Parasitic turn-on
    • Effect of gate resistance
    • Effect of snubber components

    Test across the intended operating envelope, including:

    • Maximum DC-link voltage
    • Representative and maximum current
    • Minimum and maximum junction temperature
    • Production component tolerances
    • Expected gate-supply variation

    The final voltage margin should account for measurement uncertainty and abnormal operating conditions, not only a nominal laboratory waveform.

    Estimating loop inductance from a waveform

    If the current fall rate and inductive voltage contribution can be identified, total loop inductance can be approximated from:

    [
    L_\sigma \approx \frac{\Delta V}{di/dt}
    ]

    For example, if the inductive overshoot is 120 V while current changes at 4,000 A/µs:

    [
    L_\sigma \approx \frac{120}{4{,}000} = 0.03\text{ µH} = 30\text{ nH}
    ]

    This is a simplified estimate. Device capacitance, diode recovery, nonlinear switching behavior and measurement error can affect the result. It is still useful for comparing prototypes and validating simulation trends.

    Ringing frequency can also help estimate the combined LC network if either the effective inductance or capacitance is already known.

    A practical low-inductance design checklist

    Before releasing a power converter design, confirm:

    1. Have all high-frequency commutation loops been identified?
    2. Is the local DC-link capacitor adjacent to the module terminals?
    3. Are positive and negative conductors closely overlapped?
    4. Are busbar necks, standoffs and terminal extensions minimized?
    5. Does the module package support a compact external loop?
    6. Are Kelvin emitter or source terminals used correctly?
    7. Is the gate driver close to the module?
    8. Is the driver-supply decoupling loop compact?
    9. Are high-(dv/dt) nodes separated from gate and sensing circuits?
    10. Are parallel power and gate paths physically symmetrical?
    11. Are snubbers connected through genuinely low-inductance paths?
    12. Have parasitic elements been included in simulation?
    13. Have critical inductances been extracted from the physical geometry?
    14. Has the design been verified with a double-pulse test?
    15. Were waveforms measured using low-inductance probe connections?
    16. Is adequate voltage margin maintained at maximum current, voltage and temperature?
    17. Have switching loss, EMI and reliability been evaluated together?

    Low inductance begins with the physical design

    Parasitic inductance is not a minor correction to an otherwise complete schematic. In a fast-switching power converter, the mechanical structure is part of the electrical circuit.

    The most effective strategy is to select a suitable low-inductance power-module package, minimize the commutation-loop area, place capacitors close to the module, separate gate and power paths, and validate the finished structure under realistic switching conditions.

    Fuji Electric provides IGBT and SiC power modules, application manuals, technical documents and simulation resources to support converter design. Its 7th-generation X-Series modules feature lower-loss chip technology and low-inductance package options for industrial, renewable-energy, transportation and power-conversion applications.

    By addressing parasitic inductance early, designers can reduce voltage stress and ringing while making better use of the switching performance available from modern power semiconductors.

  • Selecting the Right HMI Unit for Commercial and Industrial HVAC Systems

    Selecting the Right HMI Unit for Commercial and Industrial HVAC Systems

    Heating, ventilation and air-conditioning systems are becoming more connected and data-driven. Operators are expected to manage multiple fans, pumps, compressors, dampers, valves and variable frequency drives while maintaining comfort, process conditions, energy efficiency and equipment availability.

    A well-selected human-machine interface, or HMI, gives operators a clear local view of this equipment. It can simplify startup, display system conditions, help personnel respond to alarms and provide access to the information needed for maintenance.

    Choosing the right HMI requires more than selecting a convenient screen size. The panel must fit the application’s control architecture, operating environment, communications requirements and users. This guide explains the principal factors to consider.

    Start by defining the HMI’s role

    An HMI is an operator interface, not necessarily the primary controller. In many HVAC systems, a programmable logic controller, dedicated HVAC controller or equipment controller runs the control sequence, while the HMI displays data and allows authorized personnel to issue commands.

    Before selecting hardware, decide what the HMI needs to do.

    Typical functions include:

    • Starting and stopping equipment
    • Changing temperature, pressure or flow setpoints
    • Displaying equipment and system status
    • Monitoring variable frequency drive speed and load
    • Showing temperatures, pressures, flow rates and valve positions
    • Presenting current and historical alarms
    • Displaying trends
    • Recording operator actions
    • Supporting equipment setup and commissioning
    • Providing maintenance and diagnostic information
    • Exchanging information with supervisory or enterprise systems

    A simple packaged air-handling unit may need only a few status screens and setpoint controls. A central utility plant may require navigation across chillers, boilers, cooling towers, pumps and multiple distribution loops. The second application will need greater processing performance, more memory, a larger display and broader connectivity.

    Creating an HMI point list before selecting the panel helps prevent both undersizing and unnecessary complexity.

    Understand the difference between an HMI and a BMS

    An HMI and a building management system, or BMS, often work together, but they serve different purposes.

    A local HMI is typically located at or near the equipment. It provides immediate access for operators, technicians and commissioning personnel. A BMS supervises conditions across a building, campus or portfolio and may coordinate scheduling, alarming, energy reporting and central control.

    A local HMI can remain valuable even when a full BMS is present because it can:

    • Give technicians access at the equipment
    • Support startup when the supervisory network is unavailable
    • Display controller and drive diagnostics in greater detail
    • Reduce dependence on a laptop for routine service
    • Provide a dedicated interface for packaged equipment
    • Limit local controls to the functions appropriate for that machine

    Define which system owns each command and setpoint. If both the HMI and BMS can write to the same value without clear priority rules, operators may see commands override one another.

    Select the appropriate performance level

    HMI requirements generally fall into three broad categories.

    Basic machine or equipment interface

    A basic HMI may be suitable for a packaged rooftop unit, pump skid, fan array or small mechanical system. These applications generally require:

    • A limited number of screens
    • Basic alarm display
    • Setpoint entry
    • Equipment status
    • One or two communications interfaces
    • Modest data logging

    Fuji Electric’s MONITOUCH TECHNOSHOT family is positioned for basic operator-interface applications. The current TS4000 range includes wide-screen models from 7 to 15.6 inches, depending on configuration, with Ethernet and USB connectivity.

    High-performance HVAC interface

    A more demanding application may include multiple controllers, extensive animation, high tag counts, complex trends, recipes, logs or several communications connections.

    Fuji Electric’s MONITOUCH V10 Series uses a quad-core processor and is designed for high-speed rendering, operation, startup, communications and program transfer. Models are available in display sizes from 8.4 to 15 inches.

    The MONITOUCH V9 Series also supports advanced applications and offers models from 5.7 to 15 inches, with onboard Ethernet and SD-card slots standard across the series.

    HMI and edge-computing platform

    Some industrial HVAC applications need more than a conventional operator panel. A plant may want to collect information from multiple machines, run Windows-based applications or exchange data with IT and cloud systems.

    Fuji Electric’s MONITOUCH X1 Series combines HMI functionality with a Windows-based platform. It supports OPC UA server and client functions and can act as a gateway for field equipment that does not communicate directly through OPC UA. It also supports MQTT-based data exchange for appropriate connected applications.

    This type of platform may suit central utility plants, industrial cooling systems and facilities pursuing condition monitoring or broader digitalization. Its additional capabilities also bring greater configuration, patching and cybersecurity responsibilities.

    Verify communications before choosing hardware

    An HMI is useful only if it can communicate reliably with the controllers and devices in the HVAC system.

    Prepare a complete device list that identifies:

    • Manufacturer and model
    • Required protocol
    • Physical interface
    • Number of connections
    • Expected polling rate
    • Read and write points
    • Alarm and diagnostic data
    • Network architecture

    Potential connected devices include:

    • PLCs
    • HVAC controllers
    • Variable frequency drives
    • Temperature controllers
    • Power meters
    • Flow and pressure transmitters
    • Remote input/output
    • Chiller or boiler controllers
    • Building automation gateways

    Do not assume that an Ethernet port guarantees compatibility. Ethernet describes the network connection, not the application protocol. The HMI must have the correct driver for the controller or device.

    Likewise, confirm the precise protocol variant. Modbus RTU, Modbus TCP, BACnet MS/TP and BACnet/IP use different physical and communications arrangements. A gateway may be required when the HMI does not directly support the building-automation protocol used by the supervisory system.

    Fuji Electric MONITOUCH HMIs support connectivity to a broad range of PLCs and industrial devices, including more than 20 Ethernet drivers and multiple fieldbus options across the portfolio. Compatibility should still be checked for the exact HMI model, device and protocol version.

    Determine how many communications ports are needed

    Port count can affect both system performance and maintainability.

    An HVAC HMI may need to communicate simultaneously with:

    • A primary PLC
    • Several AC drives
    • A secondary controller
    • A supervisory network
    • A maintenance computer
    • Remote monitoring software

    Models with multiple Ethernet ports can help separate equipment communications from supervisory or maintenance traffic. Multiple serial ports may be useful when existing drives, meters or controllers use RS-232, RS-422 or RS-485.

    However, multiple ports do not automatically create secure network separation or routing. The intended network behavior should be verified with the manufacturer, and the system architecture should be reviewed by the project’s controls and cybersecurity teams.

    Also evaluate communication loading. Large point counts, short polling intervals and extensive data logging can create slow screen updates if processing and network capacity are insufficient.

    Choose the right screen size and resolution

    The best display is large enough to present information clearly without encouraging designers to crowd too much onto a single screen.

    Consider:

    • Viewing distance
    • Number of values shown simultaneously
    • Required trend detail
    • Operator age and visual accessibility
    • Available panel space
    • Whether gloves will be worn
    • Lighting and glare
    • Required touch-target size
    • Screen aspect ratio
    • Number of languages

    Small displays can work well for individual pieces of equipment. Larger screens are often appropriate for central plants, where operators need to compare several chillers, pumps or air-handling systems.

    Resolution matters as much as physical size. A higher-resolution screen can show more detail, but controls and text should remain large enough to use comfortably. Important commands should not be placed close together, where an operator could easily touch the wrong control.

    Avoid duplicating a full piping and instrumentation diagram on every screen. Start with an overview, then let users navigate to equipment, trends, alarms and maintenance details.

    Match the touchscreen to the operator

    Resistive and projected-capacitive touchscreens behave differently.

    Resistive touchscreen

    A resistive screen responds to physical pressure and can often be used with many types of gloves or a stylus. It is a familiar choice for industrial environments.

    Projected-capacitive touchscreen

    A projected-capacitive, or PCAP, screen can support a smooth, responsive interface and, in applicable configurations, multi-touch gestures. Glove compatibility depends on the glove material, thickness and panel settings.

    The correct choice depends on who will use the HMI and under what conditions. Test the intended gloves whenever possible. Also consider how water, condensation, dirt or cleaning procedures could affect touch operation.

    Regardless of screen technology, critical actions should require deliberate confirmation. For example, stopping a central chilled-water pump should not depend on one unconfirmed touch.

    Account for the operating environment

    An HMI mounted in a conditioned control room faces different conditions from one installed on an outdoor air handler or in a washdown area.

    Check the selected model’s ratings for:

    • Operating temperature
    • Storage temperature
    • Humidity
    • Condensation
    • Vibration and shock
    • Dust and water exposure
    • Ultraviolet exposure
    • Altitude
    • Hazardous-area classification
    • Electromagnetic compatibility

    The HMI’s front-panel rating applies only when it is correctly installed in a suitable enclosure using the specified gasket and mounting procedure. It does not necessarily mean the back of the unit can be exposed to the same conditions.

    Fuji Electric offers HMI configurations with front-panel protection ratings such as IP66 or NEMA 4X in applicable models. The exact environmental and certification requirements should be confirmed from the hardware specifications for the selected unit.

    Outdoor installations may require a sunshield, heater or enclosure cooling. Direct sunlight can raise internal temperature well above the reported ambient temperature and reduce screen visibility.

    Confirm the available power supply

    Determine whether the control panel provides 24 VDC or line-voltage AC power. Many industrial control systems favor 24 VDC because it can be supplied by a regulated control-power source or uninterruptible power supply.

    A short control-power interruption should not leave the HVAC equipment in an unsafe or indeterminate state. The controller, not the HMI, should retain responsibility for essential sequences. If the HMI restarts, it should reconnect automatically and display the actual equipment state rather than an assumed state.

    Check:

    • Nominal voltage and allowable variation
    • Maximum power consumption
    • Inrush requirements
    • Required overcurrent protection
    • Grounding
    • Ride-through or UPS requirements
    • Separation from electrically noisy circuits

    The HMI and communications equipment should be included in the panel’s heat-load calculation.

    Specify alarm management carefully

    More alarms do not necessarily create a safer or more useful HVAC system. Poorly configured HMIs can overwhelm operators with repeated or low-value notifications.

    Each alarm should have:

    • A clear name
    • A meaningful description
    • Priority
    • Timestamp
    • Current and acknowledged state
    • Related equipment
    • Likely cause
    • Recommended operator response

    Distinguish alarms from ordinary status messages. A fan being off because the system is unoccupied should not generate the same urgency as a fan failing to start during a cooling call.

    Useful alarm functions may include:

    • Current alarm view
    • Historical alarm log
    • Filtering by system or priority
    • First-out indication
    • Acknowledgment tracking
    • Audible notification
    • Alarm frequency or “bad actor” reports

    Preserve important alarm history through planned shutdowns and restarts where required.

    Evaluate trending and data storage

    Trend data can turn an HMI from a simple control panel into a valuable diagnostic tool.

    Useful HVAC trends include:

    • Supply and return temperatures
    • Differential pressure
    • Airflow and water flow
    • Valve and damper commands
    • Fan and pump speed
    • Drive output current or power
    • Filter differential pressure
    • Chiller loading
    • Equipment runtime
    • Dissolved or calculated performance metrics

    Define the sampling interval and retention period according to the process. A one-second interval may be appropriate for diagnosing an unstable control loop, while five- or fifteen-minute data may be sufficient for long-term energy analysis.

    Estimate storage needs instead of assuming that an SD card or internal memory will be sufficient. Determine how files will be retrieved, backed up and protected from corruption or unauthorized changes.

    Fuji Electric’s V9 Series includes SD-card interfaces across the product family, supporting local data storage and transfer in appropriate applications. 

    Build usability into the specification

    An HMI should make the system easier to operate under both normal and abnormal conditions.

    Effective HVAC screen design generally uses:

    • Consistent navigation
    • Plain equipment names
    • Standard colors and symbols
    • Clear engineering units
    • Visible operating modes
    • Actual and commanded values shown together
    • Limited use of animation
    • Color reserved for meaningful state changes
    • Large, well-spaced touch targets
    • Confirmation for consequential commands

    Do not rely on color alone. Pair colors with text, symbols or shapes so information remains understandable to users with color-vision deficiencies.

    Show why equipment is not operating. “Pump stopped” is less useful than “Pump stopped, schedule disabled,” “safety interlock open” or “failed to start.”

    The interface should also distinguish manual, automatic, local and remote control modes. Operators must be able to see which system currently has command authority.

    Apply role-based access

    Not every user should be able to change every value.

    A practical access structure might include:

    • View-only user
    • Operator
    • Maintenance technician
    • Controls specialist
    • Administrator

    Routine operators may be permitted to adjust comfort setpoints within approved limits but not modify motor parameters or safety-related thresholds. Maintenance users may need access to manual commands and diagnostic screens. Engineering-level configuration should be restricted further.

    Use individual credentials where the platform supports them. Shared passwords make it difficult to determine who changed a setting. Operation logs can support troubleshooting by recording commands and value changes.

    Also define how passwords will be created, stored, reset and removed when personnel change roles.

    Treat cybersecurity as a system requirement

    Any HMI connected to an Ethernet, wireless or enterprise network becomes part of the facility’s attack surface.

    Good practices include:

    • Change default credentials
    • Disable unused ports and services
    • Restrict write access
    • Separate operational technology from business networks
    • Use firewalls and controlled remote-access paths
    • Limit internet and cloud connectivity to approved use cases
    • Maintain an asset and firmware inventory
    • Back up HMI applications and configuration
    • Apply updates through a controlled process
    • Log administrative changes
    • Protect removable media

    CISA recommends separating operational technology and IT resources through logical or physical network segmentation.

    Wireless connectivity may simplify commissioning or maintenance, but it should be enabled only when the operational benefit justifies it and the facility has an approved security design.

    Plan for commissioning and lifecycle support

    HMI selection should include the engineering software and long-term support model, not only the physical panel.

    Before purchase, confirm:

    • Availability of configuration software
    • License requirements
    • Supported engineering-computer operating systems
    • Ability to import or convert existing applications
    • Backup and restore procedures
    • Replacement-model strategy
    • Availability of CAD files and documentation
    • Technical support
    • Expected product lifecycle
    • Availability of spare units

    During commissioning, test:

    • Every command and status point
    • Loss and restoration of each communications link
    • Controller and HMI power cycling
    • Alarm generation, acknowledgment and history
    • User-access levels
    • Trend accuracy
    • Units and scaling
    • Manual and automatic control transitions
    • Remote-access behavior
    • Backup restoration

    Leave the facility with an editable application, documented credentials, communication settings, firmware records and a verified backup.

    HMI selection checklist

    Before specifying an HVAC HMI, confirm:

    1. What equipment and processes will it display and control?
    2. Is the HMI local, supervisory or an edge-computing platform?
    3. How many devices, tags, screens and trends are required?
    4. Which exact communications protocols and drivers are needed?
    5. How many Ethernet and serial interfaces are required?
    6. What screen size and resolution suit the viewing distance?
    7. Will operators wear gloves?
    8. What temperature, moisture, dust and vibration ratings are required?
    9. Is 24 VDC or AC power available?
    10. How much alarm and trend history must be retained?
    11. What user roles and audit records are required?
    12. How will the HMI be segmented and secured?
    13. Can the application be backed up and restored easily?
    14. Is the platform supported over the expected system life?

    Select for the people as well as the equipment

    The right HMI connects operators to the information that matters without adding unnecessary complexity. It should communicate with every required device, withstand the installation environment and remain understandable during both routine operation and urgent troubleshooting.

    Fuji Electric’s MONITOUCH portfolio includes basic TECHNOSHOT panels, V9 and high-speed V10 HMIs, and the Windows-based X1 platform for applications requiring broader IT and operational-technology connectivity.

    By defining the users, functions, devices and environment before selecting a model, HVAC designers can create an interface that improves visibility, simplifies maintenance and supports dependable system operation.

  • How to Specify the Right AC Drives for Data Center Cooling

    How to Specify the Right AC Drives for Data Center Cooling

    Data center cooling is entering a new era. Higher rack densities, accelerated computing and the growing use of liquid cooling are placing greater demands on chilled-water pumps, condenser-water pumps, cooling-tower fans, air-handling units and coolant distribution units.

    AC drives, also known as variable frequency drives, or VFDs, allow these systems to adjust motor speed as cooling demand changes. When properly specified, they can improve energy efficiency, strengthen control and reduce mechanical stress. When poorly matched to the application, however, they can introduce reliability, power-quality and integration problems.

    The right selection process therefore goes beyond matching a drive’s horsepower to the motor nameplate. Engineers should evaluate the complete cooling system, its operating environment and the data center’s availability requirements.

    1. Start with the cooling application

    First, identify what the drive will control and how that equipment behaves under real operating conditions. Common applications include:

    • Chilled-water and condenser-water pumps
    • Cooling-tower fans
    • CRAH and air-handling-unit fans
    • Dry coolers and fluid coolers
    • Pumps in coolant distribution units
    • Other secondary cooling-loop pumps

    Centrifugal fans and pumps are especially well suited to variable-speed control. Their power requirement falls rapidly as speed is reduced. As a general illustration, the U.S. Department of Energy notes that a 10% reduction in speed can produce approximately a 30% reduction in power for centrifugal pumps, fans and compressors, depending on the system.

    Actual savings depend on the system curve, static head, operating hours, control sequence and part-load profile. Engineers should use the expected load profile, not simply the design-day condition, to estimate drive size, energy performance and potential return on investment.

    For pumps, confirm the required flow and pressure across every operating mode. For fans, evaluate airflow, static pressure and the minimum speed needed for stable operation. Compressor applications require additional care and should use a drive and control strategy approved for the specific compressor technology.

    2. Size the drive by current and duty, not horsepower alone

    Motor horsepower is a useful starting point, but output-current capability is the more important selection criterion. Compare the motor’s full-load current with the drive’s continuous output-current rating at the actual site conditions.

    The specification should address:

    • Motor voltage, frequency and full-load current
    • Number and type of motors connected
    • Variable-torque or constant-torque duty
    • Required starting and accelerating torque
    • Expected maximum and minimum speeds
    • Acceleration and deceleration times
    • Potential overloads or process transients
    • Whether the motor may operate above base speed

    Most centrifugal cooling fans and pumps are variable-torque loads. A drive rated for variable-torque duty can often provide the appropriate performance without the cost and footprint associated with a heavier constant-torque rating. Applications with unusually high starting torque, rapid acceleration or frequent load changes may require additional capacity.

    Avoid oversizing “just in case.” A substantially oversized drive can increase cost, occupy more panel space and operate less effectively at very light loads. Where future capacity is anticipated, define that expansion explicitly and select both the motor and drive around the planned duty point.

    3. Account for the installation environment

    Published ratings apply under stated environmental conditions. Data center mechanical spaces can exceed those assumptions, particularly in rooftop equipment, crowded electrical rooms and enclosed pump skids.

    Check:

    • Maximum and minimum ambient temperature
    • Installation altitude
    • Humidity and condensation risk
    • Dust, water and contaminant exposure
    • Indoor or outdoor location
    • Enclosure type and cooling method
    • Required clearances and ventilation
    • Heat released into the electrical room

    Apply the manufacturer’s required derating for temperature, altitude, enclosure type and switching conditions. Do not treat thermal management as an afterthought: the drive itself produces heat, and that heat must be included in room and enclosure cooling calculations

    Fuji Electric’s FRENIC-MEGA (G2) platform, for example, is offered across 208/230 V, 460 V and 575 V classes, with enclosure and derating requirements that vary by rating and installation. The current specification sheet should always be consulted during final selection. 

    4. Define the control strategy before selecting features

    A drive should support the intended sequence of operations without unnecessary external hardware. Useful functions for data center cooling can include:

    • PID control for pressure, temperature or flow
    • Sleep and wake functions
    • Minimum- and maximum-speed limits
    • Controlled acceleration and deceleration
    • Flying start for a motor that is already rotating
    • Automatic restart after a permitted interruption
    • Pump alternation or staging
    • Broken-belt, loss-of-load or dry-pump detection
    • Skip frequencies to avoid mechanical resonance
    • Real-time scheduling
    • Local and remote operating modes

    The control narrative should also describe sensor failure, loss of communication and controller failure. In a mission-critical cooling system, the safest fallback may be a predefined speed rather than an immediate stop. That decision should be made through a system-level risk assessment.

    Multiple sensors may be required where a single pressure or temperature reading cannot accurately represent cooling demand. Stable sensor placement and sensible PID tuning are just as important as the drive hardware; an unstable loop can cause hunting, excess energy use and premature equipment wear.

    5. Integrate the drive with the building management system

    Cooling equipment rarely operates in isolation. Drives should exchange meaningful information with the building management system, electrical power monitoring system or supervisory cooling controls.

    Define the required communications protocol and points list during design. Typical data points include:

    • Run and ready status
    • Speed command and feedback
    • Output frequency and current
    • Power and energy
    • Alarm and fault codes
    • Operating hours
    • Local/remote status
    • Maintenance indicators

    Fuji Electric’s FRENIC-MEGA (G2) includes RS-485/Modbus and supports common building-automation connectivity, including BACnet MS/TP and Metasys N2. [2] Confirm the exact protocol, interface hardware and point mapping required for each project.

    Hardwired enable, run-status and critical-alarm signals may still be appropriate even when network communications are used. This gives essential functions a path that does not depend entirely on the control network.

    6. Address harmonics, electromagnetic compatibility and motor protection

    AC drives are nonlinear loads, so their cumulative effect on the electrical system must be evaluated. A data center may contain dozens or hundreds of drives alongside UPS systems, power supplies and other power-electronic equipment.

    The design team should assess:

    • Harmonic distortion at the point of common coupling
    • Applicable project or utility power-quality limits
    • Input reactors, DC-link reactors or harmonic filters
    • Electromagnetic interference
    • Grounding and cable shielding
    • Motor-cable length
    • Reflected-wave voltage at the motor
    • Common-mode current and bearing-current risk

    Long motor leads can increase voltage stress on motor insulation. Depending on cable length, motor design and switching conditions, an output reactor, dV/dt filter or sine-wave filter may be needed. Inverter-duty motors and appropriate insulation systems should be considered, especially for higher voltages, long conductors or continuous low-speed operation.

    Liquid-cooling systems deserve particular attention because drives used with coolant distribution unit pumps can add to harmonic distortion. ASHRAE identifies power quality as one of the issues to consider when modernizing facilities for higher-density and liquid-cooled computing.

    A project-level harmonic study is preferable to specifying mitigation devices independently for every drive. The study can identify the most effective combination of drive topology, reactors, filters and system impedance.

    7. Engineer for availability and maintainability

    Not every cooling motor requires the same redundancy strategy. The appropriate design depends on the facility topology, such as N, N+1, 2N or distributed redundancy.

    Key questions include:

    • Can another fan or pump carry the load if this unit is unavailable?
    • Is a bypass required?
    • Will bypass operation provide useful cooling without variable-speed control?
    • Can the drive be isolated and replaced safely?
    • Are critical spares available on site?
    • Can one drive rating serve several standardized motor sizes?
    • How quickly can trained support be reached?

    A bypass is not automatically the best answer. It adds components, wiring and failure modes, while operating a fan or pump at full speed may disrupt pressure or flow control. In systems with equipment-level redundancy, a spare drive or quick-replacement strategy may provide a cleaner solution. The choice should follow a failure-mode analysis of the cooling architecture.

    Specifications should also require accessible fault histories, replaceable cooling fans where applicable, clear diagnostic information and retention or backup of parameter settings.

    8. Coordinate protection and emergency behavior

    The drive, motor, upstream protective device and control system must be coordinated as one assembly. Define short-circuit protection, disconnecting means, branch-circuit requirements, ground-fault behavior and any safety or fire-alarm interfaces in accordance with the applicable codes and project standards.

    Also document what should happen after:

    • A brief voltage dip
    • Complete power loss
    • Generator transfer
    • Loss and restoration of a control signal
    • Fire-alarm activation
    • Emergency power-off
    • Motor or sensor failure

    Automatic restart can help restore cooling quickly, but it must be applied only where restarting machinery is safe and permitted. Restart delays may need to be staggered to prevent a large block of cooling equipment from returning simultaneously after a power event.

    9. Specify commissioning, not just equipment

    Even a correctly selected drive can underperform if it is commissioned with default parameters. The project specification should include:

    • Verification of motor nameplate data
    • Direction-of-rotation checks
    • Minimum- and maximum-speed settings
    • Acceleration and deceleration tuning
    • PID-loop tuning
    • Resonance checks
    • Sensor-loss and communications-loss tests
    • Alarm and restart testing
    • BMS point-to-point verification
    • Measurement at representative load conditions
    • Backup of the final parameter set
    • Operator and maintenance training

    Trend speed, current, power, pressure, flow and temperature during functional testing. This provides evidence that the cooling loop is stable and creates a baseline for future condition monitoring.

    A system-level selection

    The best AC drive is not necessarily the one with the highest power rating or longest feature list. It is the one that fits the motor, load profile, electrical system, control architecture, environment and availability strategy.

    Fuji Electric offers AC drives for the fans and pumps used throughout data center cooling systems, with products spanning fractional through high-horsepower applications. The FRENIC-MEGA (G2) series is designed specifically for fan and pump control, while the broader FRENIC portfolio provides additional choices for varied performance and capacity requirements.

    By involving the drive manufacturer early, and treating the drive as part of the complete cooling and power system, designers can achieve responsive control, dependable operation and better lifetime energy performance.

  • What Is a Battery String and How Should It Be Configured for Commercial UPS Systems?

    What Is a Battery String and How Should It Be Configured for Commercial UPS Systems?

    A commercial uninterruptible power supply is only as dependable as its stored-energy system. When utility power fails, the UPS battery must immediately support the inverter and keep the critical load operating until power returns, a generator starts, or equipment can shut down safely.

    In medium and large UPS installations, that energy is commonly supplied by one or more battery strings. The way those strings are configured affects DC-bus voltage, runtime, fault current, maintenance flexibility, battery life, and system availability.

    Getting the configuration right requires more than connecting enough batteries to achieve a desired voltage. The batteries, conductors, protective devices, charger, monitoring system, and UPS must be designed as one coordinated system.

    What Is a Battery String?

    A battery string is a group of battery cells or monoblocs connected in series.

    In a series connection, the positive terminal of one battery is connected to the negative terminal of the next. The individual battery voltages add together to create the DC voltage required by the UPS.

    For example, connecting forty 12-volt batteries in series creates a nominal string voltage of:

    40 batteries × 12 volts = 480 VDC nominal

    The actual string voltage will vary with battery chemistry, state of charge, charging mode, temperature, load, and battery condition.

    The string’s ampere-hour capacity does not add in a series connection. If each battery is rated at 100 Ah, the complete series string is nominally a 480-volt, 100-Ah battery string, not a 4,000-Ah string.

    Commercial UPS systems may use long strings operating at several hundred volts DC. Vertiv documentation, for example, describes UPS strings made from series-connected batteries and warns that complete string voltage can reach potentially lethal levels. Installation and maintenance must therefore be performed by qualified personnel using the applicable electrical-safety procedures. 

    Series Determines Voltage

    The number of cells or battery blocks in series is selected to match the DC input range of the UPS.

    That number is not arbitrary. The UPS manufacturer establishes limits for:

    • Nominal battery voltage
    • Minimum discharge voltage
    • Maximum charging voltage
    • Permitted number of cells or blocks
    • Battery chemistry
    • Charger capacity
    • Battery-test functions
    • DC overcurrent protection
    • Runtime configuration

    Too few batteries may allow the DC voltage to fall below the inverter’s minimum operating threshold before the batteries have delivered their intended capacity.

    Too many batteries may exceed the UPS, charger, capacitor, switching-device, or insulation rating, especially during charging, when string voltage is higher than nominal.

    The correct series count must therefore come from the approved UPS and battery documentation. It should not be changed merely to obtain a different runtime.

    Parallel Strings Determine Capacity and Runtime

    When one series string cannot provide the required runtime or current, complete strings may be connected in parallel.

    In a parallel arrangement:

    • Each string has the same nominal voltage.
    • The available ampere-hour capacity increases.
    • Current is shared among the strings.
    • Potential runtime increases.
    • Available DC fault current also increases.

    Two identical 480-volt, 100-Ah strings connected in parallel form a nominal 480-volt, 200-Ah battery bank. The voltage remains 480 volts because the strings are paralleled, while the capacity increases.

    This relationship can be summarized simply:

    • Batteries in series increase voltage.
    • Complete strings in parallel increase capacity and current capability.

    Actual runtime will not necessarily double when the number of strings doubles. Battery discharge rate, age, temperature, UPS efficiency, cell cutoff voltage, load level, and conductor losses all influence usable runtime.

    Build Every Parallel String the Same Way

    Parallel strings should be electrically equivalent.

    Each string should normally have the same:

    • Number of cells or monoblocs
    • Battery manufacturer and model
    • Chemistry
    • Nominal capacity
    • Age and service history
    • Temperature exposure
    • Connection method
    • Conductor size
    • Approximate cable length
    • Protective-device arrangement

    If one string has lower resistance, it may supply more discharge current and accept more charging current than the others. That string can run hotter and age faster, increasing the imbalance further.

    Equal-length, equal-size cabling helps keep the resistance of the parallel branches similar. EnerSys specifically recommends using the same cable size and approximately the same cable length for each parallel string so that string resistance remains comparable. EnerSys UPS Battery Quick Start Guide

    A balanced bus arrangement is also important. Connecting the UPS positive and negative leads in a way that favors the physically closest string can create unequal current paths. Commercial battery systems commonly use a properly designed common bus or coordinated connection geometry to achieve better sharing.

    Do Not Mix Unlike Batteries

    Installing new batteries into an aged string may look economical, but it can create an electrically mismatched system.

    An older battery may have:

    • Lower capacity
    • Higher internal resistance
    • Greater self-discharge
    • Different charge acceptance
    • Different terminal voltage under load

    In a series string, every battery carries the same current. A weak battery can therefore reach its discharge limit before the rest of the string, restricting the capacity of the entire string.

    During charging, voltage can also divide unevenly. A deteriorated unit may become overcharged or undercharged even when total string voltage appears normal.

    Mixing different capacities, models, chemistries, or ages can make these problems worse. Unless the battery and UPS manufacturers provide a specific approved procedure, replacement should generally be performed at the complete-string or complete-bank level rather than by casually mixing dissimilar units.

    Why the Weakest Battery Matters

    Series-connected batteries carry the same current, but they do not necessarily have the same capacity or terminal voltage.

    Suppose one battery in a long string has lost substantial capacity. During a discharge, that battery may reach a dangerously low voltage before the others. The UPS sees only total string voltage unless battery-level monitoring is installed, so the problem may remain hidden until runtime is needed.

    A weak unit can cause:

    • Reduced backup time
    • Premature low-battery shutdown
    • Excessive voltage imbalance
    • Localized heating
    • Reversal of a severely depleted cell
    • Failed battery tests
    • Unexpected loss of the entire string

    This is why total string voltage alone is not a sufficient measure of battery health.

    Protect Each Parallel String Individually

    When several strings share a DC bus, each string should have appropriately engineered isolation and overcurrent protection.

    Depending on the UPS design, this may include a:

    • Battery circuit breaker
    • Fused disconnect
    • Battery disconnect cabinet
    • Manufacturer-designed internal breaker
    • Contactor coordinated with the UPS protection system

    Individual protection serves several purposes:

    • Isolates a faulted string
    • Protects string conductors
    • Allows maintenance on one string
    • Prevents healthy strings from feeding excessive current into a failed parallel branch
    • Provides a visible or controlled means of disconnection

    Vertiv guidance states that parallel strings should be equipped with disconnecting means so maintenance on one string does not interfere with the others. It also recommends locating the battery circuit breaker close to the battery terminals and minimizing connection distance. Vertiv Liebert EXM UPS user manual

    Protection must be rated for DC operation at the maximum possible system voltage and fault current. An AC-only breaker is not automatically suitable because interrupting DC presents different arc-extinguishing requirements.

    Protective-device sizing and coordination must follow the UPS manufacturer’s instructions, the battery manufacturer’s limits, the engineered design, and applicable codes.

    More Parallel Strings Are Not Always Better

    Adding strings can increase runtime, but it also changes the electrical system.

    Potential consequences include:

    • Greater prospective fault current
    • More complex protection coordination
    • Increased charger demand
    • Longer recharge time
    • More connections that can loosen or corrode
    • Greater monitoring and maintenance burden
    • More difficult current sharing
    • Increased floor-space and structural requirements

    The UPS may also impose a maximum supported number of strings or external battery modules. Eaton, for example, publishes product-specific limits and requires equal external-battery-module quantities for UPS units in certain parallel arrangements to maintain equivalent runtimes. Eaton 9155 Parallel UPS user guide

    The permissible number of strings must be verified for the exact UPS model rather than estimated from charger voltage alone.

    Charger Capacity Must Match the Battery Bank

    A larger battery bank requires more energy to recharge.

    If parallel strings are added without considering charger capacity, the UPS may still operate but require an unacceptably long time to restore full charge after a discharge. This creates a period in which another outage could occur before the system has recovered its intended runtime.

    The charger must also maintain the batteries at the correct voltage for their chemistry and temperature. Excessive charge voltage can accelerate corrosion, water loss, gas generation, or thermal problems. Insufficient voltage can leave the battery undercharged and promote capacity loss.

    Configuration should account for:

    • Battery chemistry
    • Total bank capacity
    • Desired recharge time
    • Maximum charger current
    • UPS auxiliary loads
    • Generator compatibility
    • Temperature compensation
    • Manufacturer charging limits

    Recharge performance should be evaluated following the design discharge, not just after a brief self-test.

    Runtime Is Not Simply Ampere-Hours Divided by Amps

    A rough energy estimate can be useful:

    Nominal energy = nominal string voltage × ampere-hour capacity

    However, this does not equal the energy available to the load.

    Usable runtime is affected by:

    • Discharge rate
    • Battery terminal-voltage curve
    • UPS low-voltage cutoff
    • Battery age
    • Temperature
    • Inverter efficiency
    • DC-cable voltage drop
    • Battery imbalance
    • Required end-of-life margin
    • Actual critical load

    Lead-acid capacity is particularly dependent on discharge rate. A battery rated over a long discharge period may deliver less than its nominal ampere-hour rating during a high-rate UPS discharge.

    The correct approach is to use manufacturer discharge data or approved sizing software at the required load, end voltage, temperature, aging factor, and runtime.

    Configure for End-of-Life Performance

    A new battery bank should normally provide more than the bare minimum required runtime. Batteries lose capacity as they age, so a system sized to meet the requirement only on its first day may fall short well before its planned replacement date.

    A sound design considers:

    • Required runtime at end of life
    • Battery aging factor
    • Lowest expected battery-room temperature
    • Future load growth
    • UPS conversion losses
    • Design margin
    • Generator start and stabilization time
    • Shutdown requirements if generation fails

    Excessive oversizing has drawbacks, including cost, footprint, fault current, and recharge time. The goal is a justified margin, not unlimited capacity.

    Temperature Strongly Affects Battery Performance

    Battery-room temperature influences both available capacity and service life.

    Low temperature generally reduces immediate discharge capacity. High temperature may temporarily improve available capacity but accelerates aging and can shorten service life significantly.

    Strings connected in parallel should experience similar temperatures. A string near an air-conditioning outlet and another beside a warm UPS cabinet may age differently even if they were installed at the same time.

    Good thermal design includes:

    • Uniform airflow
    • Avoidance of local hot spots
    • Temperature monitoring
    • Suitable ventilation
    • Separation from heat-producing equipment where practical
    • Charger temperature compensation when specified
    • Alarm thresholds for abnormal conditions

    Temperature sensors should be positioned according to the manufacturer’s guidance rather than simply placed at the coolest point in the room.

    VRLA, Flooded Lead-Acid, and Lithium-Ion Strings

    The meaning of a string remains similar across battery chemistries, but configuration and protection requirements differ.

    Valve-regulated lead-acid

    VRLA batteries are common in commercial UPS systems because they are compact and require less routine electrolyte maintenance than flooded cells. They remain sensitive to temperature, charging conditions, connection quality, and aging.

    Flooded lead-acid

    Flooded batteries may offer long service life and detailed cell-level inspection opportunities, but they require appropriate rooms, ventilation, spill management, maintenance access, and electrolyte procedures.

    Lithium-ion

    Lithium-ion UPS systems typically use modules combined into controlled strings with a battery-management system. The BMS monitors conditions such as cell voltage, temperature, current, and contactor state.

    Lithium-ion modules should not be treated as interchangeable substitutes for lead-acid blocks. Charger behavior, communication, protection, fault response, and UPS compatibility must be specifically approved.

    Battery Monitoring Should Go Below the String Level

    Useful battery monitoring may include:

    • Total string voltage
    • Individual cell or monobloc voltage
    • String current
    • Float current
    • Internal resistance or conductance trends
    • Battery temperature
    • Ambient temperature
    • Ground-fault or insulation status
    • Breaker position
    • Connection resistance
    • State of charge
    • Discharge history

    The most useful diagnostic information often comes from comparison and trending. One battery that gradually diverges from the rest may be more significant than an isolated reading that remains within a broad limit.

    Monitoring does not replace inspection, testing, or maintenance. It helps identify where closer investigation is needed.

    Common Configuration Mistakes

    Incorrect number of batteries in series

    This can place the DC bus outside the UPS charging or operating range.

    Unequal parallel strings

    Different battery models, capacities, ages, or conductor resistance can produce uneven current sharing.

    No individual string isolation

    A faulted string may be fed by the remaining strings, and maintenance may require taking the entire battery bank out of service.

    Adding strings without checking the charger

    Runtime may increase, but recharge time may become unacceptable.

    Sizing from nominal ampere-hours alone

    This overlooks discharge rate, cutoff voltage, temperature, aging, and UPS efficiency.

    Assuming equal voltage means equal health

    Parallel strings can show the same terminal voltage while having very different capacity or internal resistance.

    Replacing only visibly failed units

    The remaining batteries may be near the same wear-out condition, leading to repeated failures and continued imbalance.

    Ignoring cable resistance

    Unequal cable lengths, conductor sizes, or termination quality can cause unequal loading.

    Mixing battery chemistries

    Different chemistries require different charging, monitoring, and protective behavior.

    Closing a battery breaker without checking voltage and polarity

    A voltage mismatch or reversed connection can produce extreme current and catastrophic damage.

    Commissioning a Commercial UPS Battery Bank

    A formal commissioning process should verify both the design and the installation.

    Typical checks include:

    1. Confirm the approved battery model, chemistry, quantity, and series count.
    2. Verify that every parallel string has the same configuration.
    3. Inspect batteries for shipping or installation damage.
    4. Confirm polarity at the battery, string, cabinet, and UPS connections.
    5. Measure individual battery and complete-string voltages.
    6. Compare open-circuit voltage spread before final connection.
    7. Verify cable size, routing, identification, and approximate branch equality.
    8. Confirm terminal torque using the battery manufacturer’s specified values.
    9. Check barriers, terminal covers, grounding, ventilation, and working clearances.
    10. Verify each string’s protective device and DC interrupting rating.
    11. Confirm UPS battery settings, capacity, cell count, and charging parameters.
    12. Check monitoring and temperature sensors.
    13. Verify breaker-status and alarm signals.
    14. Perform manufacturer-approved functional and runtime testing.
    15. Record baseline voltage, temperature, resistance, and conductance data.

    The EnerSys commissioning guidance emphasizes checking voltage spread, using clean contact surfaces, applying specified terminal torque, confirming string voltage, and establishing the correct charge conditions before service. EnerSys UPS Battery Quick Start Guide

    Safe Maintenance Requires More Than Opening the UPS Input

    Turning off the AC supply does not necessarily remove the battery hazard. The battery bank remains an energized DC source capable of delivering very high current.

    Even when a battery breaker is open, hazardous voltage may remain inside individual strings or across sections of the bank.

    Maintenance planning should address:

    • Lockout and isolation
    • Verification of voltage
    • DC-rated test equipment
    • Insulated tools
    • Appropriate personal protective equipment
    • Removal of conductive jewelry
    • Protection against accidental short circuits
    • Correct lifting and handling
    • Chemical and fire hazards
    • Manufacturer-prescribed procedures
    • Qualified-person requirements

    Battery strings must never be treated as safe solely because the UPS display is off.

    A Practical Configuration Example

    Assume a UPS requires a nominal 480 VDC battery input and the approved design uses 12-volt, 100-Ah battery blocks.

    One string would contain:

    480 V ÷ 12 V per battery = 40 batteries in series

    That creates one nominal:

    480 V, 100 Ah string

    If the approved runtime calculation requires 300 Ah, the design might use three identical strings in parallel:

    3 strings × 100 Ah = 300 Ah nominal bank capacity

    The resulting bank would contain:

    • 40 batteries per string
    • 3 parallel strings
    • 120 batteries total
    • 480 VDC nominal bank voltage
    • 300 Ah nominal capacity

    Each string would require coordinated conductors and suitable isolation and overcurrent protection. The charger, UPS configuration, bus, cabinet, monitoring, ventilation, and fault-current rating would all need to support the three-string arrangement.

    This example illustrates the electrical relationships; it is not a substitute for manufacturer-approved sizing.

    The Bottom Line

    A battery string is a series-connected group of batteries that supplies the DC voltage required by a commercial UPS. Connecting complete, identical strings in parallel increases capacity and potential runtime without increasing nominal bank voltage.

    A reliable configuration follows several core principles:

    • Use the UPS manufacturer’s approved battery type and series count.
    • Keep parallel strings electrically and thermally equivalent.
    • Avoid mixing different models, capacities, ages, or chemistries.
    • Give each string suitable DC-rated protection and isolation.
    • Balance conductor resistance among parallel branches.
    • Verify charger capacity and recharge time.
    • Size runtime using real discharge data and end-of-life conditions.
    • Monitor individual batteries as well as the complete string.
    • Treat the battery bank as an energized high-voltage source at all times.

    The best battery-bank design is not simply the arrangement with the most batteries. It is the configuration that delivers the required end-of-life runtime, shares current predictably, isolates faults safely, can be maintained without unnecessary risk, and remains fully compatible with the UPS that depends on it.

  • Understanding MCCB Operation, Failure Modes, and Diagnostic Indicators

    Understanding MCCB Operation, Failure Modes, and Diagnostic Indicators

    Molded-case circuit breakers are often treated as simple on-off devices. Under normal conditions, they carry current. During an overload or short circuit, they trip. When a breaker begins opening unexpectedly, or fails to open when it should, the investigation can quickly become more complicated.

    An MCCB is both a mechanical switching device and a protective device. Its performance depends on contacts, springs, latches, conductors, terminals, sensors, and the trip unit working together. Understanding those parts makes it easier to distinguish a genuine electrical fault from a damaged breaker, poor connection, incorrect setting, or application problem.

    What Is an MCCB?

    A molded-case circuit breaker, or MCCB, protects electrical conductors and equipment against excessive current. Its components are enclosed in an insulating molded housing, and many MCCBs also provide a means of manually isolating a circuit.

    Compared with miniature circuit breakers, MCCBs typically support higher current ratings, greater interrupting capacities, and more adjustable protection options. They are widely used in industrial switchboards, distribution panels, motor-control systems, generators, HVAC equipment, and commercial facilities.

    Depending on its design, an MCCB may protect against:

    • Long-duration overloads
    • Short circuits
    • Ground faults
    • Phase imbalance or phase loss
    • Other abnormal conditions detected by an electronic trip unit

    Not every breaker provides every protective function. The installed trip unit and its settings determine what the device can detect.

    How an MCCB Interrupts Current

    When an MCCB detects a fault, its trip mechanism releases a stored-energy operating mechanism. The contacts separate rapidly, even if an operator holds the handle in the ON position. This “trip-free” behavior prevents the breaker from being forced closed during a fault.

    Opening contacts create an electrical arc. The breaker directs that arc into an arc chute, where metal plates divide, cool, and lengthen it until the current is interrupted.

    The breaker must contain the thermal and mechanical energy produced during this event. Its interrupting rating therefore matters just as much as its continuous-current rating. A breaker applied where the available fault current exceeds its rating may fail catastrophically instead of safely clearing the fault.

    Thermal-Magnetic and Electronic Trip Units

    MCCBs generally use either thermal-magnetic or electronic trip technology.

    Thermal overload protection

    A thermal element responds to sustained overcurrent. Current heats a bimetallic component, causing it to bend until the trip mechanism releases.

    The response is intentionally time-dependent. A moderate overload may take seconds or minutes to trip the breaker, while a heavier overload produces a faster response. Ambient temperature, enclosure temperature, loading history, and airflow can influence thermal behavior.

    Magnetic short-circuit protection

    A magnetic element responds quickly to high fault current. When current exceeds its pickup level, electromagnetic force operates the trip mechanism with little intentional delay.

    This function protects the circuit against severe short circuits rather than ordinary operating overloads.

    Electronic protection

    An electronic trip unit uses current sensors and digital or analog electronics to evaluate current. Depending on the model, it may provide adjustable:

    • Long-time pickup and delay
    • Short-time pickup and delay
    • Instantaneous pickup
    • Ground-fault pickup and delay

    Advanced trip units may also record event data, identify the cause of a trip, measure electrical quantities, and communicate with a monitoring system.

    What the Handle Position Means

    Many MCCBs have three handle positions:

    • ON: The contacts are commanded closed.
    • OFF: The breaker has been opened manually.
    • TRIPPED: The protective or trip mechanism has operated.

    The tripped position is normally between ON and OFF. To reset the breaker, the handle must usually be moved fully to OFF before it can be moved back to ON.

    A breaker that will not reset may still be receiving a trip command, may have an attached interlock or undervoltage device preventing closure, or may have internal mechanical damage. Repeatedly forcing the handle is not a valid diagnostic method.

    Common MCCB Failure Modes

    Loose or high-resistance connections

    Loose terminals, poor crimps, damaged conductors, contamination, and incorrect hardware can create resistance at a connection. The resulting heat may discolor insulation, oxidize metal, weaken spring pressure, and damage the breaker body.

    Because heating is proportional to the square of current multiplied by resistance, even a modest increase in connection resistance can become serious under heavy load.

    Typical indicators include:

    • One terminal hotter than comparable phases
    • Discolored or melted insulation
    • Burned odor
    • Oxidation around the lug
    • Deformed breaker housing
    • Abnormal voltage drop across the connection

    A hot terminal does not automatically prove that the breaker itself is defective. The conductor preparation, lug, torque, loading, and installation method all require inspection.

    Contact erosion and overheating

    Every interruption produces some contact wear. High fault currents, frequent switching, contact bounce, and improper application can accelerate erosion.

    Damaged contacts may develop increased resistance, leading to additional heating during normal operation. Internal contact condition is not always visible without disassembly, and many MCCBs are not intended to be field-serviced internally.

    Possible indicators include:

    • Abnormal temperature rise through the breaker
    • Excessive voltage drop across a closed pole
    • Crackling or arcing sounds
    • Burning odor
    • Visible smoke or case damage
    • Uneven phase temperatures under balanced loading

    Nuisance or unexplained tripping

    An unexpected trip is not necessarily a nuisance trip. The breaker may be correctly responding to a condition that has not yet been identified.

    Possible causes include:

    • Sustained overload
    • Motor starting current
    • Transformer inrush
    • Capacitor energization
    • Harmonic current
    • High ambient temperature
    • Incorrect trip settings
    • Ground leakage
    • Intermittent short circuit
    • Loose connection
    • Failing load equipment
    • Poor coordination with downstream protection

    The trip curve and actual current profile must be compared. Looking only at steady-state current can miss brief starting or inrush events.

    Failure to trip

    A breaker that fails to operate during a fault presents a severe safety risk. Causes may include a seized mechanism, damaged trip unit, incorrect settings, contamination, corrosion, improper maintenance, misapplication, or internal damage from a previous interruption.

    This condition may not be visible during normal operation. Periodic inspection and testing are therefore critical where reliability requirements or applicable standards demand them.

    Failure to close or remain closed

    An MCCB may refuse to close because:

    • It has not been fully reset
    • A fault remains on the circuit
    • An undervoltage release is not energized
    • A shunt-trip signal remains active
    • A mechanical interlock is engaged
    • The operating mechanism is damaged
    • An accessory is incorrectly installed or wired

    If the breaker trips immediately after closing, the circuit should be treated as faulted until testing establishes otherwise.

    Insulation deterioration

    Heat, moisture, contamination, conductive dust, chemicals, age, and electrical stress can weaken insulation. Carbonized tracking paths may eventually support surface current or arcing.

    Warning signs include:

    • Cracks in the molded case
    • Carbon deposits
    • Surface tracking
    • Moisture or contamination
    • Evidence of flashover
    • Reduced insulation resistance
    • Ground-fault operation

    A cracked, carbonized, or arc-damaged case generally calls for replacement rather than cosmetic cleaning.

    Internal mechanical wear

    Springs, pivots, latches, and linkages can wear, corrode, or seize. Breakers that operate infrequently may still develop problems because of contamination or hardened lubrication.

    Indicators may include:

    • A handle that feels unusually loose or stiff
    • Incomplete movement
    • Failure to latch
    • Delayed or inconsistent operation
    • A pole that does not open or close with the others

    Mechanical concerns should be evaluated using manufacturer-approved procedures. Operating a suspect breaker repeatedly can make the condition worse.

    Diagnostic Indicators That Matter

    Trip-unit information

    Electronic trip units may display LEDs, fault codes, target indicators, current values, or stored event records. This information should be captured before control power is removed or the breaker is reset, because resetting may clear useful evidence.

    Important data can include:

    • Trip type
    • Fault magnitude
    • Affected phase
    • Time and date
    • Ground-fault level
    • Pre-trip current
    • Breaker operation count

    Temperature patterns

    Thermal imaging can identify abnormal heating while equipment is energized and under meaningful load. The pattern matters more than temperature alone.

    Useful comparisons include:

    • Incoming versus outgoing terminals
    • One phase versus the other phases
    • The breaker versus adjacent breakers carrying similar loads
    • Current temperature versus earlier inspection records

    Temperature must be interpreted in context. Load current, ambient temperature, emissivity, enclosure conditions, airflow, and phase imbalance all affect the reading.

    Voltage drop

    Measuring voltage drop across each closed pole can reveal high-resistance paths. Comparing poles under similar current is often more useful than considering one measurement in isolation.

    Because this test involves energized equipment, it should only be conducted under an appropriate electrical-safety program by qualified personnel using properly rated instruments and protective equipment.

    Sound, smell, and appearance

    Crackling, buzzing, burning odor, discoloration, soot, blistering, and deformation are significant warning signs. Equipment displaying evidence of active arcing, severe overheating, or case damage should not be repeatedly operated for troubleshooting.

    Visual inspection should also check for:

    • Loose or missing hardware
    • Incorrect conductor size
    • Improperly seated accessories
    • Contamination
    • Corrosion
    • Damaged barriers
    • Blocked ventilation
    • Evidence of water entry

    Current and event measurements

    A clamp meter, power-quality analyzer, or monitoring system may reveal overloads, imbalance, harmonics, inrush, or intermittent faults. Measurements should capture the operating cycle, not just a single moment after the system has stabilized.

    Maintenance and operating history

    A breaker’s history can explain conditions that a visual inspection cannot. Useful records include:

    • Previous fault interruptions
    • Trip events
    • Maintenance dates
    • Test results
    • Loading trends
    • Environmental exposure
    • Number of mechanical operations
    • Changes to trip settings
    • Recent equipment modifications

    A breaker that has interrupted a major fault may require inspection, testing, or replacement even if it can be reset.

    A Practical Troubleshooting Sequence

    When an MCCB trips or behaves abnormally, a structured investigation is safer and more effective than immediately resetting it.

    1. Preserve the evidence

    Record handle position, trip indicators, alarm messages, temperatures, load conditions, and the operating event that preceded the trip. Retrieve electronic event data before resetting the device if possible.

    2. Make the area safe

    Follow the facility’s electrical-safety procedures. Inspect for smoke, odor, deformation, loose material, water, or signs of arcing. Do not close a visibly damaged breaker.

    3. Identify the trip function

    Determine whether the event was caused by long-time, short-time, instantaneous, or ground-fault protection. This greatly narrows the investigation.

    4. Inspect the circuit and connected load

    Look for damaged cables, failed motors, shorted components, ground faults, jammed machinery, overload conditions, and recent changes to the system.

    5. Verify the application

    Confirm the breaker rating, interrupting capacity, conductor size, trip-unit configuration, accessory wiring, and coordination requirements. Verify settings against the approved protection study or design documentation.

    6. Measure and compare

    Where it is safe and appropriate, compare phase currents, voltage drops, terminal temperatures, and insulation-test results. Look for patterns rather than relying on one isolated value.

    7. Test the breaker appropriately

    Testing may include mechanical operation, insulation resistance, contact resistance, primary-current injection, secondary injection, or trip-unit functional testing. The correct method depends on the breaker design and manufacturer’s instructions.

    A push-to-trip button verifies only part of the mechanical trip path. It does not prove that the complete overcurrent-protection system will respond correctly to actual current.

    8. Correct the root cause

    Replacing a breaker will not solve an overloaded circuit, loose termination, damaged cable, incorrect setting, excessive enclosure temperature, or poorly coordinated protection scheme. Resolve the underlying condition before returning the system to service.

    Resetting Is Not Troubleshooting

    Repeatedly resetting an MCCB without identifying the cause can expose equipment and personnel to escalating risk. A downstream fault may worsen with each re-energization, and a breaker already damaged by fault current may not safely interrupt the next event.

    Before reclosing, there should be a reasonable technical basis for believing that:

    • The fault has been identified and cleared
    • The breaker is suitable for continued service
    • No visible or measured condition indicates damage
    • Protective settings are correct
    • Re-energization follows the site’s safety procedures

    When those conditions cannot be established, the appropriate response is further inspection and testing, not another reset.

    When an MCCB Should Be Replaced

    Replacement is generally warranted when the breaker has visible case damage, carbon tracking, severe overheating, unreliable operation, failed electrical tests, damaged terminals, or a defective trip unit that cannot be serviced.

    Replacement may also be appropriate after a high-energy fault, depending on the breaker’s condition and the manufacturer’s guidance.

    A replacement breaker must match the required:

    • Voltage rating
    • Continuous-current rating
    • Interrupting capacity
    • Number of poles
    • Trip functions
    • Connection type
    • Accessories
    • Equipment listing and compatibility
    • Coordination requirements

    Physical fit alone does not establish electrical suitability.

    The Bottom Line

    An MCCB is a precision protective device, not merely a reusable switch. Its ability to carry normal current and interrupt dangerous current depends on the condition of its electrical, mechanical, and protective components.

    Unexpected trips, hot terminals, unusual sounds, inconsistent operation, and diagnostic indicators should be treated as evidence, not inconveniences to bypass. Effective troubleshooting combines trip data, electrical measurements, thermal patterns, physical inspection, application review, and maintenance history.

    Most importantly, a reset confirms only that the handle can be moved. It does not prove that the fault is gone or that the breaker remains capable of protecting the circuit.

  • How Multipath Ultrasonic Flowmeters Improve Accuracy in Large Pipelines

    How Multipath Ultrasonic Flowmeters Improve Accuracy in Large Pipelines

    Measuring flow in a large pipeline is rarely as simple as installing a meter and reading the result. Pipe diameter, installation geometry, changing flow rates, upstream disturbances, fluid properties, and maintenance constraints can all affect measurement quality.

    These challenges become especially important when small errors carry large financial or operational consequences. A one-percent error may sound minor, but in a pipeline moving thousands of units per hour, it can represent a substantial discrepancy over time.

    Multipath ultrasonic flowmeters address this problem by measuring velocity across several acoustic paths instead of relying on a single point or line. The additional paths allow the meter to capture more of the actual flow profile, recognize distortion, and produce a more representative estimate of average velocity.

    How Transit-Time Ultrasonic Measurement Works

    Many ultrasonic meters used in large liquid and gas pipelines operate on the transit-time principle.

    Transducers send ultrasonic pulses both downstream and upstream through the flowing fluid. The pulse traveling with the flow arrives slightly sooner than the pulse traveling against it. The meter uses this difference in transit time to calculate fluid velocity along the acoustic path.

    The basic sequence is:

    1. An ultrasonic pulse travels diagonally across the pipe in the downstream direction.
    2. Another pulse travels along the same path in the upstream direction.
    3. The meter measures the difference between the two travel times.
    4. The electronics calculate path velocity.
    5. Path velocity is converted into average pipe velocity.
    6. Average velocity is multiplied by the pipe’s internal cross-sectional area to determine volumetric flow.

    The time difference can be extremely small, so accurate measurement depends on precise timing, stable signal detection, correct pipe dimensions, and a reliable understanding of the velocity distribution inside the pipe.

    Why One Acoustic Path May Not Be Enough

    Flow velocity is not uniform across a pipeline.

    Under ideal conditions, the velocity profile may be reasonably symmetrical, with slower fluid near the pipe wall and faster fluid toward the center. Real installations, however, often produce profiles that are skewed, flattened, swirling, or otherwise distorted.

    Common causes include:

    • Elbows
    • Tees
    • Partially open valves
    • Reducers and expanders
    • Pumps and compressors
    • Flow conditioners
    • Headers and manifolds
    • Changes in operating rate
    • Deposits or internal roughness
    • Insufficient straight pipe

    A single acoustic path samples only one portion of this profile. If that portion is moving faster or slower than the true cross-sectional average, the calculated flow may be biased.

    The problem is similar to estimating the average traffic speed on a multi-lane highway by observing only one lane. The result may be correct if all lanes behave similarly, but it becomes unreliable when one lane moves differently from the others.

    What Makes a Flowmeter “Multipath”?

    A multipath ultrasonic flowmeter uses several pairs of transducers to create multiple acoustic paths through the pipe. These paths may cross the pipeline at different heights, angles, or orientations.

    Each path produces an independent velocity measurement. The meter then combines the measurements using a mathematical weighting method designed to estimate the average velocity across the entire pipe.

    Depending on the application and meter design, the instrument may use:

    • Paths placed at different distances from the pipe center
    • Crossed paths that help detect asymmetry
    • Paths in more than one measurement plane
    • Reflective paths that make multiple traverses through the fluid
    • Redundant paths for diagnostics and continued operation

    The number of paths alone does not determine performance. Path placement, transducer quality, signal processing, calibration, meter-body geometry, and the integration algorithm are equally important.

    More Complete Sampling of the Velocity Profile

    The primary advantage of a multipath meter is broader sampling.

    A path near the center of the pipe may encounter higher velocity, while paths closer to the walls measure slower regions. By combining strategically located measurements, the flow computer can estimate the cross-sectional average more accurately than a single path usually can.

    Multipath sampling is especially valuable in large pipelines because the distance between the centerline and the pipe wall is substantial. A local velocity measurement may not represent the full flow field.

    Well-designed path geometry reduces the meter’s sensitivity to reasonable changes in the velocity profile. As the process rate or upstream conditions change, the meter can continue to form a representative average rather than depending on one fixed sample region.

    Better Handling of Asymmetric Flow

    An upstream elbow can push the highest-velocity region away from the pipe center. Two elbows in different planes can create an even more complicated profile with swirl and cross-flow components.

    A single-path meter may interpret this local shift as a change in total flow. A multipath meter can compare velocities from different parts of the pipe and compensate more effectively for the asymmetry.

    For example, if the paths on one side consistently report higher velocity than paths on the opposite side, the meter can identify that the flow profile is not symmetrical. Its integration algorithm uses the combined path data to reduce the bias that any one path might introduce.

    This does not mean multipath technology eliminates installation requirements. Severe distortion can still affect accuracy. It does, however, provide greater tolerance and more information about what is happening inside the pipe.

    Improved Detection of Swirl

    Swirl occurs when fluid rotates around the pipeline axis while continuing to move downstream. It may result from elbows, valves, pumps, compressors, or complex piping configurations.

    Swirl can influence an ultrasonic path differently depending on its orientation. In a crossed-path arrangement, one path may be affected in one direction while another responds differently.

    Comparing those paths helps the meter distinguish axial flow from rotational components. Designs using multiple measurement planes can be particularly effective at identifying complex flow patterns.

    The ability to detect swirl is valuable for two reasons:

    • It helps the meter maintain accuracy within its design limits.
    • It provides a diagnostic indication that the installation or flow condition may be less than ideal.

    Reduced Sensitivity to Individual Path Errors

    A single-path instrument depends entirely on one acoustic measurement. If that path is affected by deposits, gas bubbles, liquid droplets, weak signal strength, transducer degradation, or electronic noise, the meter’s only velocity measurement may become unreliable.

    A multipath meter provides more measurement information. Its diagnostics may compare paths and identify one that behaves differently from the rest.

    Depending on the design and configuration, the instrument may:

    • Flag the affected path
    • Exclude invalid data
    • Continue operating in a degraded mode
    • Estimate flow using the remaining valid paths
    • Generate a maintenance alert before total measurement is lost

    Redundancy does not make the meter immune to common-mode problems. If every path is affected by the same fluid condition or incorrect pipe-area value, the reported flow can still be wrong. Nevertheless, path-to-path comparison is a powerful diagnostic tool.

    Lower Pressure Loss

    Ultrasonic meters generally have no primary element projecting into the flow stream. A full-bore meter can provide an essentially unobstructed flow passage.

    Compared with technologies that create a differential pressure, this can reduce permanent pressure loss and the associated pumping or compression energy.

    The benefit is particularly significant in large pipelines, where even a small additional pressure drop may have a meaningful energy cost.

    An unobstructed bore also makes ultrasonic meters attractive for applications involving:

    • High flow rates
    • Large pipe diameters
    • Bidirectional flow
    • Fluids carrying limited solids
    • Processes that cannot tolerate a major restriction
    • Systems where pressure loss must be minimized

    Wide Measurement Range

    Multipath ultrasonic meters can offer a broad usable flow range. Multiple paths provide stable sampling as the velocity profile changes between low and high rates.

    At low velocity, however, the upstream and downstream transit times become very similar. Accurate timing and signal processing are therefore critical. At high velocity, turbulence, acoustic refraction, and signal attenuation may become more influential.

    Actual turndown depends on the meter, fluid, pipeline geometry, required uncertainty, and operating conditions. A wide published range should not be treated as guaranteed performance for every installation.

    Path Diagnostics Reveal More Than a Flow Value

    One of the strongest advantages of multipath measurement is the amount of diagnostic information it can provide.

    Depending on the meter, available indicators may include:

    • Velocity on each path
    • Speed of sound on each path
    • Path-to-path velocity agreement
    • Path-to-path speed-of-sound agreement
    • Signal strength
    • Gain or amplification level
    • Signal-to-noise ratio
    • Transit-time quality
    • Rejected pulse count
    • Turbulence indicators
    • Profile symmetry
    • Swirl indicators
    • Active or failed paths

    These values help distinguish a genuine process change from a measurement problem.

    If the total flow changes while all paths remain consistent, the change is more likely to be real. If one path suddenly deviates while the others remain stable, the issue may involve that path’s transducers, cabling, electronics, or acoustic conditions.

    Speed of Sound as a Diagnostic Tool

    The meter calculates the fluid’s speed of sound as part of the transit-time measurement. Under uniform fluid conditions, different paths should generally report similar values.

    A disagreement among paths may indicate:

    • Temperature stratification
    • Composition differences
    • Liquid accumulation in a gas line
    • Entrained gas in a liquid
    • Contamination
    • Deposits affecting a path
    • Incorrect signal detection
    • Transducer or electronics problems

    In some applications, measured speed of sound can also be compared with an expected value based on fluid composition, pressure, and temperature. A significant mismatch may reveal incorrect process data or an unexpected change in the fluid.

    Accuracy Still Depends on Pipe Area

    An ultrasonic meter determines velocity, but volumetric flow also depends on the pipe’s internal cross-sectional area.

    An incorrect internal diameter creates a direct bias in the flow calculation. Potential sources of error include:

    • Incorrect pipe schedule
    • Manufacturing tolerances
    • Internal coating thickness
    • Corrosion
    • Scale or wax buildup
    • Liners
    • Deformation
    • Incorrect temperature or pressure compensation

    For high-accuracy service, the effective internal diameter must be established carefully. In metering runs, the bore may be precisely measured and matched to adjacent piping.

    Multipath measurement cannot compensate for an incorrect area value shared by the entire calculation.

    Installation Geometry Still Matters

    Multipath meters tolerate disturbed flow better than simpler measurement arrangements, but they do not make installation effects disappear.

    Accuracy can still be influenced by:

    • Distance from elbows and valves
    • Orientation relative to upstream disturbances
    • Meter-body alignment
    • Gasket intrusion
    • Internal diameter steps
    • Protruding welds
    • Surface roughness
    • Flow-conditioner placement
    • Pipe contamination
    • Temperature stratification

    The manufacturer’s installation requirements should therefore be followed, including recommendations for straight runs and transducer-plane orientation.

    Where space is limited or uncertainty requirements are demanding, computational analysis, laboratory testing, or calibration with the actual piping configuration may be justified.

    Clamp-On Versus Inline Multipath Meters

    Multipath technology can be applied in both inline and clamp-on designs, but their uncertainty sources differ.

    Inline meters

    Inline meters integrate the acoustic paths into a manufactured meter body. Their transducer positions, acoustic geometry, and internal diameter can be tightly controlled.

    They are generally favored for demanding applications such as custody transfer, allocation, and high-value process measurement.

    Clamp-on meters

    Clamp-on transducers are mounted on the outside of an existing pipe. They avoid cutting into the pipeline and can be installed without interrupting service.

    Their performance depends heavily on accurate knowledge of:

    • Pipe outside diameter
    • Wall thickness
    • Pipe material
    • Liner or coating
    • Fluid properties
    • Transducer spacing
    • Acoustic coupling
    • Pipe condition

    Multipath clamp-on arrangements can improve profile coverage and diagnostic confidence, but external installation introduces additional variables that must be controlled carefully.

    Calibration and Verification

    A multipath meter may be mathematically sophisticated, but calibration remains essential when low uncertainty is required.

    Flow calibration compares the complete meter against a traceable reference under controlled conditions. For some applications, the meter may be calibrated at multiple flow rates to establish its performance curve.

    Important considerations include:

    • Calibration fluid
    • Pressure and temperature
    • Reynolds-number range
    • Upstream piping configuration
    • Flow conditioner
    • Meter orientation
    • Bidirectional operation
    • Electronic configuration

    After installation, verification should include more than checking the displayed flow value. Baseline diagnostic data should be recorded so later changes can be recognized.

    A useful baseline may include path velocities, speed of sound, signal strength, gain, profile indicators, and zero-flow behavior.

    Common Misconceptions

    “More paths automatically mean better accuracy.”

    Additional paths can improve sampling, but performance also depends on where the paths are positioned, how they are weighted, and how well the meter is calibrated. A well-designed four-path meter may outperform a poorly designed meter with more paths.

    “Multipath meters do not need straight pipe.”

    They may be less sensitive to profile distortion, but upstream geometry still affects the flow field. Installation requirements remain important.

    “If all paths are working, the measurement must be correct.”

    All paths can agree while the flow result remains biased by an incorrect internal diameter, configuration error, calibration problem, or common fluid effect.

    “Ultrasonic meters are maintenance-free.”

    They have no moving parts in the flow stream, but they still require diagnostic review, electronics checks, transducer evaluation, and inspection for deposits or process changes.

    “Diagnostics can replace calibration.”

    Diagnostics help determine whether the meter is behaving consistently. They do not independently establish traceable measurement accuracy.

    A Practical Commissioning Checklist

    Before placing a multipath ultrasonic meter into service:

    1. Verify the meter size, bore, pressure class, and flow direction.
    2. Confirm that the installed meter matches the configured serial number and calibration data.
    3. Review upstream and downstream piping against installation requirements.
    4. Inspect for gasket, weld, or diameter intrusions.
    5. Verify pressure, temperature, composition, and density inputs where required.
    6. Confirm units, scaling, communications, and low-flow cutoff settings.
    7. Compare path velocities and speed-of-sound readings.
    8. Check signal strength, gain, and signal-to-noise indicators.
    9. Evaluate zero-flow behavior where a true zero condition can be established.
    10. Record a diagnostic baseline under stable operating conditions.
    11. Confirm that alarms for path failure and degraded operation are enabled.
    12. Document the normal diagnostic ranges for future comparison.

    The Bottom Line

    Multipath ultrasonic flowmeters improve measurement accuracy by observing more of the flow field.

    Instead of relying on one acoustic path to represent an entire large pipeline, they measure velocity across several regions and combine the results into a more representative average. This reduces sensitivity to asymmetric profiles, provides better insight into swirl, and creates valuable diagnostic redundancy.

    Their advantages are substantial: no significant flow obstruction, low pressure loss, broad operating range, and detailed information about measurement health.Multipath technology, however, is not a substitute for proper meter selection, accurate pipe dimensions, sound installation, calibration, and ongoing verification. Its greatest value comes from combining better physical sampling with intelligent diagnostics, and using both to understand not just the reported flow, but the quality of the measurement behind it