Author: Brian Ribeiro

  • Designing User-Friendly HMI Screens: Layout, Color, and Workflow Tips

    Designing User-Friendly HMI Screens: Layout, Color, and Workflow Tips

    Human-Machine Interfaces (HMIs) serve as the bridge between operators and industrial equipment. Whether controlling a manufacturing line, monitoring a water treatment facility, or managing an HVAC system, the effectiveness of an HMI can significantly impact productivity, safety, and operational efficiency.

    Unfortunately, not all HMI screens are designed with the operator in mind. Overly complex layouts, excessive colors, and poorly organized information can lead to confusion, slower response times, and increased risk of operator error.

    Effective HMI design focuses on clarity, usability, and situational awareness. By following proven design principles for layout, color usage, and workflow organization, engineers and system integrators can create interfaces that help operators make faster, more informed decisions.

    Why HMI Design Matters

    An HMI is much more than a graphical representation of equipment. It is a decision-making tool.

    Operators use HMIs to:

    • Monitor system performance
    • Identify alarms and abnormal conditions
    • Adjust process parameters
    • Start and stop equipment
    • Analyze trends and historical data
    • Respond to system events

    When information is presented clearly, operators can quickly understand system status and take appropriate action. Poorly designed interfaces can have the opposite effect, increasing workload and delaying responses during critical situations.

    In industries where downtime, safety incidents, or product quality issues carry significant consequences, effective HMI design becomes a valuable operational asset.

    Start with the Operator’s Workflow

    One of the most common HMI design mistakes is building screens around the equipment instead of the operator.

    Engineers often organize screens based on how systems are wired or programmed. Operators, however, think in terms of tasks and processes.

    Before designing any screen, ask:

    • What information does the operator need most frequently?
    • What actions must be performed regularly?
    • What decisions need to be made quickly?
    • What problems occur most often?

    The answers should guide the structure of the interface.

    A well-designed HMI supports the natural workflow of the operator rather than forcing operators to search through multiple screens to find critical information.

    Design Around a Clear Screen Hierarchy

    Modern HMI design often follows a hierarchical structure that allows users to move from high-level system visibility to detailed diagnostics.

    Level 1: System Overview

    The primary screen should provide a high-level overview of the entire process.

    This screen should answer questions such as:

    • Is the system operating normally?
    • Where are problems occurring?
    • What equipment is running?
    • Are there active alarms?

    The overview screen serves as the operator’s dashboard and should be accessible at all times.

    Level 2: Area or Process Screens

    These screens provide more detailed information about specific process areas, machines, or production lines.

    Examples include:

    • Pump stations
    • Packaging equipment
    • Conveyor systems
    • HVAC zones

    Level 3: Equipment Detail Screens

    These screens display detailed operating information for individual assets.

    Examples include:

    • Motor status
    • Drive parameters
    • Sensor readings
    • Maintenance data

    Level 4: Diagnostic and Configuration Screens

    The most detailed screens should be reserved for troubleshooting and engineering functions.

    This layered approach helps prevent information overload while allowing operators to drill down when necessary.

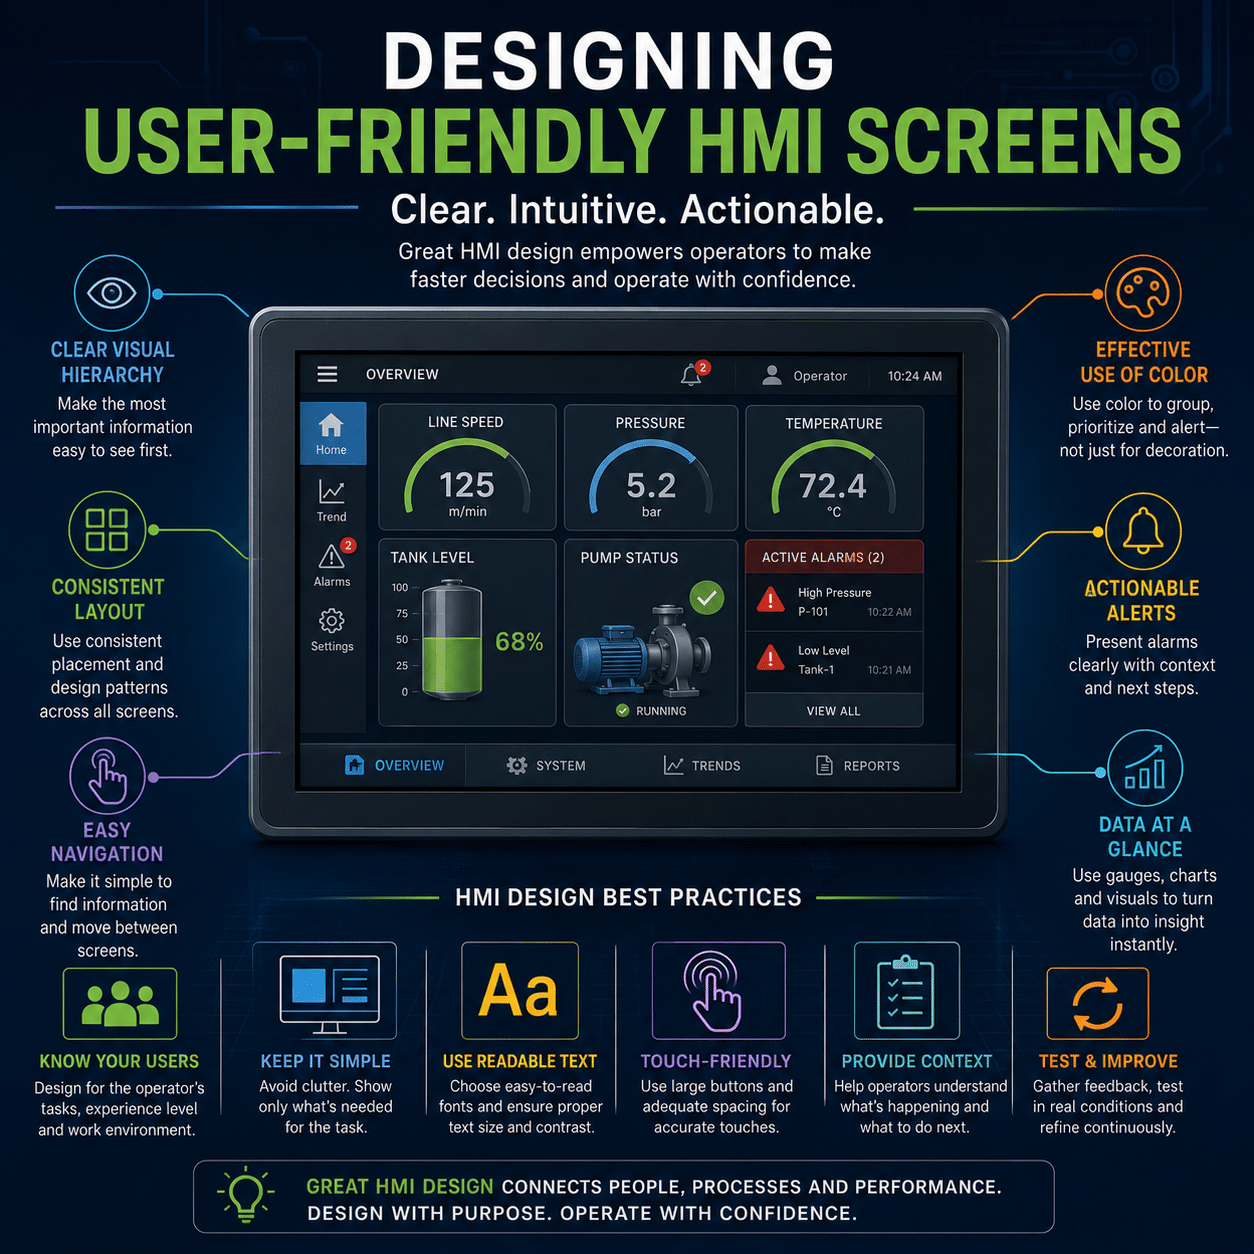
    Keep Screen Layouts Clean and Organized

    A cluttered screen increases cognitive load and makes it more difficult for operators to identify important information.

    Effective layouts typically include:

    Consistent Navigation

    Navigation buttons should remain in the same location throughout the application.

    Common placements include:

    • Top navigation bars
    • Left-side menu panels
    • Fixed footer controls

    Consistency helps operators build familiarity and reduces training requirements.

    Logical Grouping

    Related information should be grouped together.

    For example:

    • Pump controls next to pump status indicators
    • Temperature values grouped with temperature alarms
    • Production metrics displayed in a common dashboard section

    Grouping information reduces the amount of visual searching required.

    Adequate White Space

    White space is not wasted space.

    Strategic spacing improves readability and helps separate different functional areas of the screen.

    Crowded interfaces often appear more complex than they actually are.

    Use Color Purposefully

    One of the biggest mistakes in HMI design is using too many colors.

    Many older systems display equipment in bright reds, greens, blues, yellows, and purples simultaneously, creating a visually overwhelming experience.

    Modern high-performance HMI design takes a different approach.

    Use Neutral Colors for Normal Conditions

    Normal operating equipment should typically appear in neutral tones such as:

    • Gray
    • White
    • Soft blue
    • Muted earth tones

    When everything is colorful, nothing stands out.

    Reserve Bright Colors for Abnormal Conditions

    Color should attract attention only when necessary.

    Common conventions include:

    Color

    Typical Meaning

    Red

    Critical alarm or fault

    Yellow/Amber

    Warning or abnormal condition

    Green

    Running or active status

    Blue

    Operator action required

    Gray

    Inactive or unavailable

    By minimizing color use during normal operation, alarms become immediately noticeable.

    Prioritize Situational Awareness

    The primary purpose of an HMI is helping operators understand what is happening right now.

    Good situational awareness means operators can quickly answer:

    • What is happening?
    • Why is it happening?
    • What needs attention?
    • What action should be taken?

    To support situational awareness:

    Display Key Performance Indicators (KPIs)

    Important metrics should be visible without navigating through multiple screens.

    Examples include:

    • Production rate
    • Energy consumption
    • Flow rate
    • Temperature
    • Pressure
    • Equipment utilization

    Highlight Trends

    Operators often gain more insight from trends than from individual values.

    Trend displays help identify:

    • Gradual performance degradation
    • Process instability
    • Equipment wear
    • Developing faults

    Historical context supports better decision-making.

    Simplify Alarm Management

    Poor alarm design can overwhelm operators during abnormal events.

    Best practices include:

    Prioritize Alarms

    Not every event should be treated as critical.

    Classify alarms according to severity:

    • Critical
    • High
    • Medium
    • Informational

    Avoid Alarm Flooding

    Excessive alarm notifications can cause operators to ignore important alerts.

    Alarm rationalization helps ensure only meaningful events trigger notifications.

    Provide Context

    An alarm should explain:

    • What happened
    • Where it occurred
    • Possible causes
    • Recommended actions

    The goal is to help operators respond, not simply notify them.

    Optimize for Touchscreen Operation

    As touchscreen HMIs become increasingly common, interfaces should be designed accordingly.

    Use Larger Touch Targets

    Buttons should be large enough for accurate operation while wearing gloves if required.

    Avoid Overcrowding Controls

    Closely spaced buttons increase the risk of accidental selections.

    Limit Excessive Data Entry

    Whenever possible:

    • Use dropdown menus
    • Provide preset selections
    • Minimize keyboard input

    Reducing manual entry speeds operation and reduces errors.

    Standardize Graphics and Symbols

    Consistency improves usability.

    Operators should not need to interpret different symbols for identical equipment across screens.

    Standardize:

    • Pumps
    • Valves
    • Motors
    • Sensors
    • Conveyors
    • Drives

    Consistent graphics reduce training time and improve operator confidence.

    Test with Real Operators

    One of the most valuable steps in HMI development occurs before deployment.

    Involve actual operators during design reviews.

    Ask them:

    • Is information easy to find?
    • Are controls intuitive?
    • What screens are used most frequently?
    • What would improve response times?

    Operators often identify usability issues that engineers may overlook.

    Testing early can prevent costly redesigns later.

    Common HMI Design Mistakes

    Avoid these frequently encountered issues:

    • Excessive use of bright colors
    • Overcrowded screens
    • Inconsistent navigation
    • Too many alarms
    • Small touchscreen controls
    • Excessive animations
    • Complex menu structures
    • Lack of trend data
    • Poorly organized information
    • Screens designed around hardware rather than operator tasks

    Eliminating these problems often leads to immediate improvements in usability.

    Final Thoughts

    A well-designed HMI does more than display information—it helps operators understand processes, identify problems, and make informed decisions quickly. Effective HMI design combines clean layouts, thoughtful color usage, logical workflows, and clear navigation to create an interface that supports both productivity and safety.

    By focusing on operator needs, minimizing visual clutter, and emphasizing situational awareness, organizations can build HMIs that improve efficiency, reduce errors, shorten training time, and enhance overall system performance.

    In today’s increasingly automated facilities, user-friendly HMI design is not simply a convenience—it is an essential component of successful industrial operations.

  • How Battery Management Systems (BMS) Improve UPS Reliability

    How Battery Management Systems (BMS) Improve UPS Reliability

    Uninterruptible Power Supply (UPS) systems play a critical role in maintaining power continuity for mission-critical operations. From data centers and healthcare facilities to industrial automation systems and telecommunications infrastructure, UPS systems protect equipment and operations from power disturbances, outages, and voltage instability.

    At the heart of every UPS system is the battery system. While UPS electronics often receive significant attention, battery reliability ultimately determines whether backup power will be available when it is needed most. This is where Battery Management Systems (BMS) become essential.

    Modern Battery Management Systems help improve UPS reliability by continuously monitoring, protecting, and optimizing battery performance. As battery technologies evolve and facilities demand greater uptime, BMS technologies are becoming increasingly important for maintaining dependable backup power systems.

    What Is a Battery Management System (BMS)?

    A Battery Management System is an electronic control and monitoring system designed to supervise battery operation and ensure safe, reliable performance.

    A BMS continuously monitors key battery parameters such as:

    • Voltage
    • Current
    • Temperature
    • State of charge (SOC)
    • State of health (SOH)
    • Cell balancing conditions
    • Charging and discharging behavior

    The system uses this data to protect the batteries, optimize performance, and provide visibility into battery condition.

    BMS platforms are commonly used with:

    • Lithium-ion battery systems
    • Advanced energy storage systems
    • Modern UPS platforms
    • Renewable energy storage applications
    • Mission-critical backup systems

    Why Battery Reliability Matters in UPS Systems

    The battery system is often the most vulnerable component within a UPS installation.

    Even when UPS electronics remain fully operational, battery failures can prevent backup power delivery during an outage.

    Common battery-related UPS problems include:

    • Reduced runtime
    • Premature battery aging
    • Overheating
    • Cell imbalance
    • Unexpected failures
    • Thermal runaway risks
    • Inaccurate runtime predictions

    In many facilities, batteries are expected to remain on standby for long periods while still being capable of delivering immediate power during an emergency. Without proper monitoring and management, battery degradation may go unnoticed until failure occurs.

    The Growing Importance of BMS Technology

    As UPS systems increasingly adopt lithium-ion battery technologies, Battery Management Systems have become even more critical.

    Compared to traditional valve-regulated lead-acid (VRLA) batteries, lithium-ion systems offer:

    • Higher energy density
    • Longer lifespan
    • Faster charging
    • Reduced maintenance
    • Smaller footprint

    However, lithium-ion batteries require more advanced monitoring and control to ensure safe operation.

    BMS platforms provide the intelligence needed to safely manage these advanced battery systems while maximizing performance and reliability.

    How Battery Management Systems Improve UPS Reliability

    Battery Management Systems support UPS reliability in several important ways.

    Continuous Battery Monitoring

    One of the primary functions of a BMS is real-time monitoring of battery conditions.

    The BMS continuously tracks:

    • Individual cell voltages
    • Battery temperatures
    • Charging current
    • Discharge current
    • Internal resistance
    • Overall pack performance

    This constant visibility helps identify abnormalities before they become critical failures.

    Without continuous monitoring, battery degradation may remain undetected until the UPS is called upon during a power outage.

    Early Fault Detection

    A major advantage of BMS technology is predictive fault detection.

    The system can identify warning signs such as:

    • Weak cells
    • Voltage imbalance
    • Excessive temperatures
    • Abnormal charging behavior
    • Capacity degradation

    Early detection allows maintenance teams to address issues proactively, reducing the likelihood of unexpected battery failure.

    Cell Balancing Improves Performance

    Battery packs contain multiple cells connected together. Over time, slight differences between cells can lead to imbalance.

    Cell imbalance may cause:

    • Reduced runtime
    • Uneven aging
    • Reduced charging efficiency
    • Increased thermal stress

    A BMS performs cell balancing by equalizing charge levels across cells.

    Proper balancing:

    • Maximizes usable battery capacity
    • Improves runtime consistency
    • Extends battery life
    • Enhances overall reliability

    Temperature Management

    Temperature is one of the most important factors affecting battery performance and lifespan.

    Excessive heat can accelerate:

    • Battery degradation
    • Capacity loss
    • Thermal stress
    • Safety risks

    Low temperatures may reduce battery performance and discharge capability.

    A BMS monitors battery temperatures continuously and may:

    • Trigger alarms
    • Adjust charging parameters
    • Activate cooling systems
    • Shut down unsafe operation

    Effective thermal management significantly improves long-term UPS reliability.

    Protection Against Overcharging and Deep Discharge

    Improper charging and discharging can permanently damage batteries.

    The BMS helps protect batteries from:

    • Overvoltage conditions
    • Undervoltage conditions
    • Excessive charging current
    • Excessive discharge current

    These protections help preserve battery health and prevent catastrophic failures.

    Improved Runtime Accuracy

    Modern BMS platforms provide more accurate runtime predictions by analyzing:

    • State of charge
    • Battery health
    • Load conditions
    • Temperature effects

    This allows operators to better understand actual backup power availability during outages.

    Improved runtime visibility supports better operational planning and emergency preparedness.

    Enhanced Safety

    Battery safety is a major concern in mission-critical facilities.

    A BMS helps reduce risks associated with:

    • Thermal runaway
    • Short circuits
    • Overheating
    • Internal battery faults
    • Unsafe operating conditions

    If dangerous conditions are detected, the BMS can automatically disconnect the battery system or trigger protective actions.

    This is especially important in high-energy lithium-ion battery systems.

    Extending Battery Lifespan

    Battery replacement represents a major portion of UPS lifecycle costs.

    A properly managed battery system can significantly extend operational lifespan by:

    • Reducing thermal stress
    • Preventing overcharging
    • Maintaining balanced cells
    • Optimizing charge cycles
    • Minimizing deep discharges

    Longer battery life reduces:

    • Maintenance costs
    • Replacement frequency
    • Operational disruptions

    Supporting Predictive Maintenance

    Modern BMS platforms generate valuable operational data that supports predictive maintenance strategies.

    Facilities can analyze:

    • Historical performance trends
    • Temperature patterns
    • Capacity degradation
    • Charging behavior
    • Alarm history

    This data helps maintenance teams schedule service proactively rather than reacting to failures.

    Predictive maintenance improves both reliability and operational efficiency.

    Remote Monitoring and Communication

    Many advanced BMS platforms support remote monitoring and industrial communication protocols.

    This enables integration with:

    • Building management systems (BMS)
    • SCADA systems
    • Data center infrastructure management (DCIM)
    • Remote monitoring platforms

    Operators can receive real-time alerts and monitor battery status across multiple UPS installations.

    Remote visibility improves response times and system oversight.

    Supporting Redundancy Strategies

    In mission-critical environments, redundancy is essential.

    BMS technologies help support redundant UPS architectures by providing:

    • Independent battery monitoring
    • Fault isolation
    • System diagnostics
    • Load-sharing visibility

    Improved monitoring helps maintain reliability in parallel UPS configurations.

    Common Applications Benefiting from BMS Integration

    Battery Management Systems are increasingly important across many industries.

    Data Centers

    Continuous uptime and backup power reliability are critical for preventing data loss and service interruptions.

    Healthcare Facilities

    Hospitals and medical facilities require reliable emergency power for life-safety systems and critical equipment.

    Industrial Facilities

    Manufacturing operations rely on UPS systems to protect automation systems, control equipment, and sensitive processes.

    Telecommunications

    Network infrastructure depends on stable backup power to maintain communication services during outages.

    Renewable Energy Systems

    Energy storage systems require advanced battery management for reliable operation and grid support.

    Challenges Without a BMS

    UPS systems operating without advanced battery monitoring may experience:

    • Undetected battery degradation
    • Inaccurate runtime expectations
    • Increased failure risk
    • Reduced battery life
    • Limited fault visibility
    • Greater maintenance uncertainty

    In critical applications, these limitations can significantly increase operational risk.

    Fuji Electric UPS Solutions

    Fuji Electric provides advanced UPS solutions designed to support high reliability, operational continuity, and efficient power protection across demanding applications.

    Our UPS technologies support:

    • Advanced battery integration
    • Reliable backup power performance
    • Intelligent monitoring capabilities
    • Energy-efficient operation
    • Mission-critical infrastructure protection

    Fuji Electric solutions help facilities improve uptime, protect sensitive equipment, and maintain dependable power continuity in modern industrial and commercial environments.

    Battery reliability is one of the most important factors in overall UPS system performance. As backup power systems become more advanced and battery technologies continue evolving, Battery Management Systems are playing an increasingly vital role in maintaining operational reliability and safety.

    By providing continuous monitoring, fault detection, thermal management, cell balancing, and predictive diagnostics, BMS technologies help facilities reduce downtime risk, extend battery life, and improve confidence in backup power availability.

    For organizations that depend on uninterrupted power, integrating advanced Battery Management Systems is no longer simply an added feature, it is a critical component of modern UPS reliability strategy.

  • Differences Between Manual, Magnetic, and Electronic Motor Protection

    Differences Between Manual, Magnetic, and Electronic Motor Protection

    Electric motors are essential to modern industrial operations, powering everything from pumps and conveyors to compressors, fans, and production equipment. Because motors represent a significant investment and are often critical to uptime, proper motor protection is essential for maintaining reliability, safety, and operational efficiency.

    Motor protection systems are designed to prevent damage caused by overloads, short circuits, phase loss, locked rotor conditions, overheating, and other electrical or mechanical faults. However, not all motor protection methods operate the same way. Three of the most common approaches are manual motor protection, magnetic motor protection, and electronic motor protection.

    Understanding the differences between these technologies can help engineers, facility managers, OEMs, and maintenance teams select the best solution for their application.

    Why Motor Protection Matters

    Electric motors operate under varying loads and environmental conditions. Without proper protection, abnormal operating conditions can quickly lead to:

    • Motor overheating
    • Insulation breakdown
    • Premature bearing failure
    • Electrical fires
    • Equipment downtime
    • Production losses
    • Increased maintenance costs

    Motor protection devices help disconnect or control power before damage occurs, improving both safety and equipment longevity.

    The level of protection required depends on factors such as:

    • Motor size
    • Load type
    • Starting characteristics
    • Duty cycle
    • Environmental conditions
    • Process criticality

    What Is Manual Motor Protection?

    Manual motor protection typically uses a manual motor starter or motor protection circuit breaker (MPCB) that combines disconnect functionality with basic overload and short-circuit protection.

    These devices are manually operated using a rotary handle, switch, or pushbutton mechanism.

    How Manual Motor Protection Works

    Manual protectors usually incorporate:

    • Thermal overload protection
    • Magnetic short-circuit protection
    • Manual ON/OFF motor control

    Thermal protection responds to sustained overcurrent conditions by heating a bimetallic element that trips the device when excessive current persists over time.

    Magnetic protection responds almost instantly to high fault currents such as short circuits.

    Advantages of Manual Motor Protection

    Manual motor protection offers several benefits:

    • Simple operation
    • Compact design
    • Cost-effective solution
    • Easy installation
    • Built-in disconnect capability
    • Suitable for small motors and simple systems

    These devices are commonly used in:

    • Small machinery
    • HVAC systems
    • Pumps
    • Fans
    • Light industrial equipment

    Limitations of Manual Motor Protection

    While manual systems are effective for many applications, they have limitations:

    • Limited fault diagnostics
    • Less precise overload protection
    • Manual reset requirements
    • Minimal communication capabilities
    • Reduced customization

    For basic motor control applications, manual protection may be entirely sufficient. However, more demanding systems often require additional functionality.

    What Is Magnetic Motor Protection?

    Magnetic motor protection typically refers to motor starters that use electromagnetic contactors combined with overload relays.

    This type of system allows motors to be controlled remotely and automatically while providing protection against overload conditions.

    How Magnetic Motor Protection Works

    A magnetic starter contains:

    • An electromagnetic contactor
    • Overload relay protection
    • Auxiliary contacts for control circuits

    When the control circuit energizes the contactor coil, the contactor closes and supplies power to the motor. If an overload condition occurs, the overload relay trips and opens the control circuit, disconnecting the motor.

    Unlike manual starters, magnetic starters allow:

    • Remote operation
    • Automated control
    • Integration with control systems
    • Frequent cycling

    Thermal Overload Protection

    Most traditional magnetic starters use thermal overload relays based on bimetallic elements or eutectic alloys.

    These relays are designed to simulate motor heating characteristics and trip when excessive current persists long enough to threaten motor insulation.

    Advantages of Magnetic Motor Protection

    Magnetic protection systems provide several important advantages:

    • Remote motor control capability
    • Integration with automation systems
    • Better support for larger motors
    • Frequent start-stop operation
    • Reduced operator involvement
    • Improved process automation

    These systems are widely used in:

    • Manufacturing systems
    • Conveyor systems
    • Pump stations
    • Industrial automation
    • HVAC systems
    • Material handling equipment

    Limitations of Traditional Magnetic Protection

    Despite their widespread use, traditional magnetic starters may have limitations:

    • Limited diagnostics
    • Mechanical wear over time
    • Fixed protection characteristics
    • Less accurate protection under varying conditions
    • Minimal real-time monitoring

    As industrial systems become more connected and data-driven, electronic motor protection is becoming increasingly common.

    What Is Electronic Motor Protection?

    Electronic motor protection uses digital electronics and microprocessor-based monitoring to provide advanced motor protection and diagnostics.

    These systems continuously monitor motor operating conditions and can respond more accurately to abnormal events than traditional thermal devices.

    Electronic motor protection may be integrated into:

    • Electronic overload relays
    • Intelligent motor controllers
    • Soft starters
    • AC drives
    • Motor management systems

    How Electronic Motor Protection Works

    Electronic systems use sensors and digital processing to monitor parameters such as:

    • Current
    • Voltage
    • Phase imbalance
    • Ground fault conditions
    • Motor temperature
    • Power consumption
    • Locked rotor conditions
    • Underload conditions

    Instead of relying solely on thermal elements, electronic protection calculates motor heating mathematically using real-time data.

    Advanced Protection Features

    Electronic motor protection systems often provide:

    • Adjustable trip classes
    • Phase loss protection
    • Phase imbalance detection
    • Ground fault monitoring
    • Jam detection
    • Underload protection
    • Stall protection
    • Thermal memory
    • Event logging
    • Communication capabilities

    Many systems also support industrial communication protocols for integration into automation and monitoring platforms.

    Advantages of Electronic Motor Protection

    Electronic protection provides significant benefits in modern industrial environments.

    Greater Accuracy

    Electronic systems offer more precise protection than traditional thermal devices, reducing nuisance trips while improving motor safety.

    Improved Diagnostics

    Many electronic systems provide detailed fault information that helps maintenance teams quickly identify problems.

    Enhanced Motor Life

    More accurate protection reduces thermal stress and helps extend motor lifespan.

    Communication and Monitoring

    Electronic protection devices often support:

    • Ethernet/IP
    • Modbus
    • PROFIBUS
    • EtherCAT
    • Remote monitoring systems

    This enables predictive maintenance and real-time operational visibility.

    Flexible Configuration

    Protection settings can often be adjusted digitally to match specific motor requirements and application demands.

    Limitations of Electronic Protection

    Although electronic protection offers many advantages, there are considerations:

    • Higher initial cost
    • Greater system complexity
    • Additional programming requirements
    • Potential need for communication infrastructure
    • More advanced troubleshooting skills

    However, the long-term operational benefits often outweigh the higher upfront investment, particularly in critical applications.

    Comparing Manual, Magnetic, and Electronic Protection

    Manual Motor Protection

    Best suited for:

    • Small motors
    • Simple standalone applications
    • Basic motor control
    • Cost-sensitive systems

    Key characteristics:

    • Manual operation
    • Basic overload and short-circuit protection
    • Simple installation
    • Limited diagnostics

    Magnetic Motor Protection

    Best suited for:

    • Automated motor control
    • Frequent motor cycling
    • Industrial control systems
    • Medium-sized motor applications

    Key characteristics:

    • Electromagnetic contactor operation
    • Remote control capability
    • Thermal overload protection
    • Automation compatibility

    Electronic Motor Protection

    Best suited for:

    • Critical industrial systems
    • Advanced automation
    • Process optimization
    • Predictive maintenance programs
    • High-value motor assets

    Key characteristics:

    • Advanced diagnostics
    • Real-time monitoring
    • Precise protection
    • Communication integration
    • Intelligent control features

    Selecting the Right Motor Protection Solution

    Choosing the proper protection method depends on several application factors.

    Application Complexity

    Simple standalone equipment may only require manual protection, while highly automated production lines benefit from electronic systems.

    Motor Criticality

    Critical motors with high downtime costs often justify advanced electronic protection.

    Environmental Conditions

    Harsh industrial environments may require robust protection features and monitoring capabilities.

    Maintenance Strategy

    Facilities implementing predictive maintenance programs often prefer electronic protection with communication and diagnostic features.

    Budget Considerations

    Initial equipment cost is important, but total lifecycle cost should also be considered, including:

    • Downtime reduction
    • Maintenance savings
    • Energy efficiency
    • Equipment longevity

    Fuji Electric Motor Protection Solutions

    Fuji Electric offers a broad range of motor control and protection technologies designed to support industrial reliability, efficiency, and safety.

    Our solutions include:

    • Manual motor starters
    • Magnetic contactors
    • Thermal overload relays
    • Intelligent motor protection systems
    • AC drives with integrated protection features
    • Advanced automation technologies

    Fuji Electric products are engineered to help facilities improve motor performance, reduce downtime, and support modern industrial automation requirements.

    Motor protection is a critical part of maintaining reliable and efficient industrial operations. Manual, magnetic, and electronic motor protection systems each offer unique advantages depending on the application requirements, operational complexity, and protection goals.

    Manual protection provides a simple and economical solution for basic applications. Magnetic protection enables automated motor control and supports larger industrial systems. Electronic protection delivers advanced diagnostics, monitoring, and intelligent protection for modern connected facilities.

    As industrial operations continue evolving toward smarter, more automated systems, advanced motor protection technologies will play an increasingly important role in improving uptime, extending equipment life, and optimizing overall system performance.

  • How to Mitigate Vibration-Induced Damage in Pressure Transmitters

    How to Mitigate Vibration-Induced Damage in Pressure Transmitters

    Pressure transmitters play a critical role in industrial automation systems, providing accurate pressure measurements for process control, equipment protection, and operational efficiency. From manufacturing plants and chemical processing facilities to water treatment systems and HVAC applications, reliable pressure monitoring is essential for maintaining stable operations.

    However, one common challenge that can significantly impact transmitter performance and longevity is vibration.

    Excessive vibration can introduce measurement inaccuracies, damage internal components, loosen electrical connections, and ultimately lead to premature transmitter failure. Understanding the causes of vibration-induced damage ,  and how to mitigate it ,  can help improve system reliability, reduce downtime, and extend equipment life.

    Why Vibration Is a Problem for Pressure Transmitters

    Industrial environments often expose instrumentation to continuous mechanical vibration generated by:

    • Pumps
    • Compressors
    • Motors
    • AC drives
    • Fans and blowers
    • Turbines
    • Piping systems
    • Reciprocating equipment

    Pressure transmitters mounted directly on vibrating equipment or piping can experience repeated mechanical stress over time.

    Even moderate vibration levels can create problems such as:

    • Signal instability
    • Measurement drift
    • Fatigue cracking
    • Sensor damage
    • Electronics failure
    • Loose wiring or fittings
    • Calibration issues

    The severity of damage often depends on:

    • Vibration frequency
    • Amplitude
    • Exposure duration
    • Mounting method
    • Transmitter design
    • Process conditions

    Common Symptoms of Vibration-Induced Damage

    Recognizing the warning signs early can help prevent unexpected failures.

    Common symptoms include:

    Unstable Pressure Readings

    One of the earliest indicators is fluctuating or noisy pressure signals. Vibration can interfere with sensing elements and electrical components, causing unstable outputs.

    Frequent Calibration Drift

    Transmitters exposed to prolonged vibration may require more frequent recalibration due to internal mechanical stress.

    Electrical Connection Problems

    Repeated vibration can loosen terminal screws, connectors, or wiring, leading to intermittent communication issues or signal loss.

    Mechanical Fatigue Cracks

    Over time, vibration may cause fatigue damage to:

    • Mounting brackets
    • Process connections
    • Welds
    • Internal components

    Premature Device Failure

    Severe vibration can shorten the operational lifespan of both the sensing element and transmitter electronics.

    Applications Most Susceptible to Vibration Issues

    Certain applications naturally expose instrumentation to higher vibration levels.

    These include:

    • Pump skid systems
    • Compressor stations
    • Hydraulic systems
    • Power generation equipment
    • Industrial refrigeration systems
    • Oil and gas processing
    • Chemical plants
    • Rotating machinery systems

    Transmitters installed directly on process piping near rotating equipment are particularly vulnerable.

    Understanding the Source of Vibration

    Effective mitigation begins with identifying the root cause of vibration.

    Mechanical Equipment Vibration

    Rotating machinery often creates continuous vibration caused by:

    • Imbalance
    • Misalignment
    • Bearing wear
    • Mechanical looseness

    Pipe Resonance

    Long piping systems may amplify vibration through resonance effects, especially near pumps and compressors.

    Fluid Pulsation

    Positive displacement pumps and reciprocating compressors can create pressure pulsations that mechanically stress transmitters.

    Structural Vibration

    Building structures, skid assemblies, and support frames may transfer vibration into instrumentation systems.

    Identifying the primary vibration source helps determine the best mitigation strategy.

    Best Practices for Mitigating Vibration-Induced Damage

    Several proven techniques can significantly reduce the impact of vibration on pressure transmitters.

    Relocate the Transmitter Away from the Vibration Source

    One of the most effective solutions is relocating the transmitter away from the most severe vibration zone.

    Instead of mounting directly on vibrating equipment or piping, use:

    • Remote mounting brackets
    • Capillary systems
    • Impulse lines
    • Flexible tubing connections

    Increasing physical separation often reduces transmitted vibration significantly.

    Use Remote Seals or Capillary Systems

    Remote seal systems allow the sensing element to be isolated from harsh mechanical conditions while maintaining accurate pressure measurement.

    Benefits include:

    • Reduced vibration exposure
    • Improved thermal isolation
    • Better protection from pulsation
    • Extended transmitter life

    These systems are especially valuable in demanding industrial environments.

    Install Flexible Impulse Lines

    Rigid piping transfers vibration directly into the transmitter body.

    Flexible impulse tubing can help absorb mechanical movement and reduce stress on the instrument.

    Properly installed flexible tubing:

    • Dampens vibration transmission
    • Reduces fatigue stress
    • Helps stabilize measurements

    Care should be taken to avoid unsupported tubing lengths that may introduce additional resonance.

    Add Vibration Dampening Mounts

    Specialized mounting hardware can isolate transmitters from mechanical vibration.

    Common solutions include:

    • Rubber isolation mounts
    • Spring dampeners
    • Shock absorbers
    • Anti-vibration brackets

    These components reduce the amount of vibration transferred into the transmitter housing.

    Use Snubbers or Pulsation Dampeners

    In systems with pressure pulsation, mechanical snubbers or pulsation dampeners can help stabilize both pressure and vibration effects.

    These devices:

    • Reduce pressure spikes
    • Smooth pulsating flow
    • Minimize sensor stress
    • Improve signal stability

    This is especially important in reciprocating pump applications.

    Properly Support Process Piping

    Poorly supported piping can amplify vibration and resonance.

    Proper pipe support design helps reduce:

    • Pipe movement
    • Mechanical stress
    • Resonance frequencies
    • Instrument loading

    Good piping practices improve both instrumentation reliability and overall system stability.

    Select Transmitters Designed for Industrial Environments

    Not all pressure transmitters offer the same vibration resistance.

    Industrial-grade transmitters often feature:

    • Reinforced internal construction
    • Rugged housings
    • Shock-resistant electronics
    • Advanced sensor designs
    • Improved vibration immunity

    Selecting a transmitter specifically designed for harsh industrial applications can significantly improve long-term reliability.

    Avoid Resonance Conditions

    Every mechanical system has natural resonant frequencies.

    If operating vibration matches the natural frequency of the transmitter assembly or mounting structure, vibration amplitude can increase dramatically.

    Mitigation strategies include:

    • Changing mounting configurations
    • Increasing structural rigidity
    • Adjusting support spacing
    • Using damping materials

    Avoiding resonance is critical for long-term equipment durability.

    Verify Electrical Connections

    Vibration can gradually loosen electrical terminations.

    Regular inspection and maintenance should include:

    • Checking terminal tightness
    • Inspecting connectors
    • Verifying grounding integrity
    • Looking for cable wear

    Secure wiring practices help maintain signal reliability.

    Implement Preventive Maintenance

    Routine inspection programs help detect vibration-related issues before failures occur.

    Preventive maintenance may include:

    • Visual inspections
    • Calibration verification
    • Signal trend analysis
    • Mounting inspections
    • Vibration monitoring

    Monitoring equipment condition over time helps identify developing problems early.

    The Role of Digital Signal Filtering

    Some modern pressure transmitters include digital filtering features that help stabilize readings in vibrating environments.

    Digital filtering can:

    • Reduce signal noise
    • Smooth output fluctuations
    • Improve process control stability

    However, filtering addresses signal instability ,  not the root mechanical cause of vibration damage. Mechanical mitigation strategies are still necessary.

    Environmental Considerations

    Industrial vibration issues are often compounded by other environmental factors such as:

    • Temperature cycling
    • Moisture
    • Corrosive chemicals
    • Electrical noise

    A comprehensive instrumentation strategy should evaluate all environmental conditions together when selecting and installing transmitters.

    Benefits of Proper Vibration Mitigation

    Reducing vibration-induced stress can deliver several operational benefits:

    Improved Measurement Accuracy

    Stable sensors provide more consistent and reliable process data.

    Longer Equipment Life

    Reducing mechanical fatigue extends transmitter lifespan.

    Reduced Maintenance Costs

    Fewer failures and recalibrations reduce maintenance requirements.

    Improved Process Reliability

    Reliable instrumentation improves process control and operational stability.

    Reduced Downtime

    Preventing premature failures helps minimize unplanned outages.

    Fuji Electric Pressure Measurement Solutions

    Fuji Electric offers industrial pressure measurement solutions engineered for demanding applications and harsh operating environments.

    Our pressure transmitters are designed to support:

    • Stable process measurement
    • Industrial durability
    • Long-term reliability
    • Harsh environmental operation
    • High-performance automation systems

    Fuji Electric instrumentation solutions help facilities improve process visibility, maintain measurement accuracy, and support reliable industrial operations even in challenging conditions.

    Vibration is one of the most common causes of premature pressure transmitter failure in industrial environments. Left unaddressed, vibration can reduce measurement accuracy, damage instrumentation, and increase maintenance costs.

    Fortunately, many vibration-related problems can be mitigated through proper installation practices, transmitter selection, mechanical isolation, and preventive maintenance strategies.

    By understanding the sources of vibration and implementing effective mitigation techniques, facilities can improve instrumentation reliability, extend equipment life, and maintain more stable and efficient industrial processes.

  • Noise Reduction Strategies for Regenerative Blower Installations

    Noise Reduction Strategies for Regenerative Blower Installations

    Regenerative blowers are widely used across industrial and commercial applications because of their compact design, oil-free operation, reliability, and ability to provide consistent airflow and vacuum performance. From pneumatic conveying and wastewater aeration to packaging equipment and medical systems, regenerative blowers play an essential role in many processes.

    However, like all high-speed air-moving equipment, regenerative blowers can generate noise during operation. If not properly managed, excessive noise can create challenges related to worker comfort, regulatory compliance, equipment perception, and overall facility environment.

    Understanding the causes of blower noise and implementing effective noise reduction strategies can significantly improve installation performance while maintaining airflow efficiency and system reliability.

    Why Regenerative Blowers Generate Noise

    Regenerative blowers operate by accelerating air through an impeller with multiple blades rotating at high speeds inside a specially designed housing. As air circulates through the blower stages, pressure and vacuum are generated through regenerative airflow principles.

    Several factors contribute to operational noise, including:

    • High-speed impeller rotation
    • Air turbulence
    • Motor noise
    • Mechanical vibration
    • Resonance within piping systems
    • Intake and discharge airflow noise

    The sound generated may vary depending on:

    • Blower size
    • Operating speed
    • System pressure
    • Installation environment
    • Mounting method
    • Piping design

    Understanding the primary noise source is the first step toward effective mitigation.

    Common Sources of Noise in Regenerative Blower Systems

    Noise does not always originate from the blower itself. In many installations, surrounding components and system design contribute significantly to overall sound levels.

    Airflow Noise

    Air movement through the intake and discharge ports is one of the most common noise sources.

    High-velocity airflow can create:

    • Turbulence
    • Whistling
    • Pulsation noise
    • Broadband airflow sound

    Restrictions or poorly designed piping may increase airflow turbulence and amplify noise levels.

    Mechanical Vibration

    Mechanical vibration from the blower and motor can transfer into:

    • Equipment frames
    • Floors
    • Pipe supports
    • Building structures

    This structure-borne vibration can create additional noise through resonance and amplification.

    Motor Noise

    The electric motor itself contributes operational sound through:

    • Bearing movement
    • Cooling fans
    • Electromagnetic hum
    • Rotational dynamics

    Variable frequency drive (VFD) operation may also introduce tonal noise depending on switching frequencies and motor design.

    Piping Resonance

    Long piping runs or unsupported ducts can resonate at certain frequencies, increasing perceived noise throughout the system.

    In some cases, piping systems act like acoustic amplifiers.

    Installation Environment

    Hard surfaces such as concrete walls, metal panels, and enclosed rooms can reflect and amplify sound waves, increasing overall noise exposure.

    Why Noise Reduction Matters

    Reducing blower noise offers several important benefits.

    Improved Workplace Comfort

    Lower noise levels create a more comfortable environment for operators and maintenance personnel.

    Regulatory Compliance

    Facilities may need to comply with:

    • OSHA workplace noise regulations
    • Local noise ordinances
    • Environmental standards

    Reduced Operator Fatigue

    Continuous exposure to high noise levels can contribute to fatigue and communication difficulties.

    Improved Equipment Perception

    Quiet operation often creates the perception of higher equipment quality and improved system performance.

    Better Facility Integration

    Noise reduction is particularly important in:

    • Medical facilities
    • Laboratories
    • Commercial buildings
    • Food processing facilities
    • Indoor manufacturing environments

    Effective Noise Reduction Strategies

    Several proven strategies can help reduce noise in regenerative blower installations.

    Install Intake Silencers

    One of the most effective methods for reducing blower noise is using intake silencers.

    Intake silencers help:

    • Reduce airflow turbulence noise
    • Lower intake sound pressure levels
    • Minimize high-frequency noise

    Properly sized silencers can significantly reduce airborne sound without substantially restricting airflow.

    Use Discharge Silencers

    Discharge silencers reduce noise generated as pressurized air exits the blower system.

    These silencers are especially beneficial in:

    • High-pressure applications
    • Pneumatic conveying systems
    • Aeration systems
    • Vacuum transport applications

    Selecting the correct silencer design is important to avoid excessive pressure drop.

    Isolate Vibration

    Mechanical vibration often contributes heavily to perceived noise levels.

    Vibration isolation techniques include:

    • Rubber isolation mounts
    • Spring isolators
    • Flexible connectors
    • Anti-vibration pads

    Proper isolation prevents vibration transfer into building structures and connected piping.

    Use Flexible Piping Connections

    Rigid piping can transfer vibration directly through the system.

    Flexible connectors help:

    • Reduce vibration transmission
    • Minimize resonance
    • Lower structure-borne noise

    Flexible connections are particularly important near the blower inlet and discharge ports.

    Optimize Piping Design

    Poor piping layouts can increase turbulence and resonance.

    Best practices include:

    • Avoiding abrupt transitions
    • Minimizing sharp bends
    • Using properly sized piping
    • Reducing airflow restrictions
    • Supporting piping adequately

    Smooth airflow reduces turbulence-related sound generation.

    Install Acoustic Enclosures

    In applications requiring substantial noise reduction, acoustic enclosures can provide significant sound attenuation.

    Well-designed enclosures may include:

    • Sound-absorbing insulation
    • Ventilation systems
    • Service access panels
    • Cooling airflow management

    However, thermal management is critical because regenerative blowers generate heat during operation.

    Apply Sound-Absorbing Materials

    Acoustic treatments within the installation area can help reduce reflected noise.

    Examples include:

    • Acoustic wall panels
    • Sound-absorbing ceiling materials
    • Insulated equipment rooms
    • Acoustic curtains

    Reducing sound reflection improves the overall acoustic environment.

    Proper Equipment Placement

    Blower location can significantly affect perceived noise levels.

    Whenever possible:

    • Place blowers away from occupied areas
    • Avoid corner installations that amplify sound
    • Use isolated equipment rooms
    • Separate blowers from reflective surfaces

    Strategic placement can reduce operator exposure without modifying the equipment itself.

    Optimize Blower Sizing

    Oversized blowers may operate inefficiently and generate unnecessary noise.

    Proper sizing helps:

    • Improve efficiency
    • Reduce excessive airflow velocity
    • Lower operating speeds
    • Minimize turbulence

    Selecting the correct blower for the application improves both acoustic and energy performance.

    Use Variable Frequency Drives (VFDs)

    Variable frequency drives allow blower speed control based on system demand.

    Benefits may include:

    • Lower operating speeds during reduced demand
    • Reduced airflow noise
    • Improved energy efficiency
    • Smoother system operation

    Careful VFD parameter setup can also help minimize motor-related tonal noise.

    Maintain the Blower System Properly

    Worn or damaged components can increase operational noise.

    Preventive maintenance should include:

    • Bearing inspections
    • Impeller inspection
    • Filter cleaning
    • Fastener checks
    • Alignment verification
    • Vibration monitoring

    Maintained equipment generally operates more quietly and efficiently.

    Understanding Noise Frequency Characteristics

    Different noise reduction methods target different frequency ranges.

    For example:

    • Silencers primarily address airborne airflow noise
    • Isolation mounts reduce low-frequency vibration
    • Acoustic foam absorbs mid- and high-frequency reflections

    A comprehensive noise reduction strategy often combines multiple approaches for the best results.

    Measuring and Evaluating Noise Levels

    Noise assessments help determine:

    • Primary noise sources
    • Frequency characteristics
    • Operator exposure levels
    • Effectiveness of mitigation efforts

    Sound measurements are commonly expressed in decibels (dBA).

    Evaluating both overall sound level and frequency spectrum provides better insight into appropriate mitigation strategies.

    Balancing Noise Reduction and Performance

    Noise reduction efforts should not compromise blower performance.

    Improper modifications may cause:

    • Excessive pressure drop
    • Reduced airflow
    • Increased motor loading
    • Thermal issues

    The goal is to achieve quieter operation while maintaining reliable system performance and efficiency.

    Fuji Electric Regenerative Blower Solutions

    Fuji Electric regenerative blowers are engineered for high performance, reliability, and efficient operation across demanding industrial applications.

    Our blower solutions are designed to support:

    • Stable airflow performance
    • Compact installation
    • Reliable continuous-duty operation
    • Industrial durability
    • Reduced maintenance requirements

    Fuji Electric also supports system optimization strategies that help improve installation efficiency, operational reliability, and overall acoustic performance.

    Noise generation is a common consideration in regenerative blower installations, particularly in facilities where operator comfort, environmental conditions, and regulatory compliance are important.

    Fortunately, effective noise reduction can often be achieved through a combination of:

    • Intake and discharge silencers
    • Vibration isolation
    • Proper piping design
    • Acoustic treatment
    • Equipment placement
    • Preventive maintenance

    By understanding the sources of blower noise and implementing appropriate mitigation strategies, facilities can create quieter, more efficient, and more reliable blower systems while maintaining the performance benefits regenerative blowers are known for.

  • Thermal Runaway in Power Semiconductors: Causes, Risks, and Prevention

    Thermal Runaway in Power Semiconductors: Causes, Risks, and Prevention

    Power semiconductors are the foundation of modern power electronics systems, enabling efficient energy conversion and motor control across applications such as industrial automation, renewable energy, electric vehicles, UPS systems, robotics, HVAC equipment, and data centers.

    As power densities continue to increase and systems become more compact, thermal management has become one of the most critical aspects of semiconductor reliability. One of the most serious thermal-related failure mechanisms in power electronics is thermal runaway.

    Thermal runaway can rapidly escalate from a localized temperature increase into catastrophic semiconductor failure, potentially damaging surrounding components and causing system downtime. Understanding the causes, risks, and prevention methods associated with thermal runaway is essential for improving reliability and long-term system performance.

    What Is Thermal Runaway?

    Thermal runaway occurs when increasing device temperature causes higher power dissipation, which then creates even more heat. This self-reinforcing cycle can quickly drive the semiconductor beyond safe operating limits.

    In many semiconductor devices, electrical characteristics change as temperature rises. Under certain operating conditions, higher temperatures may increase current flow or conduction losses, producing additional heat faster than the system can dissipate it.

    If heat generation exceeds the cooling system’s ability to remove heat, junction temperatures continue rising until permanent damage occurs.

    Thermal runaway can affect various power semiconductor devices, including:

    • IGBTs
    • MOSFETs
    • Diodes
    • SiC devices
    • Power modules
    • Bipolar transistors

    Why Thermal Runaway Matters

    Power semiconductor failures can have major consequences in industrial and commercial systems.

    Thermal runaway may result in:

    • Catastrophic semiconductor failure
    • Equipment shutdowns
    • Damage to surrounding circuitry
    • Reduced system reliability
    • Safety hazards
    • Increased maintenance costs
    • Production downtime

    In high-power applications such as motor drives, renewable energy inverters, and EV charging systems, preventing thermal runaway is critical for maintaining operational stability and equipment longevity.

    How Thermal Runaway Develops

    Thermal runaway typically occurs through a repeating feedback loop:

    1. Device temperature increases.
    2. Electrical losses increase.
    3. Additional heat is generated.
    4. Junction temperature rises further.
    5. The cycle accelerates.

    Without intervention, device temperatures can exceed safe operating limits in a very short time.

    The risk is especially high in high-current and high-switching-frequency applications where semiconductors already operate near thermal limits.

    Common Causes of Thermal Runaway

    Several factors can contribute to thermal runaway in power semiconductor systems.

    Inadequate Heat Dissipation

    One of the most common causes is insufficient cooling capacity.

    Heat generated inside the semiconductor must be transferred efficiently through:

    • Device packaging
    • Thermal interface materials
    • Heat sinks
    • Cooling systems

    If thermal resistance is too high, heat accumulates inside the device.

    Common cooling-related issues include:

    • Undersized heat sinks
    • Poor airflow
    • Inadequate liquid cooling
    • Contaminated cooling surfaces
    • Improper thermal interface application

    Even minor cooling inefficiencies can significantly impact junction temperatures.

    Excessive Current

    Operating semiconductors beyond their rated current increases conduction losses and junction heating.

    Overcurrent conditions may result from:

    • Motor stalls
    • Short circuits
    • Overloads
    • Improper sizing
    • Fault conditions

    As current increases, power dissipation rises rapidly, increasing thermal stress.

    High Switching Frequencies

    Switching losses increase with frequency.

    Applications using high-frequency switching may generate significant heat due to:

    • Turn-on losses
    • Turn-off losses
    • Gate charging losses
    • Reverse recovery losses

    If switching losses exceed cooling capability, thermal runaway risk increases.

    Poor PCB or Busbar Design

    Thermal performance is heavily influenced by system layout.

    Poor designs may create:

    • Uneven current distribution
    • Hot spots
    • Increased parasitic inductance
    • Localized thermal stress

    Inadequate copper area or insufficient thermal pathways can worsen heat accumulation.

    Uneven Current Sharing

    In parallel semiconductor configurations, current imbalance can occur between devices.

    If one device carries more current than others, it heats more rapidly. Higher temperature may further alter electrical characteristics, causing even greater imbalance.

    This localized overheating can trigger thermal runaway in the overloaded device.

    Elevated Ambient Temperatures

    High surrounding temperatures reduce the cooling system’s ability to remove heat.

    Applications exposed to:

    • Outdoor environments
    • Enclosed cabinets
    • High-temperature industrial facilities
    • Poor ventilation

    may experience reduced thermal margins.

    Gate Drive Issues

    Improper gate drive design can increase semiconductor losses.

    Examples include:

    • Incorrect gate voltage
    • Slow switching transitions
    • Insufficient dead time
    • Excessive ringing
    • Gate instability

    Suboptimal switching behavior increases power dissipation and thermal stress.

    Degraded Thermal Interface Materials

    Thermal interface materials (TIMs) help transfer heat between the semiconductor and heat sink.

    Over time, TIM degradation may increase thermal resistance due to:

    • Drying
    • Pump-out effects
    • Mechanical fatigue
    • Improper mounting pressure

    Reduced thermal conductivity can significantly elevate junction temperatures.

    Semiconductor Characteristics and Thermal Behavior

    Different semiconductor technologies respond differently to temperature changes.

    Bipolar Devices

    Traditional bipolar transistors can exhibit negative temperature characteristics that increase thermal runaway susceptibility.

    MOSFETs

    MOSFETs generally have positive temperature coefficients at higher operating regions, which can help improve current sharing in parallel configurations.

    However, MOSFETs may still experience thermal runaway under certain conditions involving excessive switching losses or insufficient cooling.

    IGBTs

    IGBT thermal behavior depends on operating current and temperature range. Modern IGBT technologies are carefully engineered to improve thermal stability and reliability.

    SiC Devices

    Silicon carbide (SiC) semiconductors support higher temperature operation and improved efficiency, but thermal management remains essential due to extremely high power density.

    Risks Associated with Thermal Runaway

    Thermal runaway can produce severe consequences beyond simple device failure.

    Catastrophic Device Destruction

    Extreme temperatures may destroy:

    • Semiconductor junctions
    • Bond wires
    • Packaging materials
    • Solder connections

    Failure may occur explosively in severe cases.

    Secondary System Damage

    Failed semiconductors can damage:

    • Gate drivers
    • Bus capacitors
    • PCBs
    • Motors
    • Power supplies
    • Adjacent modules

    The resulting repair costs may be substantial.

    Reduced Reliability and Lifespan

    Even repeated near-runaway thermal cycling can accelerate:

    • Solder fatigue
    • Wire bond degradation
    • Material aging
    • Mechanical stress

    Over time, this reduces overall system reliability.

    Downtime and Operational Losses

    Unexpected semiconductor failures can create:

    • Production interruptions
    • Unplanned maintenance
    • Lost productivity
    • Service disruptions

    For mission-critical systems, downtime costs can be extremely high.

    Strategies for Preventing Thermal Runaway

    Preventing thermal runaway requires a comprehensive thermal management approach.

    Proper Thermal Design

    Effective cooling design is the first line of defense.

    Key considerations include:

    • Correct heat sink sizing
    • Adequate airflow
    • Liquid cooling when necessary
    • Low thermal resistance pathways
    • Proper enclosure ventilation

    Thermal simulations are often used during system design to verify cooling performance.

    Monitor Junction Temperatures

    Temperature monitoring helps detect abnormal operating conditions before failure occurs.

    Modern systems may use:

    • Embedded temperature sensors
    • Thermal shutdown protection
    • Real-time diagnostics
    • Predictive monitoring systems

    Active monitoring improves system protection and reliability.

    Use Appropriate Semiconductor Ratings

    Devices should be selected with adequate safety margins for:

    • Current
    • Voltage
    • Temperature
    • Switching frequency

    Operating continuously near maximum ratings reduces thermal margin and increases failure risk.

    Optimize Switching Performance

    Proper gate driver design minimizes switching losses.

    Optimization may include:

    • Gate resistor tuning
    • Controlled switching speeds
    • Dead-time optimization
    • Low-inductance layouts

    Efficient switching reduces overall heat generation.

    Improve Thermal Interface Quality

    Proper thermal interface application is critical.

    Best practices include:

    • Uniform mounting pressure
    • High-quality TIM materials
    • Clean mounting surfaces
    • Periodic inspection and replacement

    Reducing interface resistance improves heat transfer efficiency.

    Balance Parallel Devices Properly

    Parallel semiconductor designs should ensure balanced current sharing through:

    • Matched devices
    • Symmetrical layouts
    • Proper gate drive design
    • Current balancing techniques

    Uniform current distribution reduces localized overheating risk.

    Implement Protective Circuits

    Protective functions help prevent dangerous operating conditions.

    Common protections include:

    • Overcurrent protection
    • Thermal shutdown
    • Short-circuit protection
    • Desaturation detection
    • Soft shutdown circuits

    Fast fault response helps prevent thermal escalation.

    Maintain Cooling Systems

    Cooling system degradation can increase thermal resistance over time.

    Preventive maintenance should include:

    • Fan inspection
    • Filter cleaning
    • Coolant verification
    • Heat sink cleaning
    • Airflow monitoring

    Maintained cooling systems improve long-term reliability.

    The Importance of Thermal Simulation

    Thermal modeling and simulation are increasingly important in modern power electronics design.

    Simulation tools help engineers evaluate:

    • Junction temperatures
    • Airflow patterns
    • Heat distribution
    • Cooling effectiveness
    • Worst-case operating conditions

    Early thermal analysis helps identify risks before hardware deployment.

    Fuji Electric Semiconductor Solutions

    Fuji Electric develops advanced semiconductor technologies engineered for high efficiency, thermal performance, and long-term reliability across demanding industrial applications.

    Our semiconductor solutions support:

    • Industrial motor drives
    • Renewable energy systems
    • UPS platforms
    • HVAC systems
    • Electric mobility
    • Power conversion applications

    Fuji Electric technologies are designed to help improve thermal stability, reduce losses, and support reliable high-performance power electronics systems.

    Thermal runaway remains one of the most significant reliability risks in power semiconductor systems. As power densities increase and systems become more compact, effective thermal management becomes even more critical.

    Understanding the causes of thermal runaway ,  including inadequate cooling, excessive current, switching losses, and thermal imbalance ,  allows engineers to design safer and more reliable systems.

    Through proper thermal design, careful component selection, active monitoring, and preventive maintenance, facilities can significantly reduce the risk of thermal runaway while improving the performance and longevity of power electronic systems.

  • What Makes an HMI “Industrial Grade”? Key Specs to Look For

    What Makes an HMI “Industrial Grade”? Key Specs to Look For

    Human Machine Interfaces (HMIs) have become a critical part of modern industrial automation systems. From manufacturing plants and water treatment facilities to energy systems and packaging equipment, HMIs provide operators with real-time visibility and control over machines and processes.

    However, not all HMIs are designed for demanding industrial environments. While consumer-grade displays may function in controlled office settings, industrial applications require rugged, reliable, and purpose-built systems capable of withstanding harsh operating conditions.

    Understanding what makes an HMI truly “industrial grade” is essential when selecting the right solution for long-term reliability, safety, and performance.

    What Is an Industrial HMI?

    An industrial HMI is a specialized interface device that allows operators to monitor, control, and interact with industrial machinery and automation systems.

    Industrial HMIs typically provide:

    • Real-time process visualization
    • Alarm management
    • Equipment status monitoring
    • Data collection and trending
    • System diagnostics
    • Operator controls
    • Integration with PLCs, drives, and SCADA systems

    Unlike consumer electronics, industrial HMIs are engineered to operate continuously in environments exposed to:

    • Dust
    • Moisture
    • Vibration
    • Temperature extremes
    • Electrical noise
    • Chemicals
    • Washdown procedures

    The reliability requirements are significantly higher because downtime can directly impact production, safety, and profitability.

    Why “Industrial Grade” Matters

    In industrial environments, equipment failures can lead to:

    • Production interruptions
    • Lost revenue
    • Safety risks
    • Product quality issues
    • Increased maintenance costs

    A consumer-grade display or under-specified HMI may fail prematurely when exposed to harsh conditions. Industrial-grade HMIs are specifically designed to deliver stable operation under continuous industrial use.

    Choosing the right HMI can improve:

    • System uptime
    • Operator efficiency
    • Equipment longevity
    • Maintenance response times
    • Overall operational reliability

    Key Specifications That Define an Industrial-Grade HMI

    Several critical specifications separate industrial HMIs from standard commercial displays.

    Rugged Environmental Ratings

    One of the most important indicators of an industrial-grade HMI is its environmental protection rating.

    IP Ratings

    Ingress Protection (IP) ratings define resistance to dust and moisture.

    Common industrial ratings include:

    • IP65 ,  Dust-tight and protected against water jets
    • IP66 ,  Higher protection against powerful water jets
    • IP67 ,  Temporary immersion protection

    For washdown environments such as food processing or pharmaceuticals, higher protection ratings are often required.

    NEMA Ratings

    In North America, NEMA enclosure ratings are also commonly used.

    Examples include:

    • NEMA 4 ,  Indoor/outdoor protection against dust and water
    • NEMA 4X ,  Additional corrosion resistance
    • NEMA 12 ,  Protection against dust, dirt, and oil

    Proper environmental protection is essential for preventing contamination and premature equipment failure.

    Wide Operating Temperature Range

    Industrial facilities may experience:

    • High ambient temperatures
    • Cold outdoor installations
    • Heat generated by surrounding equipment

    Industrial HMIs are designed to operate reliably across wider temperature ranges than commercial displays.

    Typical industrial operating ranges may include:

    • 0°C to 50°C
    • -20°C to 60°C
    • Wider ranges for extreme environments

    Temperature tolerance is particularly important in:

    • Steel mills
    • Outdoor pumping stations
    • HVAC systems
    • Refrigeration facilities
    • Energy infrastructure

    Vibration and Shock Resistance

    Industrial machinery often generates continuous vibration and mechanical shock.

    Industrial-grade HMIs are designed with:

    • Reinforced internal components
    • Solid-state storage
    • Rugged mounting systems
    • Shock-resistant construction

    This helps maintain reliable operation in environments such as:

    • Manufacturing plants
    • Heavy equipment
    • Transportation systems
    • Material handling systems

    Without adequate vibration resistance, connectors, displays, and circuit boards may fail over time.

    High Display Brightness and Visibility

    Operators must be able to clearly view the HMI under varying lighting conditions.

    Industrial HMIs often feature:

    • High-brightness displays
    • Anti-glare coatings
    • Wide viewing angles
    • Enhanced contrast ratios

    Outdoor or brightly lit facilities may require sunlight-readable displays with brightness levels exceeding 1,000 nits.

    Good visibility improves:

    • Operator response time
    • Safety
    • Process monitoring accuracy
    • Overall usability

    Long Product Lifecycle Support

    Consumer electronics change rapidly, but industrial systems often remain in operation for 10 to 20 years or more.

    Industrial-grade HMIs typically offer:

    • Longer product availability
    • Stable hardware platforms
    • Long-term replacement support
    • Backward compatibility
    • Extended firmware support

    This is critical for minimizing redesign costs and maintaining system consistency over the life of the equipment.

    Industrial Communication Protocol Support

    Industrial automation systems rely on communication between devices.

    Industrial HMIs commonly support protocols such as:

    • Modbus TCP/IP
    • EtherNet/IP
    • PROFINET
    • EtherCAT
    • BACnet
    • CANopen
    • PROFIBUS

    Seamless communication with PLCs, AC drives, sensors, and SCADA systems is essential for reliable automation performance.

    Compatibility with multiple protocols increases system flexibility and simplifies integration.

    Continuous Duty Reliability

    Unlike office displays that may operate intermittently, industrial HMIs are often required to run continuously 24/7.

    Industrial-grade designs prioritize:

    • Long-life components
    • Thermal management
    • Fanless cooling designs
    • High MTBF (Mean Time Between Failures)

    Fanless systems are particularly valuable because they reduce:

    • Dust intake
    • Mechanical failure points
    • Maintenance requirements

    Continuous-duty reliability is essential in critical operations where downtime is costly.

    Touchscreen Durability

    Industrial touchscreens must withstand:

    • Frequent operator use
    • Gloves
    • Chemicals
    • Cleaning agents
    • Abrasion

    Industrial HMIs may use:

    • Resistive touchscreens
    • Capacitive touchscreens
    • Chemically strengthened glass
    • Multi-touch functionality

    Application requirements determine which touchscreen technology is best.

    For example:

    • Resistive screens work well with gloves and harsh conditions
    • Capacitive screens offer improved responsiveness and modern usability

    Electrical Noise Immunity

    Industrial facilities often contain:

    • Large motors
    • AC drives
    • Welding equipment
    • Switching power systems

    These environments generate significant electromagnetic interference (EMI).

    Industrial-grade HMIs are designed with shielding and filtering to maintain stable operation despite electrical noise.

    Proper EMI immunity helps prevent:

    • Communication errors
    • Screen freezes
    • Unexpected resets
    • Data corruption

    Data Logging and Edge Processing Capabilities

    Modern industrial HMIs increasingly support:

    • Data logging
    • Historical trending
    • Edge computing
    • Local analytics
    • Alarm history storage

    These capabilities help improve:

    • Troubleshooting
    • Process optimization
    • Predictive maintenance
    • Operational visibility

    Advanced HMIs may even support embedded scripting and lightweight industrial applications.

    Security Features

    As industrial systems become more connected, cybersecurity becomes increasingly important.

    Industrial HMIs may include:

    • User authentication
    • Role-based access
    • Encrypted communications
    • Secure remote access
    • Firmware integrity protection

    Security features help protect critical infrastructure and industrial operations from unauthorized access.

    Scalability and Expandability

    Industrial facilities evolve over time, so HMIs should support future expansion.

    Scalable HMIs may offer:

    • Multiple screen sizes
    • Expansion ports
    • Remote monitoring support
    • Web-based visualization
    • Cloud connectivity

    Flexible platforms help reduce future upgrade costs and simplify system growth.

    Software Stability and Ease of Integration

    Reliable hardware is only part of the equation. Industrial-grade HMIs also require stable software platforms.

    Important software considerations include:

    • Intuitive development tools
    • Reliable runtime performance
    • Easy PLC integration
    • Alarm management tools
    • Data visualization capabilities
    • Remote maintenance support

    Ease of configuration can significantly reduce engineering and commissioning time.

    Selecting the Right Industrial HMI

    Choosing the best HMI depends on:

    • Environmental conditions
    • Application complexity
    • Operator requirements
    • Communication needs
    • Regulatory requirements
    • Long-term support expectations

    Facilities should carefully evaluate:

    • Environmental ratings
    • Display performance
    • Connectivity
    • Lifecycle support
    • Reliability history
    • Vendor support capabilities

    The lowest upfront cost may not provide the best long-term value in demanding industrial environments.

    Fuji Electric Industrial HMI Solutions

    Fuji Electric offers industrial HMI solutions designed for reliability, usability, and performance in demanding automation environments.

    Our HMI technologies support:

    • Industrial communication integration
    • Rugged operating environments
    • High-performance visualization
    • Automation system connectivity
    • Long-term operational reliability

    Fuji Electric solutions are engineered to help manufacturers improve operator visibility, streamline control systems, and support efficient industrial operations.

    Industrial HMIs play a vital role in modern automation systems, serving as the connection point between operators and industrial equipment. However, not all HMIs are built to withstand the demands of industrial environments.

    True industrial-grade HMIs are designed with rugged construction, environmental protection, long-term reliability, communication flexibility, and continuous-duty performance in mind.

    By understanding the key specifications that define industrial-grade performance, facilities can make more informed HMI selection decisions that improve uptime, simplify maintenance, and support long-term operational success.

  • Regenerative Loads: When Do You Need a Dynamic Braking Resistor?

    Regenerative Loads: When Do You Need a Dynamic Braking Resistor?

    Modern AC drive systems are designed to deliver precise motor control, energy efficiency, and reliable operation across a wide range of industrial applications. However, some applications create a unique challenge for variable frequency drives (VFDs): regenerative energy.

    When a motor slows down or is driven by the load itself, it can act like a generator and send energy back into the drive. If that energy is not properly managed, it can cause nuisance trips, overvoltage faults, or even equipment damage. One of the most common solutions is a dynamic braking resistor.

    Understanding when regenerative energy occurs ,  and when a braking resistor is required ,  is essential for designing reliable motion control systems.

    What Is a Regenerative Load?

    A regenerative load occurs when the mechanical system drives the motor faster than the commanded speed or when the motor rapidly decelerates. Instead of consuming power, the motor generates power and sends it back into the DC bus of the AC drive.

    As regenerative energy builds inside the drive, the DC bus voltage rises. If the voltage exceeds safe operating limits, the drive will typically trip on a DC bus overvoltage fault.

    Regenerative conditions commonly occur in applications with:

    • Rapid deceleration
    • High inertia loads
    • Overhauling loads
    • Vertical motion systems
    • Frequent stopping and starting
    • Continuous energy feedback from the process

    Common Applications That Create Regenerative Energy

    Several industrial applications are naturally regenerative due to the physics of the load.

    Conveyors with High Inertia

    Long conveyors transporting heavy products often store large amounts of kinetic energy. During deceleration, that energy must go somewhere. Without a braking method, the drive may experience overvoltage conditions.

    Centrifuges and Flywheel Loads

    High-speed rotating equipment stores significant rotational energy. Fast stopping times can generate large regenerative currents as the motor attempts to slow the system.

    Cranes, Hoists, and Elevators

    Vertical loads are among the most common regenerative applications. Gravity can drive the motor during lowering operations, continuously feeding energy back into the drive.

    Fans and Blowers

    Large fans may continue spinning due to airflow or momentum after a stop command. Applications with aggressive deceleration ramps can become regenerative.

    Unwind Systems

    In web handling and converting operations, tension-controlled unwind systems often operate in regenerative mode because the material roll drives the motor.

    What Happens Without Proper Braking?

    When regenerative energy cannot be dissipated or redirected, several issues may occur:

    • DC bus overvoltage trips
    • Unexpected downtime
    • Loss of process control
    • Excessive stopping times
    • Reduced system reliability
    • Potential stress on drive components

    In some cases, operators attempt to solve the issue by increasing deceleration times. While this can reduce regenerative energy, it may not meet process requirements where rapid stopping is necessary.

    What Is a Dynamic Braking Resistor?

    A dynamic braking resistor dissipates excess regenerative energy as heat.

    When the DC bus voltage rises above a predefined threshold, the drive activates a braking transistor (sometimes called a chopper transistor). The transistor directs excess energy into the resistor, where it is converted into thermal energy and safely dissipated.

    This allows the drive to:

    • Decelerate loads faster
    • Prevent overvoltage faults
    • Improve stopping performance
    • Maintain process control
    • Protect drive electronics

    Dynamic braking is one of the simplest and most cost-effective solutions for handling intermittent regenerative energy.

    How Dynamic Braking Works

    The process can be summarized in four basic steps:

    1. The motor begins decelerating.
    2. The motor generates regenerative energy.
    3. DC bus voltage inside the drive increases.
    4. The braking transistor switches energy into the resistor.

    The resistor absorbs and dissipates the energy as heat until the DC bus voltage returns to a safe range.

    Because the resistor converts energy into heat, proper sizing and ventilation are important considerations.

    When Do You Need a Dynamic Braking Resistor?

    Not every AC drive application requires a braking resistor. Several factors determine whether one is necessary.

    Fast Deceleration Requirements

    If the application requires rapid stopping times, regenerative energy increases significantly. The shorter the deceleration ramp, the greater the braking demand.

    Applications that need aggressive acceleration and deceleration cycles often benefit from braking resistors.

    High Inertia Loads

    Loads with large rotating masses store more kinetic energy. Even moderate deceleration rates can generate substantial regenerative power.

    Examples include:

    • Large fans
    • Crushers
    • Centrifuges
    • Heavy conveyors

    Vertical or Overhauling Loads

    Whenever gravity assists motion, the motor can easily become regenerative. Hoists, elevators, cranes, and winches frequently require braking solutions.

    Frequent Cycling

    Applications with constant start-stop operation can repeatedly generate regenerative energy. Over time, this can create recurring overvoltage faults without proper braking.

    Overvoltage Faults During Deceleration

    One of the clearest signs that braking may be required is repeated DC bus overvoltage trips during stopping.

    If extending deceleration time is not practical, a braking resistor may be the best solution.

    When a Braking Resistor May Not Be Necessary

    Some applications naturally dissipate energy through system losses and may not require external braking.

    Examples include:

    • Low inertia loads
    • Long deceleration times
    • Constant-speed applications
    • Systems with infrequent stopping

    Many modern AC drives can also use techniques such as flux braking or controlled deceleration to help manage smaller regenerative conditions.

    Dynamic Braking vs. Regenerative Drives

    While braking resistors dissipate energy as heat, regenerative drive systems return excess energy back to the power grid.

    Each approach has advantages depending on the application.

    Dynamic Braking Resistors

    Advantages:

    • Lower initial cost
    • Simpler installation
    • Effective for intermittent braking
    • Compact solution

    Considerations:

    • Energy is wasted as heat
    • Additional heat management may be required
    • Limited continuous braking capability

    Regenerative Drives

    Advantages:

    • Returns energy to the electrical system
    • Improved overall efficiency
    • Better for continuous regeneration
    • Reduced heat generation

    Considerations:

    • Higher initial cost
    • More complex system integration
    • May require harmonic mitigation considerations

    For many industrial applications with occasional deceleration events, dynamic braking remains the preferred solution due to its simplicity and cost effectiveness.

    Proper Braking Resistor Sizing Matters

    Selecting the correct resistor is critical for reliable operation.

    Important sizing factors include:

    • Motor horsepower
    • DC bus voltage
    • Braking torque requirements
    • Duty cycle
    • Deceleration time
    • Load inertia
    • Ambient temperature

    Undersized resistors can overheat or fail prematurely, while oversized systems may increase unnecessary cost.

    Thermal management is also important because braking resistors can generate substantial heat during operation.

    Improving Reliability in Regenerative Applications

    Proper system design can help minimize braking-related issues and improve long-term reliability.

    Best practices include:

    • Verify load inertia during system design
    • Avoid unnecessarily aggressive deceleration ramps
    • Ensure proper resistor ventilation
    • Follow manufacturer sizing guidelines
    • Monitor braking duty cycle
    • Consider regenerative drives for continuous energy feedback applications

    Understanding the behavior of regenerative loads early in the design process helps prevent nuisance trips and improves overall system performance.

    Fuji Electric AC Drive Solutions

    Fuji Electric offers advanced AC drive solutions designed to handle demanding industrial applications, including regenerative load conditions. Our drive technologies provide reliable motor control, flexible braking integration, and high-performance operation across a wide range of industries.

    Fuji Electric drives support:

    • Dynamic braking configurations
    • High-performance motor control
    • Fast response applications
    • High-inertia load management
    • Industrial automation systems
    • Energy-efficient operation

    Whether your application involves conveyors, cranes, fans, hoists, or heavy industrial machinery, Fuji Electric can help identify the right drive and braking solution to improve performance and reliability.

    Regenerative energy is a common challenge in many AC drive applications, particularly those involving rapid deceleration, high inertia, or overhauling loads. Without proper energy management, regenerative conditions can lead to overvoltage faults, downtime, and reduced system reliability.

    Dynamic braking resistors provide a practical and effective method for dissipating excess energy and maintaining stable drive operation. By understanding when regenerative braking occurs and selecting the appropriate braking solution, facilities can improve uptime, protect equipment, and optimize motion control performance.

    As industrial systems continue demanding faster speeds, greater precision, and higher efficiency, effective regenerative energy management will remain an essential part of modern AC drive system design.

  • Understanding Short-Circuit Ratings (SCCR) for Control Panels

    Understanding Short-Circuit Ratings (SCCR) for Control Panels

    Protect your equipment. Ensure compliance. Prevent catastrophic failure.

    What is SCCR?

    Short-Circuit Current Rating (SCCR) defines the maximum fault current a control panel can safely withstand without causing fire, explosion, or extensive damage. It’s expressed in kiloamperes (kA) and must meet or exceed the available fault current at the installation point.


    Why SCCR Matters

    Safety First
    An underrated panel exposed to high fault current can fail violently—putting personnel and equipment at serious risk.

    Code Compliance
    Standards like NFPA 70 (National Electrical Code) and UL 508A require proper SCCR marking and verification for industrial control panels.

    Avoid Costly Rework
    If a panel’s SCCR is lower than the available fault current, it may fail inspection—leading to redesigns, delays, and added cost.


    How SCCR is Determined

    SCCR is based on the lowest-rated component within the power circuit—unless specific tested combinations allow for higher ratings.

    Key factors include:

    • Overcurrent Protection Devices (OCPDs)
      Fuses and circuit breakers can significantly influence overall SCCR when properly selected.
    • Component Ratings
      Contactors, motor starters, terminal blocks, and drives all have individual SCCRs.
    • Tested Combinations
      Using manufacturer-tested combinations (per UL 508A Supplement SB) can increase the panel’s overall SCCR.


    Common Pitfalls

    Weakest-Link Limitation
    A single low-rated component can reduce the entire panel’s SCCR.

    Ignoring Available Fault Current
    Failing to calculate or verify available fault current at the installation site leads to mismatches.

    Improper Component Pairing
    Not all combinations of breakers, fuses, and components are rated to work together at higher fault levels.


    Using current-limiting devices or UL-tested component combinations can allow a control panel’s SCCR to exceed the rating of its lowest-rated individual component. A component SCCR applies only to an individual device, while a panel SCCR represents the overall short-circuit withstand rating of the entire assembled control panel under specified conditions.


    How to Increase SCCR

    Use Current-Limiting Fuses
    These can dramatically raise the effective SCCR by reducing let-through energy during a fault.

    Select High-SCCR Components
    Choose contactors, drives, and terminals with higher withstand ratings.

    Leverage Tested Assemblies
    Follow UL 508A Supplement SB guidelines for approved component combinations.

    Optimize Circuit Design
    Segment circuits or add protective devices to isolate and limit fault exposure.


    Best Practices

    • Verify available fault current early in the design phase
    • Match or exceed SCCR across all components
    • Clearly label panel SCCR per code requirements
    • Document calculations and component ratings for inspection


    SCCR isn’t just a specification—it’s a critical safeguard. Properly rated control panels protect people, ensure compliance, and prevent costly failures.

  • How UPS Scalability Impacts Total Cost of Ownership in AI Data Centers

    How UPS Scalability Impacts Total Cost of Ownership in AI Data Centers

    Scale intelligently. Control costs. Keep compute online.


    Why Scalability Matters in AI Environments

    AI data centers don’t grow linearly—they scale in bursts as new GPU clusters come online. A UPS that can expand in step with demand avoids overbuilding, reduces stranded capacity, and keeps capital aligned with actual load.


    Where Scalability Impacts TCO

    1) CapEx Efficiency (Pay-as-You-Grow)

    • Start with a right-sized frame; add power modules as racks come online
    • Defer capital until it’s needed; avoid idle kW
    • Simplify budgeting for phased AI deployments

    Result: Lower upfront spend and better capital utilization.


    2) Energy Efficiency Across Load Ranges

    • Modular systems keep each module near optimal load
    • Higher efficiency at partial load vs oversized monolithic units
    • Reduced losses lower cooling demand

    Result: Lower OpEx and improved PUE.


    3) Availability & Redundancy (N+1 at Every Stage)

    • Add redundancy per phase (e.g., N+1 per frame)
    • Hot-swappable modules enable maintenance without downtime
    • Isolate failures to a single module

    Result: Higher uptime and reduced risk of revenue-impacting outages.


    4) Footprint & Power Density

    • Consolidate capacity into compact frames
    • Free up white space for revenue-generating compute
    • Align with high-density AI rack designs

    Result: Better $/sq ft and higher compute density.


    5) Maintenance & Lifecycle Costs

    • Swap modules instead of full-system overhauls
    • Standardized spares reduce inventory complexity
    • Enable predictive maintenance via granular monitoring

    Result: Lower service costs and less downtime.


    6) Future-Proofing for AI Workloads

    • Rapid onboarding of new GPU clusters without re-architecting power
    • Support for higher rack densities (e.g., 30–100+ kW/rack)
    • Easier integration of new battery chemistries and firmware upgrades

    Result: Avoid costly retrofits as AI demand accelerates.


    Modular vs. Monolithic UPS (TCO Snapshot)

    Factor

    Modular UPS

    Monolithic UPS

    Upfront Cost

    Lower (phased)

    Higher (overprovisioned)

    Efficiency at Partial Load

    High

    Lower

    Scalability

    Incremental

    Limited/step changes

    Redundancy

    Flexible (N+1 per stage)

    Fixed

    Maintenance

    Module-level

    System-level

    Risk of Stranded Capacity

    Low

    High


    Best Practices for AI Data Centers

    • Design for growth blocks: Size frames for near-term expansion, not peak end-state
    • Standardize modules: Simplify spares and maintenance across sites
    • Target optimal loading (40–80%): Maximize efficiency and longevity
    • Plan redundancy early: Build N+1 (or 2N) into each expansion phase
    • Integrate monitoring: Tie UPS telemetry into DCIM for capacity and health insights


    UPS scalability directly shapes both CapEx and OpEx in AI data centers. Modular, pay-as-you-grow architectures reduce wasted capacity, maintain high efficiency, and deliver resilient uptime—lowering total cost of ownership while enabling rapid expansion.